How do Surface Area Analyzers work?
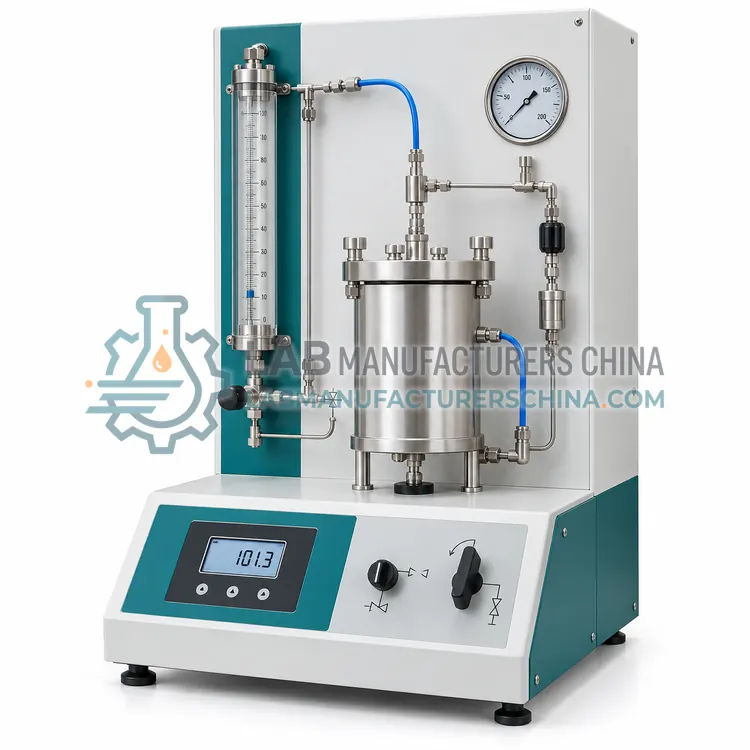
Gas adsorption methods expose a degassed powder to nitrogen at 77 K. Adsorbed gas quantity is measured at several relative pressures, and the Brunauer–Emmett–Teller (BET) equation converts the monolayer capacity into surface area using the molecular cross-sectional area of nitrogen, 0.162 nm². Static volumetric systems dose known gas volumes and calculate uptake from pressure changes. Dynamic flow systems pass a nitrogen–helium mixture over the sample and detect adsorption and desorption by a thermal conductivity detector. Air permeability methods, such as Blaine or Fisher-type apparatus, measure the resistance to airflow through a packed powder bed of defined porosity, and the Kozeny–Carman relation gives specific surface area. Key components include sample tubes, degassing stations, pressure transducers, Dewar flask or cryogenic bath, and calibrated volumes.
Which Surface Area Analyzers variants are available?
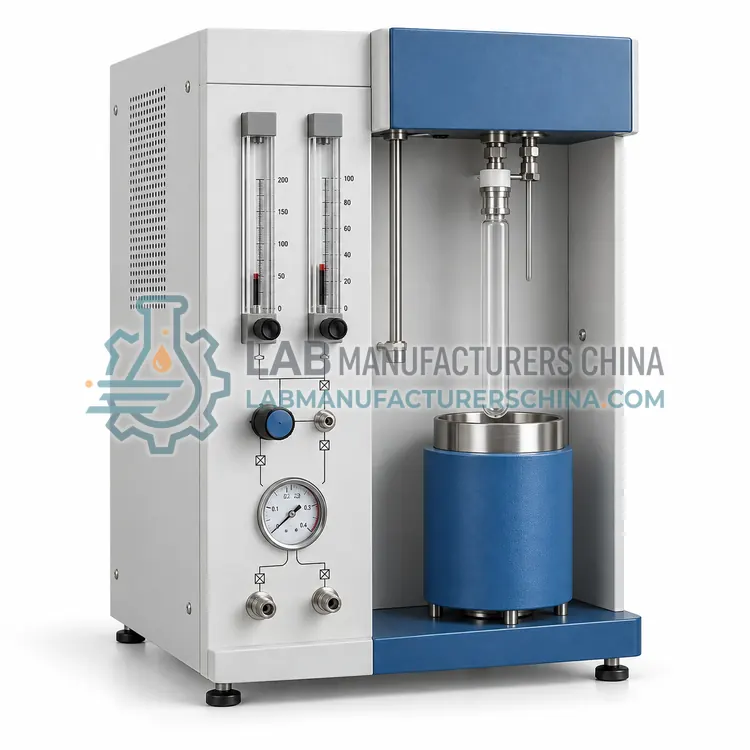
- Single-Point Flow BET Surface Area Analyzer for Powder QC — A dynamic flow analyzer that measures nitrogen adsorption from a helium mixture with a thermal conductivity detector, producing single-point or few-point BET values in minutes.
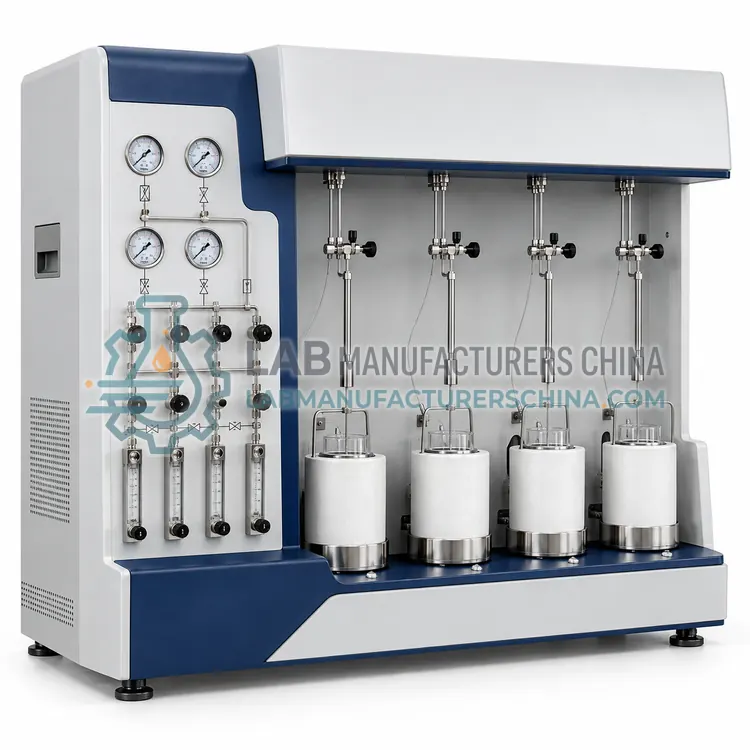
- Multi-Station Static Volumetric BET Surface Area Analyzer for Powders — A static volumetric analyzer that dose nitrogen to a cooled sample and records the full adsorption isotherm at up to four stations simultaneously.
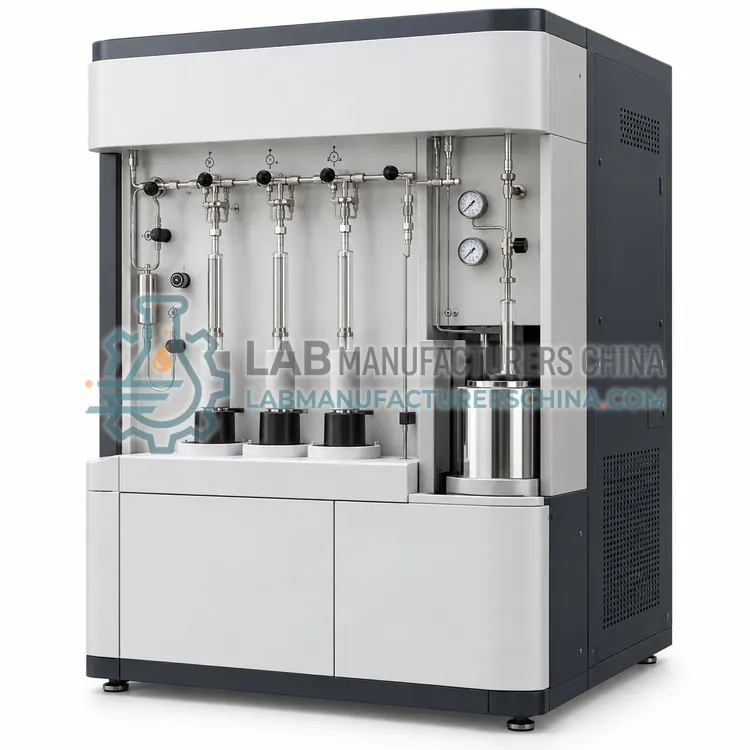
- Nanopowder and Fine Particle BET Surface Area Analyzer with Micropore Option — A static physisorption analyzer configured for high-surface-area nanopowders, with a fine pressure transducer range and turbomolecular pump for micropore analysis.
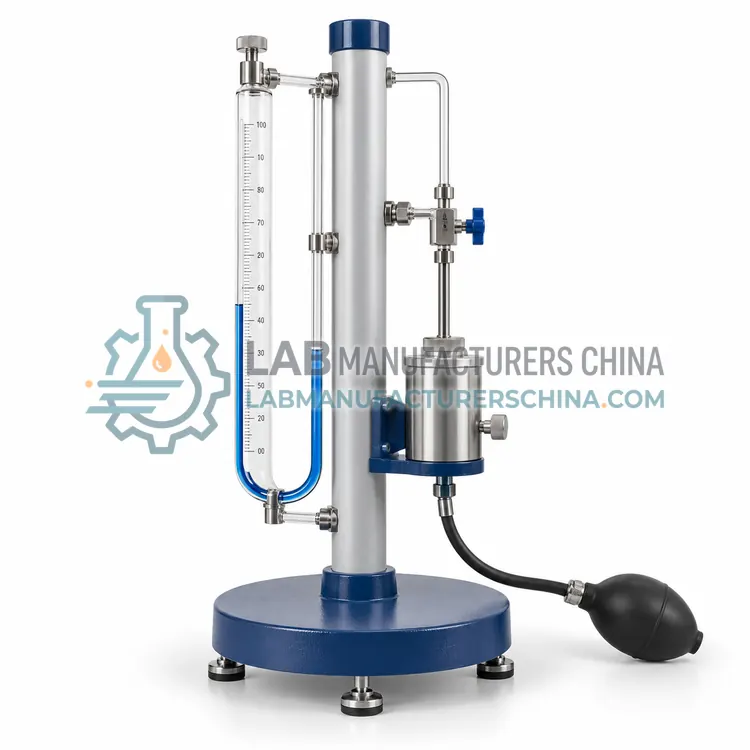
- Blaine Air Permeability Apparatus for Cement and Fine Powders — A manual or automatic air permeability apparatus that measures the specific surface of cement and similar fine powders by timing air flow through a compacted bed of defined porosity.
- Automatic Air Permeability Specific Surface Analyzer — An automated air permeability instrument that controls airflow, pressure drop and bed compaction electronically to give specific surface and average particle size of fine powders.
How do I choose the right variant?
Choose according to the material and the decision that depends on the result. Cement and fine powders in production control are commonly measured by air permeability because it is fast and standardised. Nanopowders, catalysts supports and battery materials need gas adsorption to capture surfaces that permeability cannot. Single-point flow instruments give quick QC numbers, while multipoint static systems provide a full BET isotherm and validate linearity and C constant. Consider the expected surface area range, because materials under 1 m²/g require krypton or larger sample masses. Check the number of stations, degassing capability, liquid nitrogen handling, and whether results must follow ISO 9277 or ASTM D3663. Software features for automatic BET range selection per ISO 9277 and Rouquerol criteria reduce operator bias.
Where are Surface Area Analyzers used?
Surface Area Analyzers are specified in cement fineness control, battery electrode and cathode powders, catalyst supports and activated carbon, pharmaceutical API and excipient characterisation, pigments, silica and carbon black and nanopowder development.
Which standards and certifications apply?
Work with Surface Area Analyzers is commonly governed by ISO 9277, ASTM D3663, ASTM C204, EN 196-6, ASTM D6556, ISO 15901-2 and GB/T 19587. Instrument certifications such as CE marking are confirmed per configuration and never assumed.
What are the key considerations before purchase?
Sample preparation strongly affects surface area. Degas powders at a temperature and time that remove moisture and volatiles without altering the structure, and use the same protocol for every batch. Weigh samples accurately after degassing, because mass error transfers directly to the result. Keep the cryogenic bath level and cold trap stable, use high-purity nitrogen and helium, and check for leaks. Verify calibration with certified reference materials of known surface area. For air permeability, control bed porosity, temperature and humidity, and calibrate with a reference powder. Record degassing conditions and the BET pressure range in reports, and follow IQ/OQ/PQ practice where regulated.