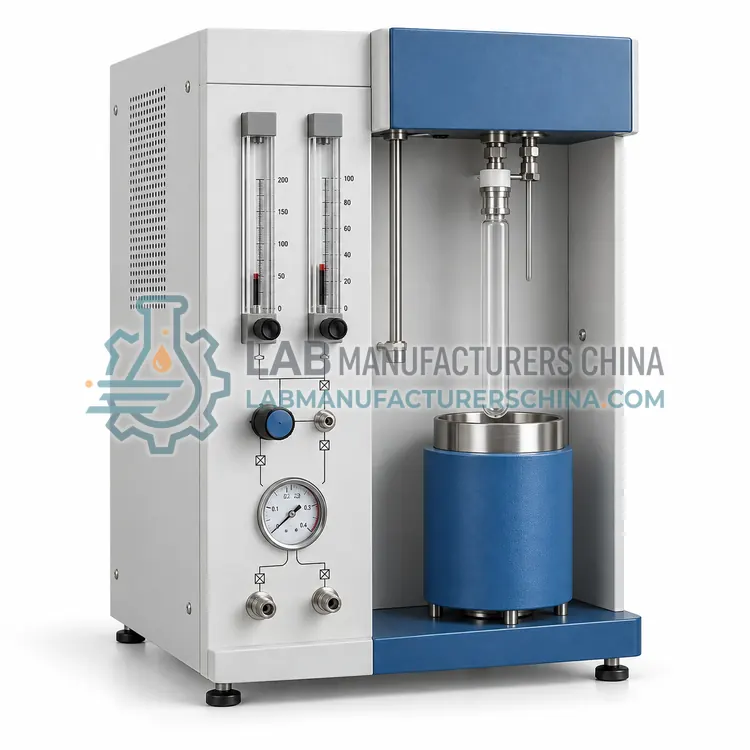
Single-Point Flow BET Surface Area Analyzer for Powder QC
粉体质控单点流动法 BET 比表面积分析仪
- CE (to be confirmed)
- +1
Welcome to Lab Manufacturers China — laboratory instruments direct from a Chinese manufacturer
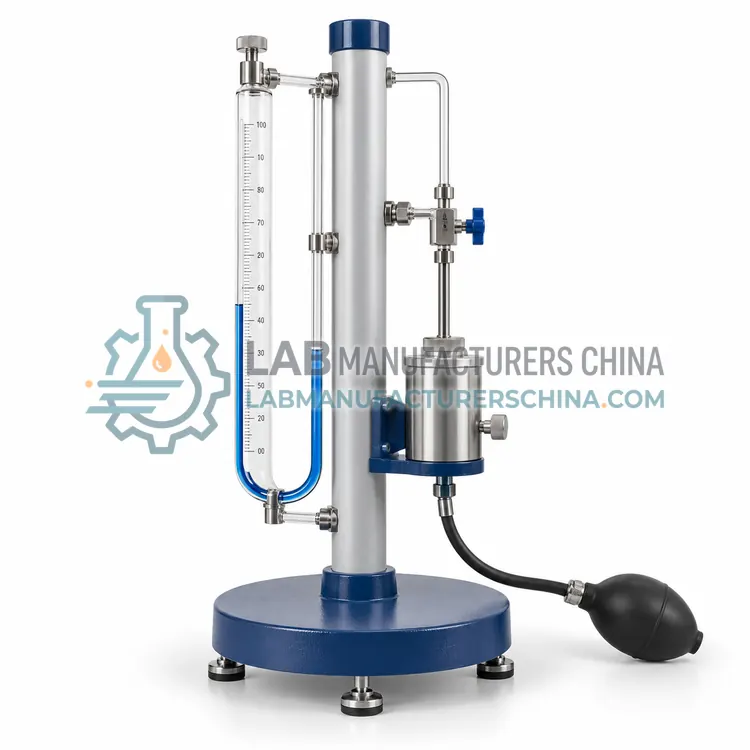
水泥和细粉用 Blaine 透气仪
Price on request — FOB / CIF quoted per order
Prices depend on configuration, quantity and destination port.
| Measurement principle | Air permeability (Kozeny–Carman) |
|---|---|
| Specific surface range | 100–1000 m²/kg |
| Bed porosity | 0.500 (typical for cement) |
| Cell diameter | 12.70 ± 0.05 mm |
| Bed height | 15 ± 1 mm |
| Timing | Manual or IR automatic, 0.1 s |
By Lab Manufacturers China Technical TeamLast reviewed Standards: ISO 9277, ASTM D3663, ASTM C204
A manual or automatic air permeability apparatus that measures the specific surface of cement and similar fine powders by timing air flow through a compacted bed of defined porosity. It provides the Blaine fineness value in m²/kg used in cement standards and production control.
A manual or automatic air permeability apparatus that measures the specific surface of cement and similar fine powders by timing air flow through a compacted bed of defined porosity. It provides the Blaine fineness value in m²/kg used in cement standards and production control.
The Blaine apparatus consists of a permeability cell, perforated disc, a U-shaped manometer, and a pump. A weighed mass of cement is compacted to a defined porosity, typically 0.500, in the cell. Air is drawn through the bed and the time for the manometer liquid to fall between two marks is measured. Specific surface is proportional to the square root of time for a given porosity, temperature and viscosity, per the Kozeny–Carman relation, and is calibrated with a standard reference cement. Standards EN 196-6 and ASTM C204 specify the procedure. Automatic versions use infrared sensors and digital timers. Results, typically 250 to 600 m²/kg for cements, are sensitive to bed porosity, humidity and sample preparation. The method captures external surface only, so it is not interchangeable with nitrogen BET.
Gas adsorption methods expose a degassed powder to nitrogen at 77 K. Adsorbed gas quantity is measured at several relative pressures, and the Brunauer–Emmett–Teller (BET) equation converts the monolayer capacity into surface area using the molecular cross-sectional area of nitrogen, 0.162 nm². Static volumetric systems dose known gas volumes and calculate uptake from pressure changes. Dynamic flow systems pass a nitrogen–helium mixture over the sample and detect adsorption and desorption by a thermal conductivity detector. Air permeability methods, such as Blaine or Fisher-type apparatus, measure the resistance to airflow through a packed powder bed of defined porosity, and the Kozeny–Carman relation gives specific surface area. Key components include sample tubes, degassing stations, pressure transducers, Dewar flask or cryogenic bath, and calibrated volumes.
A typical blaine air permeability apparatus for cement and fine powders configuration offers measurement principle of Air permeability (Kozeny–Carman), specific surface range of 100–1000 m²/kg, bed porosity of 0.500 (typical for cement), cell diameter of 12.70 ± 0.05 mm, bed height of 15 ± 1 mm and timing of Manual or IR automatic, 0.1 s. Values are indicative of the product class; the exact figures for each configuration are confirmed on the quotation and the calibration documents supplied with the instrument.
The Blaine Air Permeability Apparatus for Cement and Fine Powders is used in cement fineness in plant laboratories, fly ash and slag fineness, lime and gypsum powders, ceramic raw materials and mineral filler quality control. Across the wider Surface Area Analyzers class, laboratories also deploy it for cement fineness control, battery electrode and cathode powders and catalyst supports and activated carbon.
Relevant standards and methods include ISO 9277, ASTM D3663, ASTM C204, EN 196-6, ASTM D6556, ISO 15901-2 and GB/T 19587. Certification candidates for this model are CE and ISO 9001 manufacturing; each is to be confirmed for the specific configuration before shipment, and certificates are supplied only where they have been issued.
Sample preparation strongly affects surface area. Degas powders at a temperature and time that remove moisture and volatiles without altering the structure, and use the same protocol for every batch. Weigh samples accurately after degassing, because mass error transfers directly to the result. Keep the cryogenic bath level and cold trap stable, use high-purity nitrogen and helium, and check for leaks. Verify calibration with certified reference materials of known surface area. For air permeability, control bed porosity, temperature and humidity, and calibrate with a reference powder. Record degassing conditions and the BET pressure range in reports, and follow IQ/OQ/PQ practice where regulated.
Choose the Blaine apparatus for cement, fly ash and similar powders where standards prescribe air permeability fineness. Specify manual or automatic timing, cell type to EN 196-6 or ASTM C204, and supply of reference cement. It cannot replace BET for nanopowders, porous materials or powders with internal surface.
Choose according to the material and the decision that depends on the result. Cement and fine powders in production control are commonly measured by air permeability because it is fast and standardised. Nanopowders, catalysts supports and battery materials need gas adsorption to capture surfaces that permeability cannot. Single-point flow instruments give quick QC numbers, while multipoint static systems provide a full BET isotherm and validate linearity and C constant. Consider the expected surface area range, because materials under 1 m²/g require krypton or larger sample masses. Check the number of stations, degassing capability, liquid nitrogen handling, and whether results must follow ISO 9277 or ASTM D3663. Software features for automatic BET range selection per ISO 9277 and Rouquerol criteria reduce operator bias.
| Measurement principle | Air permeability (Kozeny–Carman) |
|---|---|
| Specific surface range | 100–1000 m²/kg |
| Bed porosity | 0.500 (typical for cement) |
| Cell diameter | 12.70 ± 0.05 mm |
| Bed height | 15 ± 1 mm |
| Timing | Manual or IR automatic, 0.1 s |
| Sample mass | ≈ 2.8–3.0 g (cement) |
| Manometer liquid | Dibutyl phthalate or mineral oil |
| Repeatability | ≤ 1% RSD with reference cement |
| Standards | EN 196-6, ASTM C204 |
Indicative values for this product class. Final specifications are confirmed on the quotation and in the calibration documents supplied with the instrument.
Results are expressed in square metres per kilogram (m²/kg), with portland cements commonly between 300 and 500 m²/kg. The value reflects external surface area determined from air permeability.
Specific surface calculated from permeability depends strongly on the porosity. Compaction at the specified porosity, using the correct sample mass from density, is required for results to be comparable.
Calibrate with a reference cement at regular intervals and whenever the cell or manometer is replaced. The standards require that the apparatus constant is determined with certified reference materials.
BET surface area is the specific surface area of a material calculated from nitrogen adsorption isotherm data using the Brunauer–Emmett–Teller model. It is expressed in m²/g and includes accessible external and pore surface for the probe molecule.
Blaine fineness is determined by air permeability and reflects the external surface of a packed bed, typically 250 to 500 m²/kg for cement. BET uses gas adsorption and also measures internal and rough surfaces, so values are higher.
Adsorbed water and volatiles block surface sites and would be released during measurement, distorting results. Degassing under vacuum or flowing gas at an appropriate temperature cleans the surface without damaging the sample.
粉体质控单点流动法 BET 比表面积分析仪
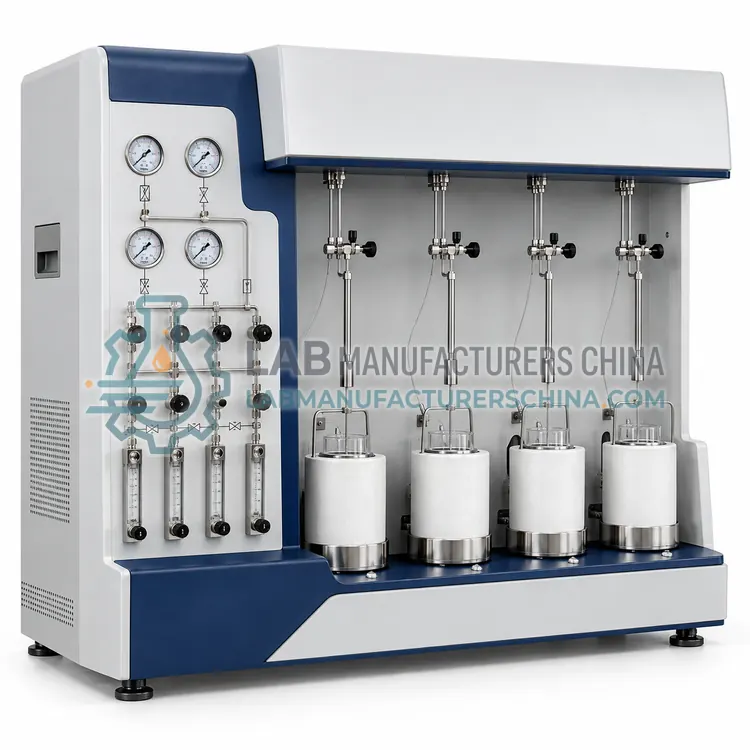
多工位静态容量法粉体 BET 比表面积分析仪
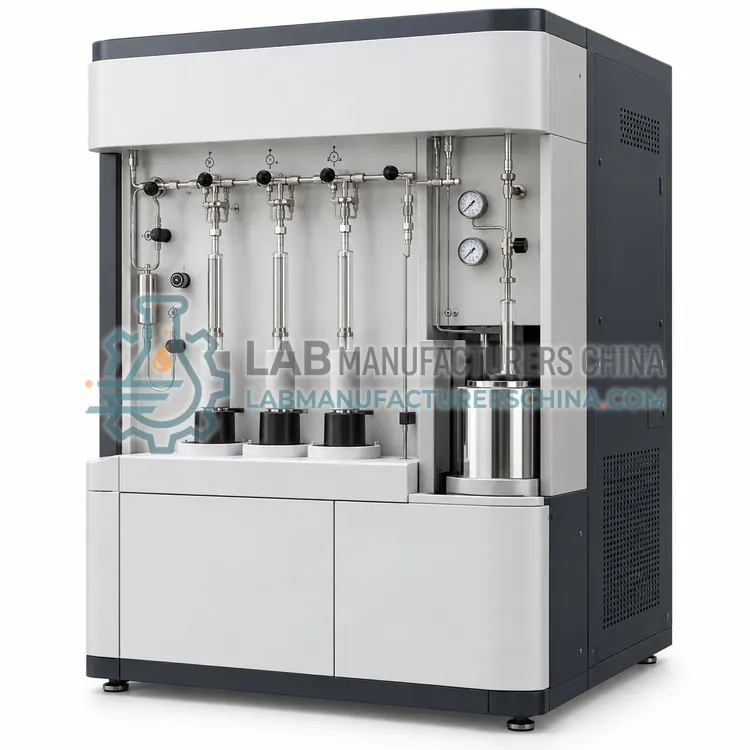
带微孔选项的纳米粉体细颗粒 BET 比表面积分析仪