How do Vacuum Pumps work?
Vacuum pumps remove gas molecules to lower pressure in a sealed volume. Positive-displacement types, including rotary vane, diaphragm, scroll and roots pumps, trap a volume of gas and push it out. Momentum-transfer pumps, including turbomolecular and diffusion pumps, accelerate molecules toward an exhaust that a backing pump removes. Water-ring and ejector pumps use a liquid or a jet to entrain and carry gas away. Performance is described by ultimate or base pressure and by pumping speed, which is measured in liters per second or cubic meters per hour. Real performance also depends on the gas load, on outgassing from chamber walls, and on the conductance of the connecting piping. Vapor handling, corrosion resistance and cleanliness determine which pump suits a given process, and pumps are often combined in stages to cover a wide pressure range.
Which Vacuum Pumps variants are available?
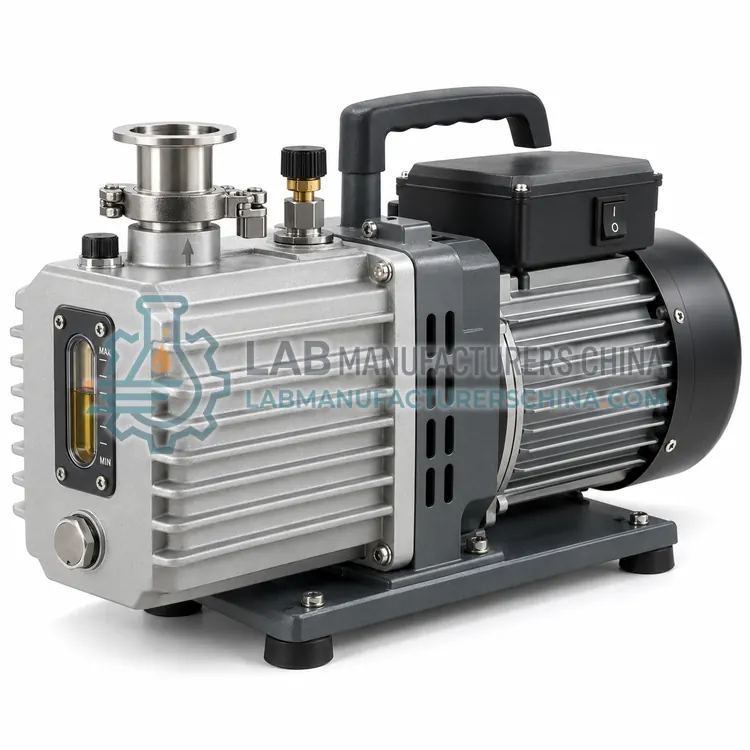
- Two-Stage Rotary Vane Vacuum Pump — A two-stage rotary vane vacuum pump reaches about 0.5 to 0.05 mbar and is the workhorse for medium-vacuum laboratory work.
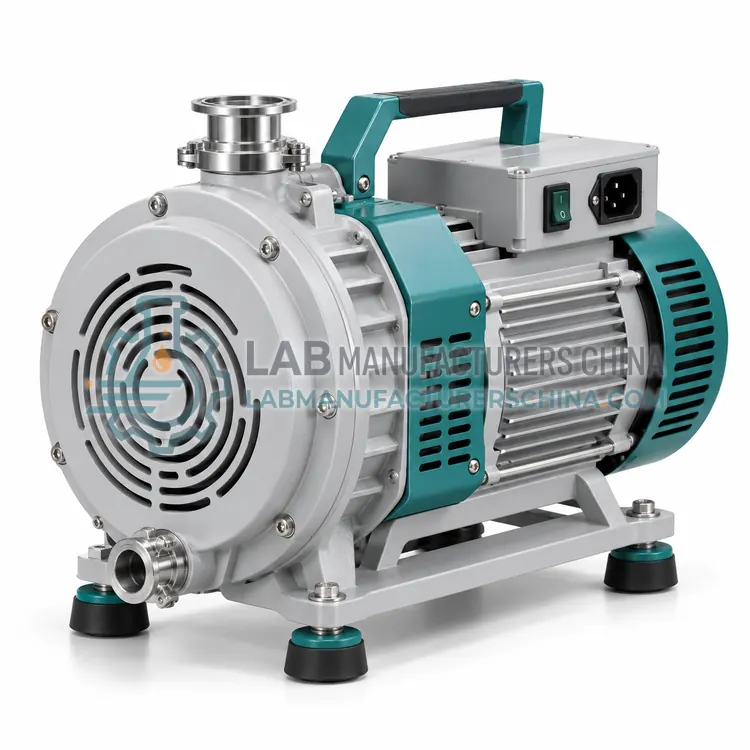
- Oil-Free Scroll Vacuum Pump — An oil-free scroll vacuum pump uses interleaved spiral scrolls to reach about 0.1 to 0.01 mbar without oil.
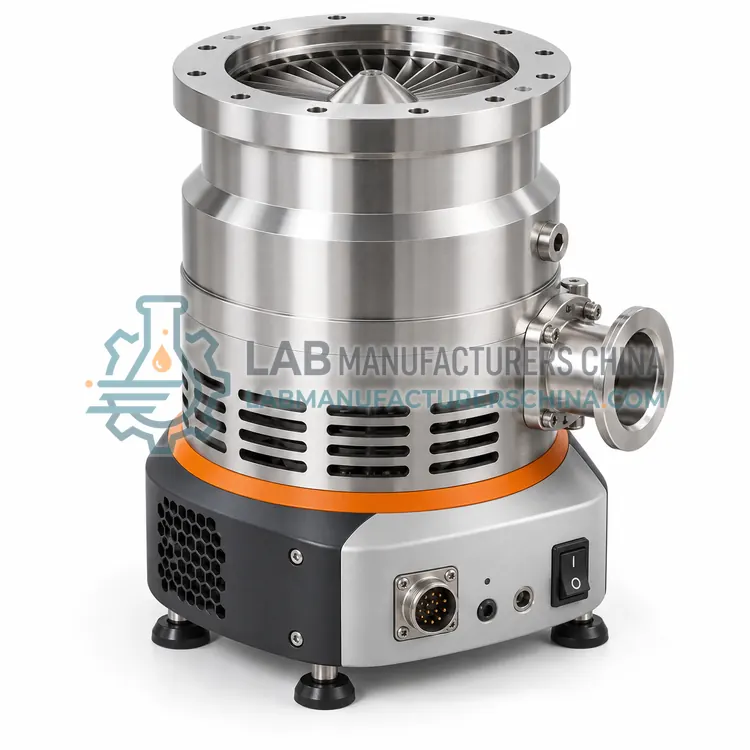
- Turbomolecular Vacuum Pump — A turbomolecular pump uses rapidly rotating blades to reach high and ultra-high vacuum below 10⁻⁶ mbar.
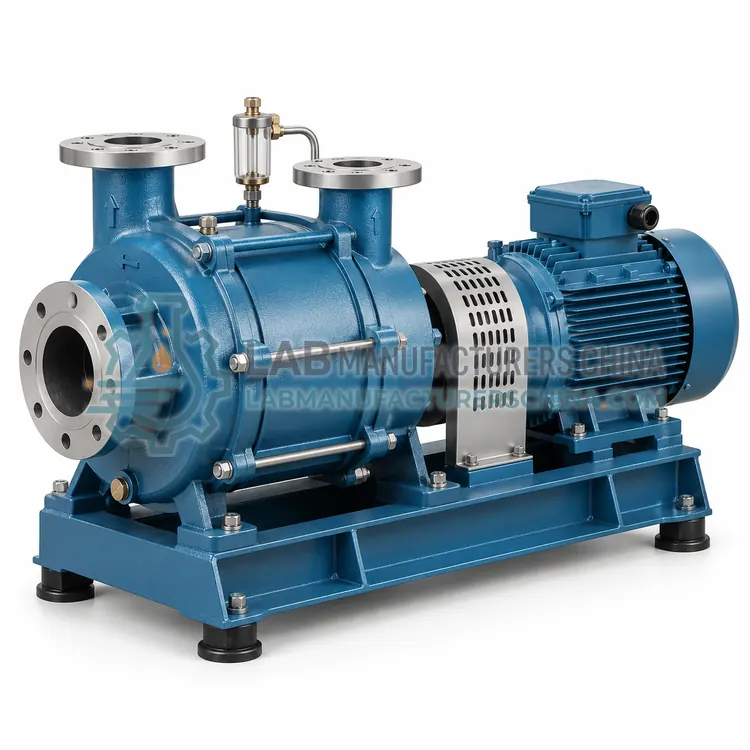
- Water-Ring Vacuum Pump — A water-ring vacuum pump uses a rotating water ring as the sealing and compressing element, reaching about 30 to 50 mbar.
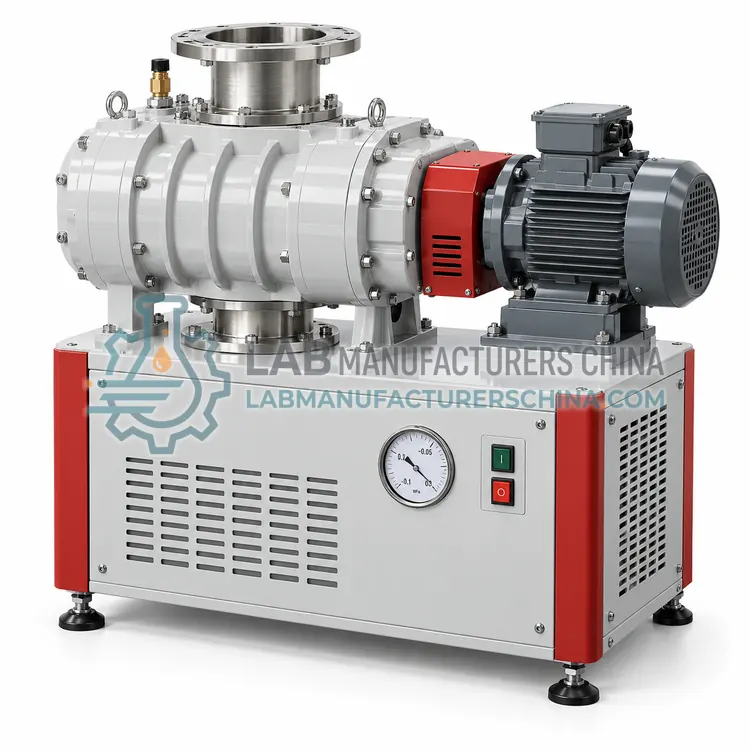
- Roots Vacuum Booster Pump — A roots vacuum booster pump uses two rotating lobes to increase the pumping speed of a backing pump in the medium-vacuum range.
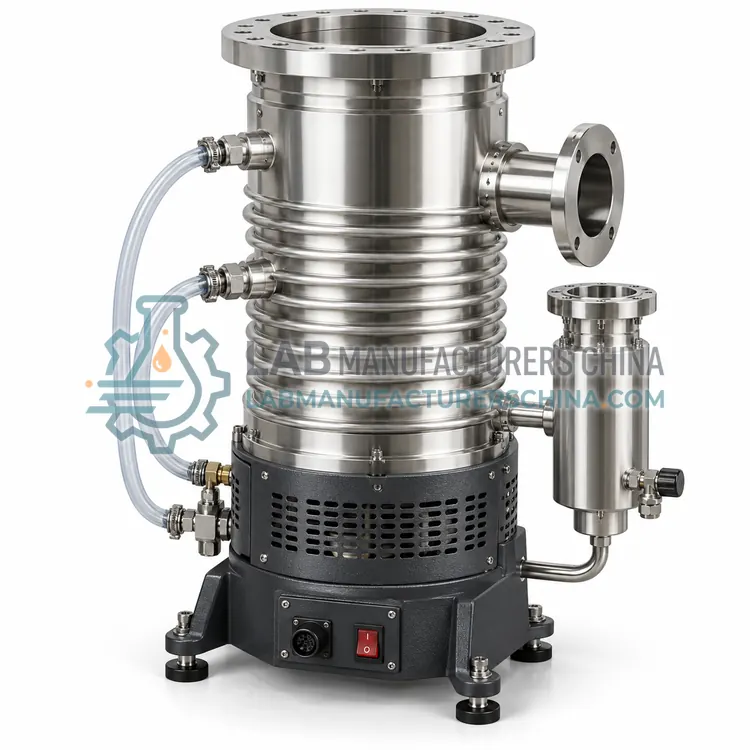
- Diffusion Vacuum Pump — A diffusion vacuum pump uses a boiling oil jet to reach high vacuum with no moving parts.
How do I choose the right variant?
Work from the required working pressure, the gas composition and the volume to be evacuated. For rough vacuum in filtration and drying, a diaphragm or single-stage rotary vane pump is sufficient. For medium vacuum in rotary evaporation and coating, a two-stage rotary vane or scroll pump is appropriate. For high and ultra-high vacuum in electron optics, surface analysis and semiconductor work, a turbomolecular pump with a suitable backing pump is needed. Consider whether the gas is condensable, corrosive or particle-laden, and add traps, filters and corrosion-resistant materials as required. Size pumping speed from the chamber volume, the target pressure and the acceptable pump-down time, remembering that conductance limits real speed. Decide between oil-sealed and dry designs based on contamination risk, and specify gauges, valves and controllers as part of the system.
Where are Vacuum Pumps used?
Vacuum Pumps are specified in chamber evacuation for drying and degassing, rotary evaporation and distillation, freeze drying and centrifugal concentration, sputtering and evaporation coating, electron microscopy and surface analysis and leak detection and vacuum testing.
Which standards and certifications apply?
Work with Vacuum Pumps is commonly governed by IEC 61010-1, IEC 61326-1, ISO 21360, ISO 27893, ISO 20485 and GB 4793.1. Instrument certifications such as CE marking are confirmed per configuration and never assumed.
What are the key considerations before purchase?
Protect the pump from the process with a cold trap, foreline trap or filter, and vent to atmosphere before switching off a high-vacuum pump. Change oil and check seals on schedule for oil-sealed pumps, and inspect scroll tips and diaphragms for dry pumps. Keep tubing as short and wide as possible to preserve conductance, and use the correct flange type and vacuum grease sparingly. Monitor pressure with gauges appropriate to the range, such as Pirani, capacitance or ion gauges. Follow IEC 61010-1 for electrical safety and local pressure equipment rules. For oil-free or clean processes, confirm that the pump cannot backstream oil or particles. Record base pressure and pump-down curves during commissioning and at each service so that degradation is detected early.