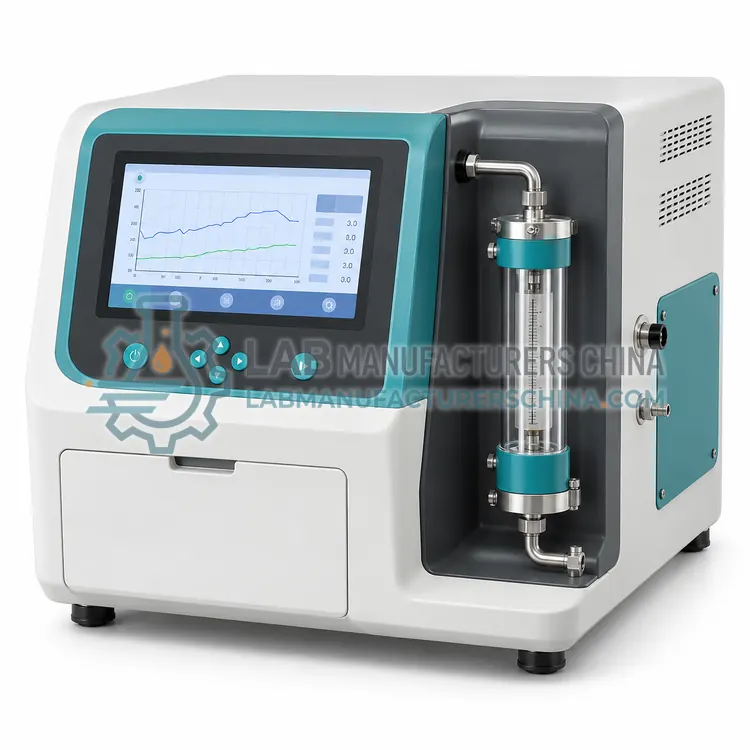
How do Emission Monitoring work?
Emission monitors determine pollutants in hot, wet and dusty flue gas. Extractive systems withdraw a sample through a heated probe and line at 180 °C, remove particles with a filter, and either keep the gas hot for analysis or dry it in a chiller before measurement. Analyzers use non-dispersive infrared for CO, CO2 and SO2, chemiluminescence or UV for NOx, paramagnetic or zirconia cells for O2, and FTIR for multi-component measurement. In-situ systems measure across the stack using tunable diode laser absorption or UV. Particulate monitors use light scattering, transmissometry for opacity, or triboelectric signals, and flow is measured by differential pressure pitot tubes or ultrasonic transit time. A data acquisition system normalizes values to reference oxygen, dry basis and standard conditions, applies calibration and reports averages.
Which Emission Monitoring variants are available?
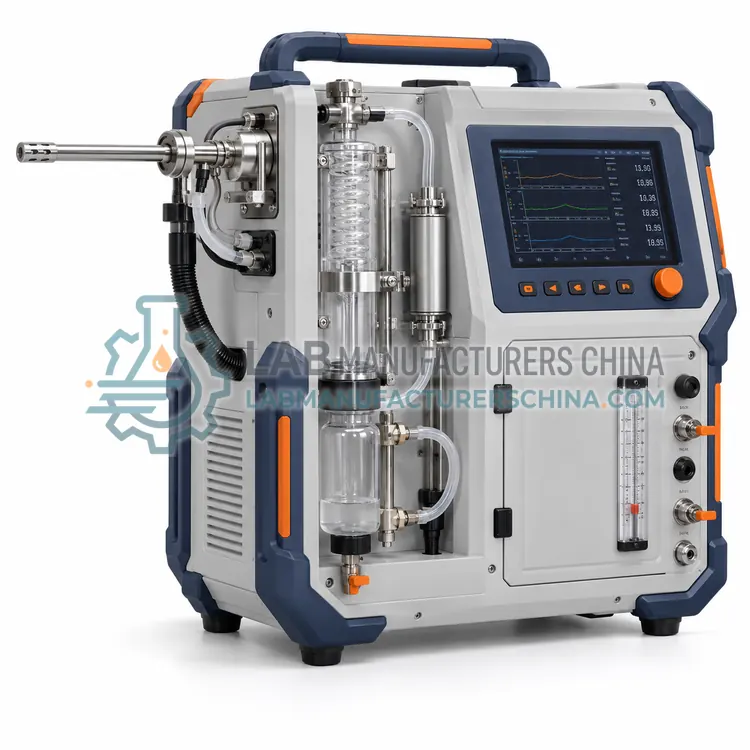
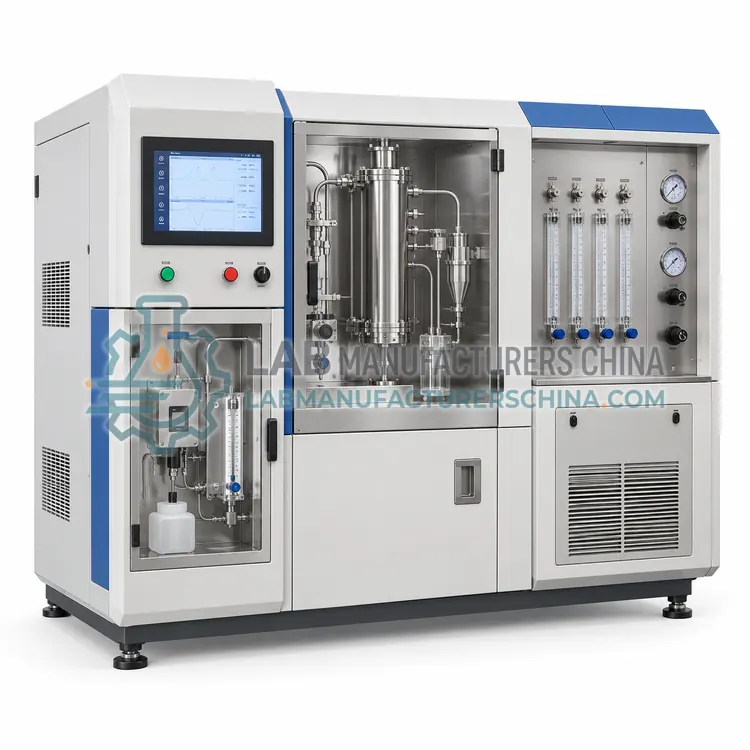
- Extractive Hot-Wet CEMS for Multi-Gas Stack Monitoring — A system that extracts flue gas through a heated probe and line to a cabinet where SO2, NOx, CO, CO2 and O2 are measured without drying the sample.
- Cold-Dry Extractive CEMS with Sample Conditioning — An extractive system that cools the sample to about 4 °C to remove water before measuring SO2, NOx, CO, CO2 and O2 on a dry basis.
- In-Situ Laser Gas Analyzer for Stack and Duct — A cross-duct tunable diode laser analyzer that measures gases such as HCl, NH3, O2, CO and H2O directly in the flue gas without extraction.
- Stack Dust and Opacity Monitor — An optical instrument that continuously measures particulate emissions in a stack by light scattering or transmission, reporting relative dust concentration or opacity.
- Stack Gas Flow and Velocity Monitor — A monitor that measures gas velocity, temperature and volumetric flow in a stack using ultrasonic transit time, differential pressure pitot tubes or thermal mass sensing.
How do I choose the right variant?
Start with the regulated pollutants, emission limits and the standard your permit cites, such as EN 14181 or HJ 75. Decide between extractive and in-situ systems according to stack temperature, moisture, acid gas content and the number of species: extractive suits multi-component and low-level measurements, while in-situ suits single gases and fast response. Check that measurement ranges are suitable for the limits, with limits in the lower third of the range where possible. Consider reporting requirements for averaging, data validation and certified instrument status under schemes such as EN 15267 or China CEMS certification. Include sample conditioning maintenance, calibration gas logistics, shelter size and the ability to cope with wet scrubber stacks.
Where are Emission Monitoring used?
Emission Monitoring are specified in coal and gas power plant stacks, cement and lime kiln emissions, waste incineration monitoring, chemical and petrochemical process stacks and steel and glass furnace emissions.
Which standards and certifications apply?
Work with Emission Monitoring is commonly governed by EN 14181, EN 15267-3, EN 15259, ISO 12039, US EPA 40 CFR Part 60, US EPA 40 CFR Part 75, HJ 75 and HJ 76. Instrument certifications such as CE marking are confirmed per configuration and never assumed.
What are the key considerations before purchase?
Choose sampling locations that meet EN 15259 or HJ/T 397 requirements for straight duct length and port access, because flow profile affects representativeness. Keep heated lines above the acid dew point to prevent condensation and corrosion, and replace probe filters and pump heads regularly. Perform daily automatic zero and span checks, quarterly or annual linearity checks, and an annual surveillance test against a standard reference method under EN 14181 QAL3 and AST. Protect cabinets from dust and temperature extremes, and provide calibration gas cylinders with certified uncertainties. Keep records of maintenance, calibration and data substitution, since regulators audit these, and train operators in safe work on platforms.