Automated Optical Tablet Inspection System
自动光学片剂检测系统
- SKU TAI-0002
- Tablet Inspection
- CE (to be confirmed)
- ISO 9001 manufacturing (to be confirmed)
Price on request — FOB / CIF quoted per order
Prices depend on configuration, quantity and destination port.
Key specifications
| Throughput | 50,000–300,000 tablets/h |
|---|---|
| Tablet size range | 3–25 mm |
| Camera type | Area or line-scan, 5–12 MP |
| Minimum defect size | approx. 0.1–0.2 mm |
| Inspected surfaces | Top, bottom, optional edge |
| Rejection method | Air jet |
Request a quote Download brochure · to be provided
By Lab Manufacturers China Technical TeamLast reviewed Standards: USP <1>, Ph. Eur. 2.9.40, ISO 9001
What is the Automated Optical Tablet Inspection System?
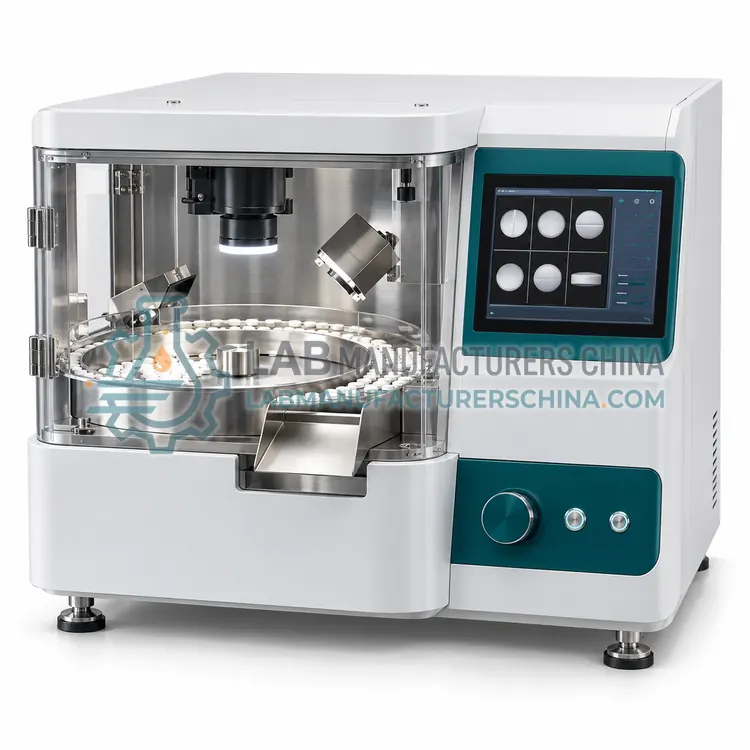
An automated optical tablet inspection system images each tablet on both sides with cameras and software, then rejects units with visual defects. It provides consistent, documented inspection at production-line speeds for most tablet shapes.
What is the Automated Optical Tablet Inspection System?
An automated optical tablet inspection system images each tablet on both sides with cameras and software, then rejects units with visual defects. It provides consistent, documented inspection at production-line speeds for most tablet shapes.
Overview
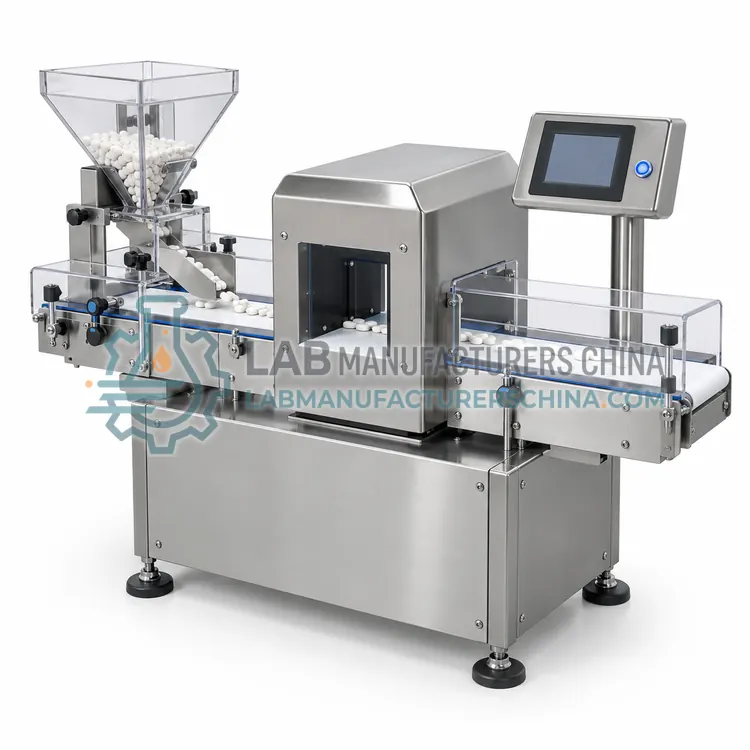
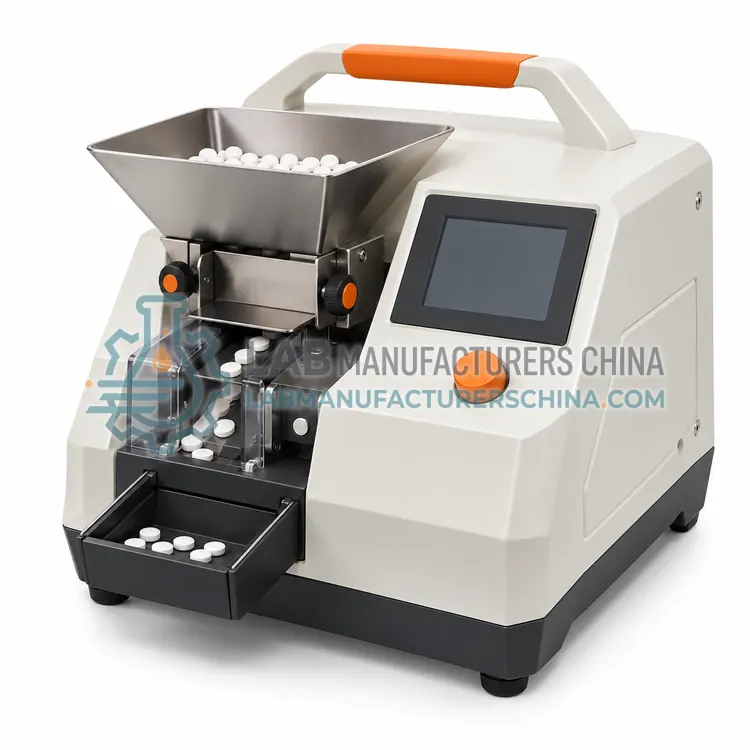
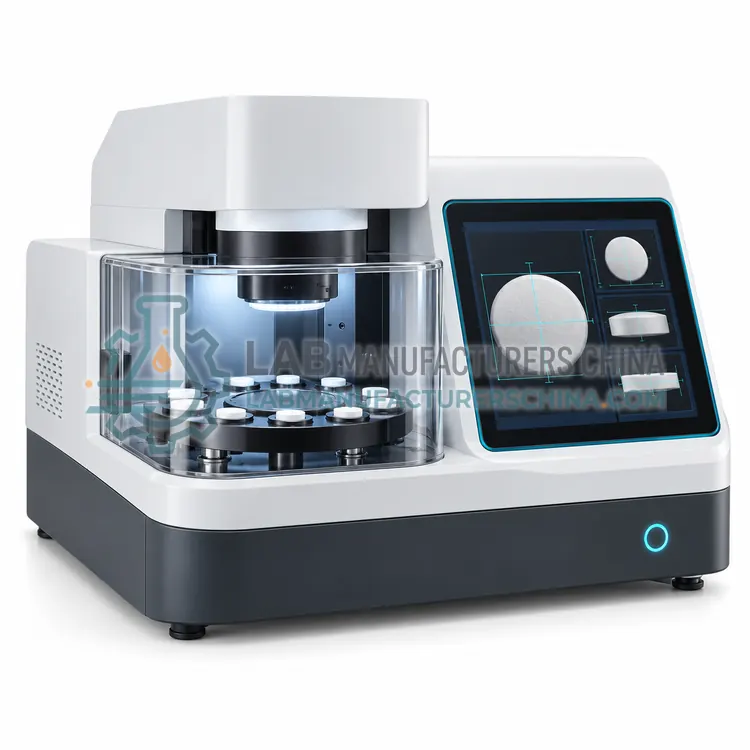
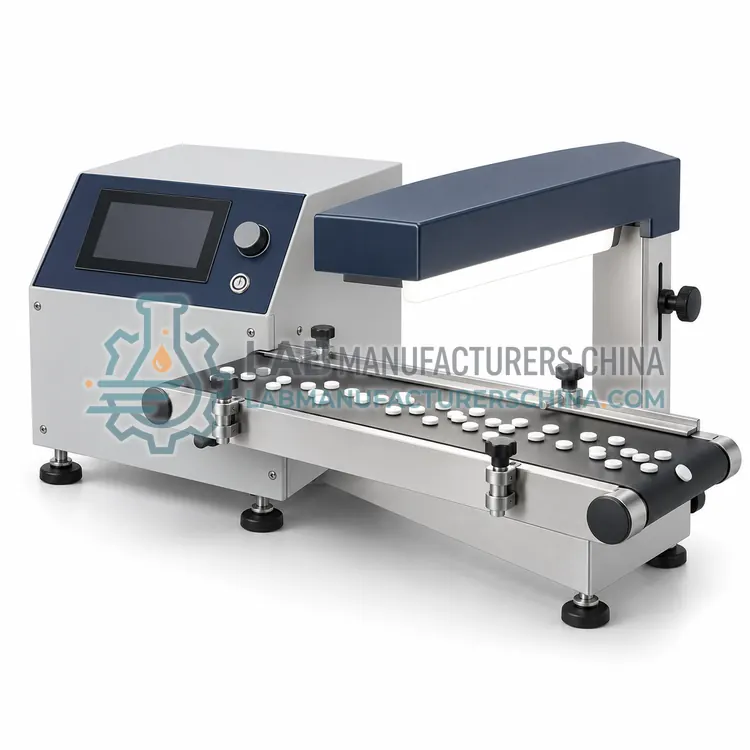
The system feeds tablets through a vibratory track or along a belt and presents them to high-resolution cameras with controlled lighting. Area-scan or line-scan cameras image the top and bottom faces, and sometimes the edge. The software compares each image with the learned reference and evaluates chips, cracks, spots, color deviation, size, shape and print legibility. Units exceeding set thresholds are removed by a precisely timed air jet. Throughput is typically 50,000 to 300,000 tablets per hour depending on configuration. The operator trains the system using good tablets and defect examples, and may adjust sensitivity for each product. The images of rejected tablets can be stored for investigation. Changeover needs format parts, recipe selection and a verification step, and optical components require regular cleaning and calibration.
How does it work?
Tablet inspection combines several physical principles. Vision systems illuminate tablets with controlled light and capture images with area or line-scan cameras, and software compares shape, color, surface texture and printing with a learned reference to detect chips, cracks, spots, capping and double-pressed units. Metal detectors use a balanced coil system that produces an electromagnetic field, and a disturbance caused by ferrous or non-ferrous metal triggers a reject. Checkweighers measure mass as tablets pass over a load cell or electromagnetic force restoration cell, and reject units outside set limits. Manual inspection tables use lighting and a moving belt so that trained inspectors can view both sides of the tablet. Rejection is typically by an air jet or diverter gate, and data are logged for trend analysis.
What are the key features?
- High-resolution cameras inspect top and bottom faces
- Software detects chips, cracks, spots, color and print errors
- Air-jet rejection timed to the individual tablet
- Image storage of rejected tablets for investigation
- Recipe storage for quick product changeover
- Throughput up to 300,000 tablets per hour
What are the technical specifications?
A typical automated optical tablet inspection system configuration offers throughput of 50,000–300,000 tablets/h, tablet size range of 3–25 mm, camera type of Area or line-scan, 5–12 MP, minimum defect size of approx. 0.1–0.2 mm, inspected surfaces of Top, bottom, optional edge and rejection method of Air jet. Values are indicative of the product class; the exact figures for each configuration are confirmed on the quotation and the calibration documents supplied with the instrument.
Which applications is it used for?
The Automated Optical Tablet Inspection System is used in high-speed tablet production lines, printed and coated tablet inspection, pre-packaging quality assurance and contract manufacturing. Across the wider Tablet Inspection class, laboratories also deploy it for visual defect detection in tablet production, foreign-matter control and weight control of finished tablets.
Which standards and certifications apply?
Relevant standards and methods include USP <1>, Ph. Eur. 2.9.40, ISO 9001, IEC 61010-1 and EN 60529. Certification candidates for this model are CE and ISO 9001 manufacturing; each is to be confirmed for the specific configuration before shipment, and certificates are supplied only where they have been issued.
Install inspection equipment on a stable, vibration-free surface with controlled lighting, because ambient light and vibration affect vision and weighing accuracy. Validate detection sensitivity with certified test pieces, for example ferrous, non-ferrous and stainless steel spheres for metal detectors, and with known defect samples for vision systems. Perform challenge tests at start-up, at set intervals and after changeover. Keep optics, belts and chutes clean and protect metal detector coils from nearby metal and electrical interference. Maintain calibration records for checkweighers with traceable test weights. Under GMP, document qualification, control reject handling and ensure rejected tablets are segregated and investigated.
How do I select the right Automated Optical Tablet Inspection System?
Select this system when defect criteria are visual, volumes are high and consistent, documented inspection is required. For trial or small batches, a manual belt is enough. In an RFQ, state tablet sizes and shapes, throughput, minimum defect size, reject method, recipe count and integration requirements.
How does it compare with other Tablet Inspection variants?
Match the inspection method to the defect you need to catch. Vision inspection addresses appearance, chips, cracks, color and print, while metal detection addresses contamination from machinery wear, and checkweighing addresses fill weight. Manual inspection is flexible and low cost but subjective and slower. Consider throughput, expressed in tablets per minute, and ensure the system can keep pace with the press or packaging line. Check the size range and shapes supported, as oblong, biconvex and scored tablets are more difficult to image. Sensitivity specification, for example the smallest detectable ferrous sphere, should be stated. Regulated users should verify reject confirmation, audit trails and challenge testing procedures, and consider whether the system must integrate with upstream or downstream equipment.
Full specifications
| Throughput | 50,000–300,000 tablets/h |
|---|---|
| Tablet size range | 3–25 mm |
| Camera type | Area or line-scan, 5–12 MP |
| Minimum defect size | approx. 0.1–0.2 mm |
| Inspected surfaces | Top, bottom, optional edge |
| Rejection method | Air jet |
| Lighting | LED, multi-angle |
| Recipe memory | ≥ 100 products |
| Data output | Ethernet / USB |
| Power supply | 220 V, 50/60 Hz |
Indicative values for this product class. Final specifications are confirmed on the quotation and in the calibration documents supplied with the instrument.
Applications
- High-speed tablet production lines
- Printed and coated tablet inspection
- Pre-packaging quality assurance
- Contract manufacturing
Key features
- High-resolution cameras inspect top and bottom faces
- Software detects chips, cracks, spots, color and print errors
- Air-jet rejection timed to the individual tablet
- Image storage of rejected tablets for investigation
- Recipe storage for quick product changeover
- Throughput up to 300,000 tablets per hour
Frequently asked questions about Automated Optical Tablet Inspection System
Detectable defect size depends on camera resolution, tablet size and contrast. Systems commonly detect defects around 0.1 to 0.2 mm, but capability must be confirmed with your tablets and known defect samples.
Yes, if the camera resolution and lighting are suitable. The system can check the presence, position and legibility of printing, though verification for each print design is needed.
False rejection is controlled through sensitivity settings, good lighting and recipe training. Challenge testing with defect samples and good tablets establishes acceptable false-reject and missed-defect rates.
Tablet inspection equipment detects defects in tablets before packaging. It includes vision systems for appearance, metal detectors for contamination, and checkweighers for mass, and it automatically rejects units that fall outside preset criteria.
Vision systems detect chips, cracks, capping, spots, discoloration, double-pressed tablets, missing or misprinted marks, and wrong size or shape. Detection performance depends on lighting, tablet color, resolution and the learned reference.
Machinery wear, broken screens or punch fragments can introduce metal particles. A tablet metal detector identifies ferrous, non-ferrous and stainless steel contaminants that other methods cannot see, protecting patients and downstream equipment.
Related models