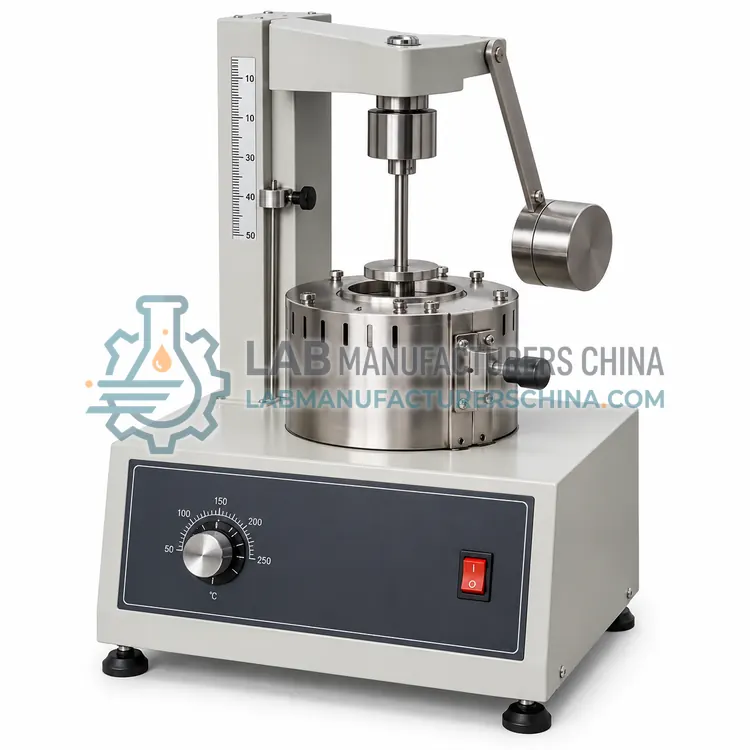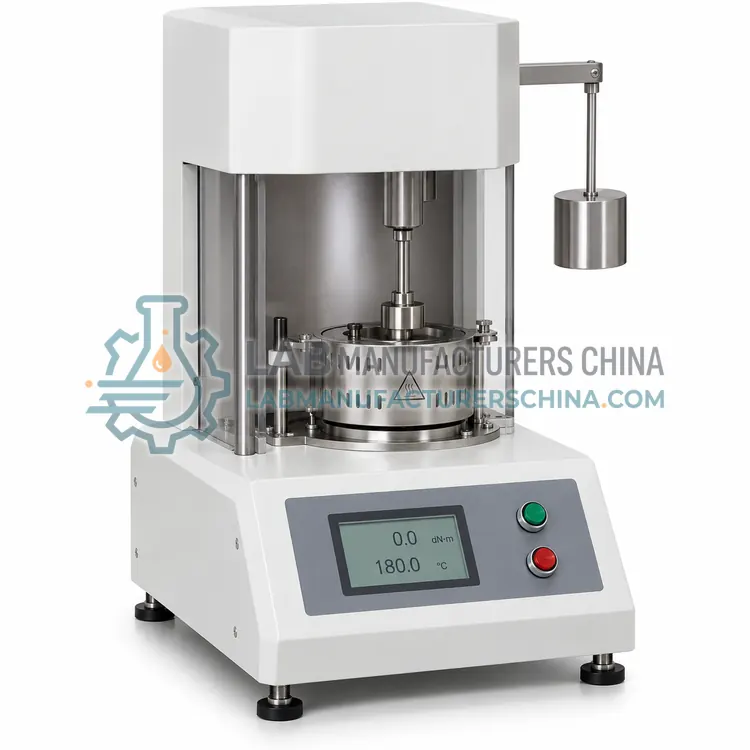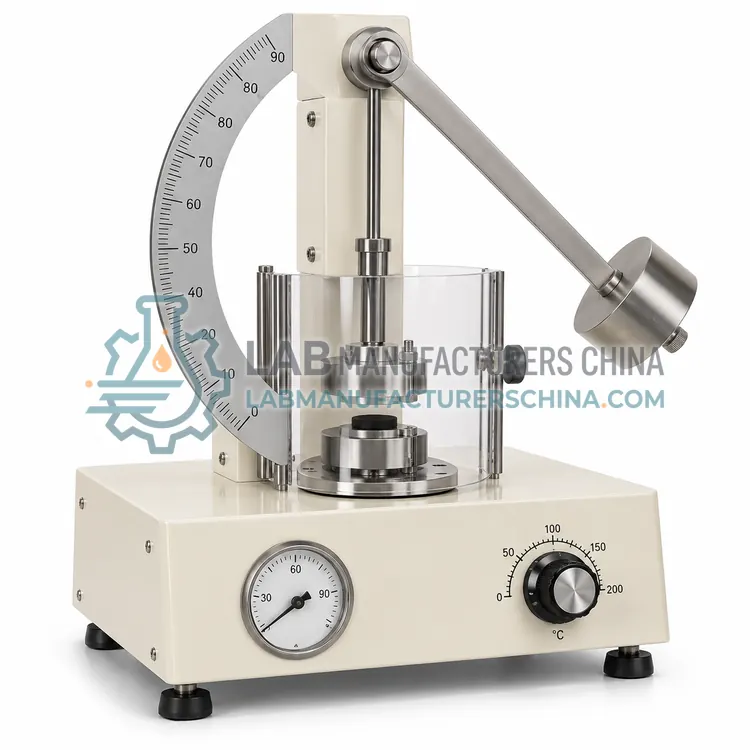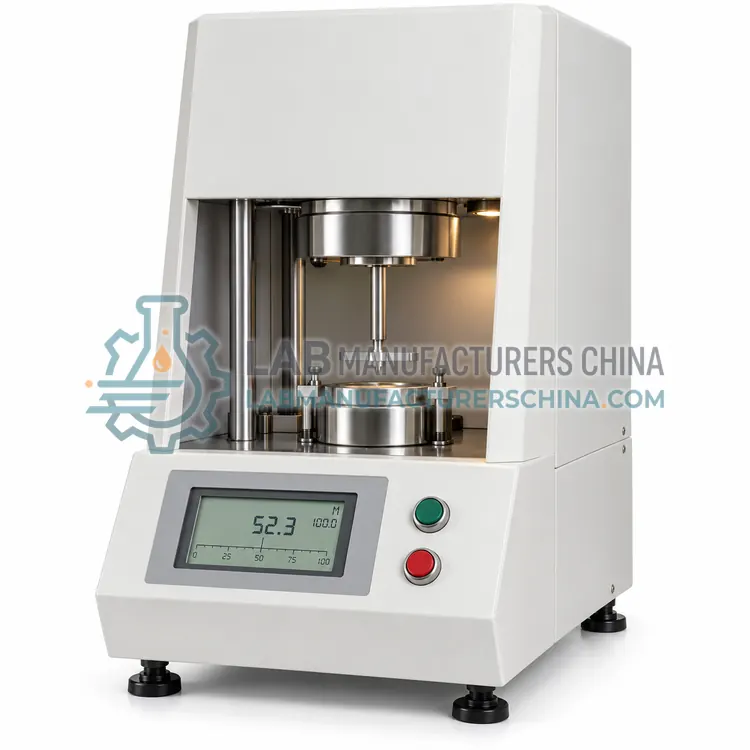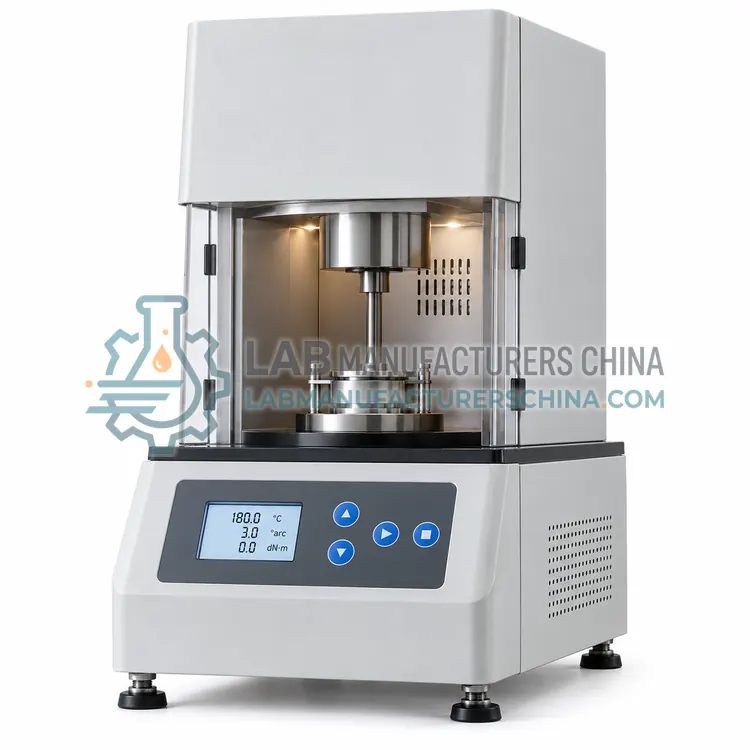
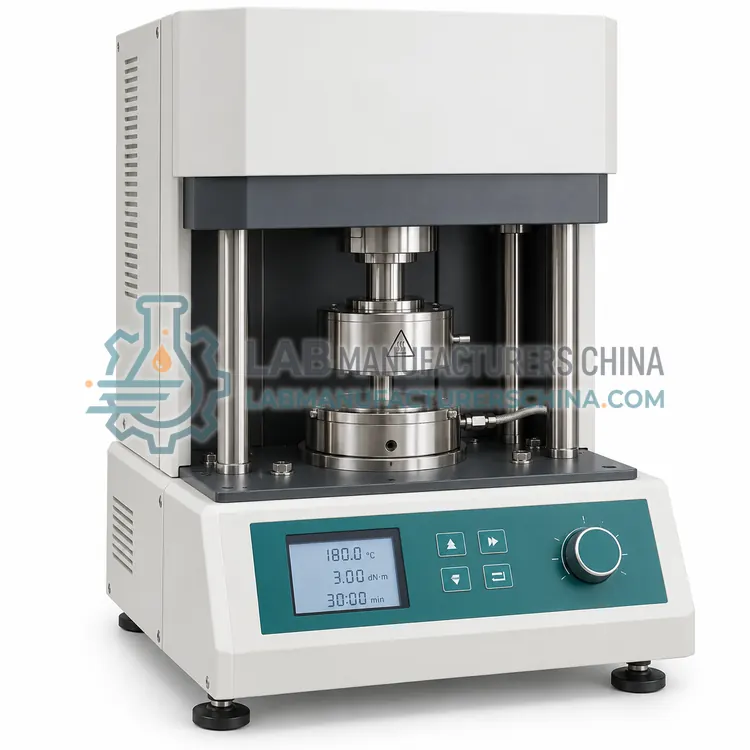
Rotational Rheometer for Rubber Compounds
橡胶混合料用旋转流变仪
- SKU RHM-0003
- Rheometers
- CE (to be confirmed)
- ISO 9001 manufacturing (to be confirmed)
Price on request — FOB / CIF quoted per order
Prices depend on configuration, quantity and destination port.
Key specifications
| Torque range | 0.1–200 mN·m |
|---|---|
| Strain range | 0.01–50% at curing temperature |
| Frequency range | 0.01–100 rad/s |
| Temperature range | Ambient to 250 °C |
| Temperature accuracy | ±0.5 °C |
| Geometry options | Parallel plates, closed cavity, serrated plates |
Request a quote Download brochure · to be provided
By Lab Manufacturers China Technical TeamLast reviewed Standards: ISO 6502-1, ISO 6502-2, ISO 6502-3
What is the Rotational Rheometer for Rubber Compounds?
A rotational rheometer applies controlled shear or oscillation to a rubber compound across a range of strain and frequency, measuring viscoelastic moduli rather than cure torque. It is used to study filler networking, processability and the effect of strain history.
Overview
The compound is held between parallel plates or in a closed cavity while the instrument applies steady shear or a small oscillatory strain, and the resulting torque or normal force is recorded. A strain sweep reveals the Payne effect, the drop in storage modulus as strain amplitude rises, which quantifies filler networking and is sensitive to carbon black or silica content, coupling agents and mixing quality. A frequency sweep characterises the viscoelastic response relevant to extrusion and moulding, and can be carried out at curing temperature to follow the rise in modulus while the compound is uncured. Because the material is rough and sticky, serrated plates or closed cavities are used to prevent slip, and specimen preparation by compression moulding directly from the mixed compound is part of the method.
How does it work?
An unvulcanised rubber compound is viscoelastic and its properties change as crosslinking proceeds, so a rheometer records torque or complex modulus against time at a fixed temperature. Curemeters hold the compound in a sealed cavity at vulcanisation temperature and oscillate a rotor or the cavity itself through a small arc, producing a cure curve from which scorch time, optimum cure time and minimum and maximum torque are read. Oscillating disc instruments turn a biconical rotor inside the sample, while rotorless instruments oscillate the lower die and measure the reaction torque on the upper die, giving faster thermal response and lower inertia. Rotational and dynamic mechanical instruments apply small strains over a frequency range to measure viscoelastic moduli, and capillary instruments push the compound through a die to measure process viscosity at extrusion rates.
What are the key features?
- Strain sweeps to quantify filler networking
- Frequency sweeps from 0.01 to 100 rad/s
- Closed cavity or serrated plates to prevent slip
- Temperature control to vulcanisation range
- Normal force measurement for elasticity
- Compression-moulded specimen accessories
What are the technical specifications?
A typical rotational rheometer for rubber compounds configuration offers torque range of 0.1–200 mN·m, strain range of 0.01–50% at curing temperature, frequency range of 0.01–100 rad/s, temperature range of Ambient to 250 °C, temperature accuracy of ±0.5 °C and geometry options of Parallel plates, closed cavity, serrated plates. Values are indicative of the product class; the exact figures for each configuration are confirmed on the quotation and the calibration documents supplied with the instrument.
Which applications is it used for?
The Rotational Rheometer for Rubber Compounds is used in filler networking and coupling agent evaluation, mix quality assessment for carbon black and silica compounds, processability and die swell prediction and uncured compound consistency testing. Across the wider Rheometers class, laboratories also deploy it for scorch and cure time determination for production control, compound development and accelerator selection and batch-to-batch consistency of mixed rubber.
Which standards and certifications apply?
Relevant standards and methods include ISO 6502-1, ISO 6502-2, ISO 6502-3, ASTM D2084, ASTM D5289, ASTM D6204, ASTM D5099, ASTM D5992 and IEC 61010-1. Certification candidates for this model are CE and ISO 9001 manufacturing; each is to be confirmed for the specific configuration before shipment, and certificates are supplied only where they have been issued.
Cavity cleanliness is the main source of error: cured residue from a previous test alters the torque reading, so dies should be cleaned after every specimen and inspected at intervals. Verify cavity temperature with a calibrated probe, because cure rate changes steeply with temperature and a one degree offset changes the optimum cure time measurably. Weigh or volume-dose specimens consistently, close the dies fully and record test temperature, arc amplitude and frequency with every curve. Condition compounds at standard temperature before testing, and store them away from heat. Calibration with reference compounds, such as a certified rubber standard, provides a periodic check on the whole measurement chain.
How do I select the right Rotational Rheometer for Rubber Compounds?
Choose a rotational rheometer when cure parameters alone are not enough, for example when comparing silica compounds with different coupling systems, investigating a mixing problem, or quantifying the Payne effect as a process control parameter. Confirm the strain and frequency ranges, and that a closed cavity is available for sticky high-filler compounds.
How does it compare with other Rheometers variants?
Begin with the standard your product or customer specifies. Rotorless curemeters dominate modern production control because they reach thermal equilibrium quickly and give repeatable scorch and cure times, while oscillating disc instruments remain in use where historical data or older specifications require them. Where the interest is the compound's response to varying strain and frequency, for example in filler networking or processability studies, a rotorless instrument with frequency sweep capability or a dedicated rotational rheometer is chosen. Capillary instruments are used when extrusion viscosity, die swell or the behaviour of a stiff or highly filled compound must be quantified. For vulcanised rubber, dynamic mechanical analysis describes the viscoelastic behaviour that governs damping, heat build-up and fatigue.
Full specifications
| Torque range | 0.1–200 mN·m |
|---|---|
| Strain range | 0.01–50% at curing temperature |
| Frequency range | 0.01–100 rad/s |
| Temperature range | Ambient to 250 °C |
| Temperature accuracy | ±0.5 °C |
| Geometry options | Parallel plates, closed cavity, serrated plates |
| Normal force range | 0.01–20 N |
| Specimen volume | 1–5 cm³ |
| Purge gas | Nitrogen or air |
| Power supply | 220 V, 50/60 Hz |
Indicative values for this product class. Final specifications are confirmed on the quotation and in the calibration documents supplied with the instrument.
Applications
- Filler networking and coupling agent evaluation
- Mix quality assessment for carbon black and silica compounds
- Processability and die swell prediction
- Uncured compound consistency testing
Key features
- Strain sweeps to quantify filler networking
- Frequency sweeps from 0.01 to 100 rad/s
- Closed cavity or serrated plates to prevent slip
- Temperature control to vulcanisation range
- Normal force measurement for elasticity
- Compression-moulded specimen accessories
Frequently asked questions about Rotational Rheometer for Rubber Compounds
The Payne effect is the drop in storage modulus as strain amplitude increases, caused by breakage of the filler network built up during mixing. Its magnitude reflects filler content, dispersion quality and coupling efficiency, so a strain sweep is a sensitive check on mixing consistency even when cure curves look identical.
Rubber compounds are stiff and slightly rough, so smooth plates allow the specimen to slip during the measurement, which produces a falsely low modulus. Serrated or grooved plates grip the specimen and ensure that the imposed strain is actually transmitted, which is essential for reliable strain sweep data.
Yes. Running a time sweep at vulcanisation temperature shows storage modulus rising as crosslinking proceeds, which gives a curing profile that complements a curemeter. Because the geometry differs from a sealed cavity, the values are not identical to curemeter torque, but the trend can be compared with process data.
The curve plots torque against time at constant temperature. Minimum torque indicates the viscosity of the unvulcanised compound, the time to a defined torque rise above minimum gives scorch time, and the time to 90% of the maximum torque rise gives optimum cure time. Maximum torque and the shape after the peak show the degree and stability of crosslinking.
The two designs impose different strain fields and have different thermal masses, so absolute torque values differ and cure times shift slightly even for the same compound. Both are valid within their own standard, but data from one type should not be compared directly with data from the other, and specifications must state the instrument type.
A calibrated thermocouple or a reference compound with a known cure response is used. Thermocouple verification checks the die surface, while a reference compound such as a certified rubber standard checks the whole system, including closing pressure and die condition. Both checks are normally performed at defined intervals and recorded.
Related models