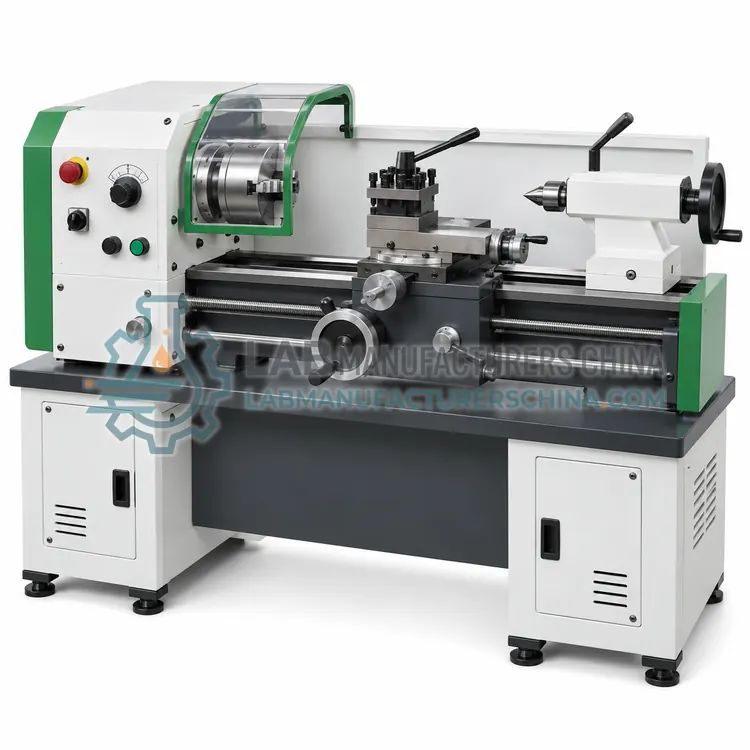
Laboratory Lathe for Metal Sample Turning
实验室金属试样车床
- SKU SAR-0004
- Sample Preparation
- CE (to be confirmed)
- ISO 9001 manufacturing (to be confirmed)
Price on request — FOB / CIF quoted per order
Prices depend on configuration, quantity and destination port.
Key specifications
| Swing over bed | 200–400 mm |
|---|---|
| Spindle speed | 100–2500 rpm, variable |
| Insert material | Tungsten carbide or ceramic |
| Surface roughness achieved | Ra about 1–3 µm |
| Maximum sample length | 500–1000 mm |
| Chip collection | Tray under the tool holder |
Request a quote Download brochure · to be provided
By Lab Manufacturers China Technical TeamLast reviewed Standards: ISO 14284, ASTM E1806, ASTM E3
What is the Laboratory Lathe for Metal Sample Turning?
A laboratory lathe turns a clean, flat surface on a metal sample and simultaneously produces chips for analysis, so one preparation serves both optical emission and combustion methods. It handles cylindrical and disc samples.
What is the Laboratory Lathe for Metal Sample Turning?
A laboratory lathe turns a clean, flat surface on a metal sample and simultaneously produces chips for analysis, so one preparation serves both optical emission and combustion methods. It handles cylindrical and disc samples.
Overview
The sample is clamped in a chuck or between centres, and a carbide or ceramic insert tool turns the surface at a controlled speed and depth. Because the tool is rigid and the cutting action is continuous, the resulting surface is flat with a roughness suitable for spark excitation, and the chip curls can be collected for carbon, sulfur and gas analysis from the same sample. Lathes are used where samples are long or heavy, such as drill rods, pipe sections and bar stock, and where the surface must be cut rather than milled because of the geometry. Coolant can be used where a flat surface is the priority, or omitted where chips must remain uncontaminated, and the choice and the parameters should be recorded. Tool geometry, cutting speed and feed determine whether the surface is smeared or the chips burnt.
How does it work?
Metal analysis requires a surface or chip that is uniform, free of contamination and undamaged by heat, because spark optical emission, X-ray fluorescence and combustion methods all sample a small volume of material. A cut-off saw with coolant sections a bar or a casting without heating it above the tempering range. A milling machine or lathe removes the surface layer, which may be decarburized, scaled, coated or altered by earlier machining, to expose sound metal with a defined roughness. A drill press or lathe generates chips for combustion analysis of carbon, sulfur, oxygen, nitrogen and hydrogen, with cutting parameters chosen to avoid smearing or burning the chips. Ferroalloys and some raw materials are too hard or too coarse for these methods and are crushed or ground first. In every case the tool material and the cleaning routine matter, because residues of iron, aluminium, copper or previous samples bias the result.
What are the key features?
- Chuck or between-centres clamping for long samples
- Carbide or ceramic insert tooling
- Variable spindle speed and feed
- Chip collection tray under the tool
- Coolant option for surface quality
- Surface finish suitable for spark excitation
What are the technical specifications?
A typical laboratory lathe for metal sample turning configuration offers swing over bed of 200–400 mm, spindle speed of 100–2500 rpm, variable, insert material of Tungsten carbide or ceramic, surface roughness achieved of Ra about 1–3 µm, maximum sample length of 500–1000 mm and chip collection of Tray under the tool holder. Values are indicative of the product class; the exact figures for each configuration are confirmed on the quotation and the calibration documents supplied with the instrument.
Which applications is it used for?
The Laboratory Lathe for Metal Sample Turning is used in turning surfaces on bar, rod and pipe samples, chip sampling for combustion analysis, preparation of long specimens for emission analysis and machining of cast and forged test pieces. Across the wider Sample Preparation class, laboratories also deploy it for surface preparation before spark optical emission, chip sampling for carbon and sulfur determination and sectioning of castings and weld macros.
Which standards and certifications apply?
Relevant standards and methods include ISO 14284, ASTM E1806, ASTM E3, ASTM E415, ASTM E1019 and IEC 61010-1. Certification candidates for this model are CE and ISO 9001 manufacturing; each is to be confirmed for the specific configuration before shipment, and certificates are supplied only where they have been issued.
Control cutting parameters: use coolant as specified, avoid dwelling with a blunt tool and discard the first part of any cut if it has been scorched. Clean machines and tools between samples with brushes, solvent and, where relevant, a purge block of the same material, and keep the number of tools per sample type fixed so procedure is reproducible. Record the surface condition or chip size, because methods specify acceptable limits and results can be rejected if preparation is not documented. Maintain coolant quality and replace it on schedule, since contaminated coolant leaves deposits that interfere with sparks. When crushing ferroalloys, use tungsten carbide jaws and bowls and be aware that the powder may be pyrophoric in fine form. Guard rotating tools, provide extraction for dust and fume, and store samples so identity cannot be lost.
How do I select the right Laboratory Lathe for Metal Sample Turning?
Select the lathe where samples are long, heavy or cylindrical and the same preparation must yield both a surface and chips. Specify swing, spindle speed range, tooling and chip collection, and decide in advance whether cutting will be dry or with coolant.
How does it compare with other Sample Preparation variants?
Choose equipment from the analytical method that follows. Spark optical emission needs a flat, machined surface of specified roughness and freedom from cracks and porosity, so a milling machine or a lathe is essential; portable analysers may accept a ground surface instead. Combustion and inert gas fusion methods need chips of a defined size produced without overheating, so a drill press with controlled feed or a lathe with the right tool geometry is used, and the chips are cleaned with solvent and a magnet where appropriate. Metallographic work needs a cut-off saw that sections with minimal damage and a mounting system for subsequent grinding and polishing. Ferroalloys need crushing and grinding to a fine powder with tungsten carbide tooling to avoid iron and chromium contamination. Plan for sample identification and traceability, because a mix-up between heats is a bigger error source than instrument precision.
Full specifications
| Swing over bed | 200–400 mm |
|---|---|
| Spindle speed | 100–2500 rpm, variable |
| Insert material | Tungsten carbide or ceramic |
| Surface roughness achieved | Ra about 1–3 µm |
| Maximum sample length | 500–1000 mm |
| Chip collection | Tray under the tool holder |
| Coolant | Optional, flood or dry cutting |
| Power supply | 380 V, 50/60 Hz, three phase |
Indicative values for this product class. Final specifications are confirmed on the quotation and in the calibration documents supplied with the instrument.
Applications
- Turning surfaces on bar, rod and pipe samples
- Chip sampling for combustion analysis
- Preparation of long specimens for emission analysis
- Machining of cast and forged test pieces
Key features
- Chuck or between-centres clamping for long samples
- Carbide or ceramic insert tooling
- Variable spindle speed and feed
- Chip collection tray under the tool
- Coolant option for surface quality
- Surface finish suitable for spark excitation
Frequently asked questions about Laboratory Lathe for Metal Sample Turning
Yes, if the preparation is done correctly: the turned surface is used for spark excitation and the chips collected during the same cut are used for carbon, sulfur and gas determination, provided they are not overheated.
When chips are needed for combustion or gas analysis, because coolant would contaminate them. Dry cutting requires lower speed and sharp tools to avoid burning the chips and to keep the surface acceptable.
Turning rotates the sample against a single-point tool, so it suits cylindrical and long parts and can produce chips in one operation. Milling traverses a rotating cutter over a stationary sample, which suits flat discs and blocks.
Cutting generates heat that can temper or anneal the specimen, altering hardness, microstructure and gas content. Coolant removes that heat so the sectioned surface still represents the original material.
A flat surface machined to the roughness stated in the method, free from cracks, porosity, scale, coatings and oxide, with the specimen thick enough to dissipate heat so sparks do not burn through it.
With a drill press or lathe using sharp tools and moderate parameters so the chips are not discoloured or burnt, then cleaned with solvent, dried, and magnetically separated if magnetic contamination is a concern.
Related models
Inductively Coupled Plasma Optical Emission Spectrometer for Metal Assay
金属测定用电感耦合等离子体发射光谱仪
- CE (to be confirmed)
- +1