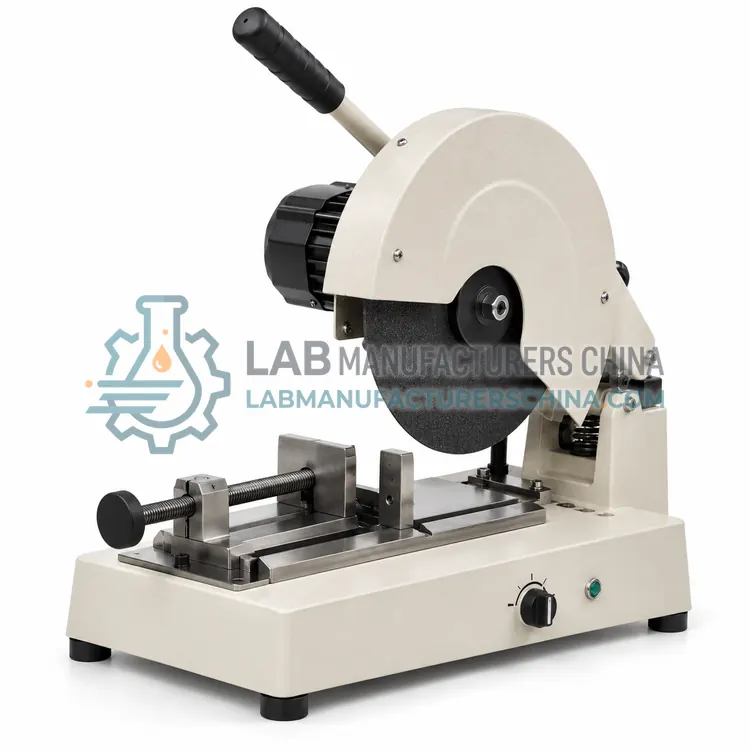
Abrasive Cut-Off Saw for Metal Specimens
金属试样切割机
- SKU SAR-0001
- Sample Preparation
- CE (to be confirmed)
- ISO 9001 manufacturing (to be confirmed)
Price on request — FOB / CIF quoted per order
Prices depend on configuration, quantity and destination port.
Key specifications
| Wheel diameter | 200–350 mm |
|---|---|
| Maximum section | 60–150 mm diameter |
| Wheel speed | 2800–3800 rpm, low speed option 200–600 rpm |
| Feed control | Manual or automatic with load control |
| Coolant volume | 20–60 L |
| Clamping | Vice with quick-release or cam lock |
Request a quote Download brochure · to be provided
By Lab Manufacturers China Technical TeamLast reviewed Standards: ISO 14284, ASTM E1806, ASTM E3
What is the Abrasive Cut-Off Saw for Metal Specimens?
An abrasive cut-off saw sections metal bars, castings, welds and forgings with a cooled abrasive wheel, producing cut faces suitable for metallography or further preparation. It is the first step in almost every metallurgical sample routine.
What is the Abrasive Cut-Off Saw for Metal Specimens?
An abrasive cut-off saw sections metal bars, castings, welds and forgings with a cooled abrasive wheel, producing cut faces suitable for metallography or further preparation. It is the first step in almost every metallurgical sample routine.
Overview
The specimen is clamped in a vice and a consumable abrasive wheel, usually aluminium oxide or silicon carbide, is fed through it at a controlled rate while coolant floods the cut. Wheels are selected for hardness and material type: softer bonds for hard metals so fresh abrasive is exposed, harder bonds for soft metals. Flood cooling keeps the cut zone below the temperature that would alter hardness or microstructure, and cutting rate and pressure are adjusted so the wheel does not glaze or load. Larger models accept sections of 100 to 150 mm diameter, while precision saws with low-speed blades cut thin or delicate samples such as coated parts and brittle castings with minimal damage. After cutting, specimens are cleaned, dried and either mounted for metallography or prepared for surface analysis.
How does it work?
Metal analysis requires a surface or chip that is uniform, free of contamination and undamaged by heat, because spark optical emission, X-ray fluorescence and combustion methods all sample a small volume of material. A cut-off saw with coolant sections a bar or a casting without heating it above the tempering range. A milling machine or lathe removes the surface layer, which may be decarburized, scaled, coated or altered by earlier machining, to expose sound metal with a defined roughness. A drill press or lathe generates chips for combustion analysis of carbon, sulfur, oxygen, nitrogen and hydrogen, with cutting parameters chosen to avoid smearing or burning the chips. Ferroalloys and some raw materials are too hard or too coarse for these methods and are crushed or ground first. In every case the tool material and the cleaning routine matter, because residues of iron, aluminium, copper or previous samples bias the result.
What are the key features?
- Consumable abrasive wheel in aluminium oxide or silicon carbide
- Flood coolant system with tank and pump
- Controlled feed rate and clamping vice
- Cutting chamber with splash guard and drain
- Low speed precision option for delicate specimens
- Wheel selection for hard and soft metals
What are the technical specifications?
A typical abrasive cut-off saw for metal specimens configuration offers wheel diameter of 200–350 mm, maximum section of 60–150 mm diameter, wheel speed of 2800–3800 rpm, low speed option 200–600 rpm, feed control of Manual or automatic with load control, coolant volume of 20–60 L and clamping of Vice with quick-release or cam lock. Values are indicative of the product class; the exact figures for each configuration are confirmed on the quotation and the calibration documents supplied with the instrument.
Which applications is it used for?
The Abrasive Cut-Off Saw for Metal Specimens is used in sectioning bars and billets for analysis, weld macro and heat-affected zone specimens, cutting castings and forgings for metallography and preparation of samples for hardness traverses. Across the wider Sample Preparation class, laboratories also deploy it for surface preparation before spark optical emission, chip sampling for carbon and sulfur determination and sectioning of castings and weld macros.
Which standards and certifications apply?
Relevant standards and methods include ISO 14284, ASTM E1806, ASTM E3, ASTM E415, ASTM E1019 and IEC 61010-1. Certification candidates for this model are CE and ISO 9001 manufacturing; each is to be confirmed for the specific configuration before shipment, and certificates are supplied only where they have been issued.
Control cutting parameters: use coolant as specified, avoid dwelling with a blunt tool and discard the first part of any cut if it has been scorched. Clean machines and tools between samples with brushes, solvent and, where relevant, a purge block of the same material, and keep the number of tools per sample type fixed so procedure is reproducible. Record the surface condition or chip size, because methods specify acceptable limits and results can be rejected if preparation is not documented. Maintain coolant quality and replace it on schedule, since contaminated coolant leaves deposits that interfere with sparks. When crushing ferroalloys, use tungsten carbide jaws and bowls and be aware that the powder may be pyrophoric in fine form. Guard rotating tools, provide extraction for dust and fume, and store samples so identity cannot be lost.
How do I select the right Abrasive Cut-Off Saw for Metal Specimens?
Select the cut-off saw as the first machine in the sample flow, matching wheel diameter and maximum section to your largest specimens and adding low speed capability if you handle coatings or brittle materials. Specify coolant capacity, clamping arrangement and safety guarding.
How does it compare with other Sample Preparation variants?
Choose equipment from the analytical method that follows. Spark optical emission needs a flat, machined surface of specified roughness and freedom from cracks and porosity, so a milling machine or a lathe is essential; portable analysers may accept a ground surface instead. Combustion and inert gas fusion methods need chips of a defined size produced without overheating, so a drill press with controlled feed or a lathe with the right tool geometry is used, and the chips are cleaned with solvent and a magnet where appropriate. Metallographic work needs a cut-off saw that sections with minimal damage and a mounting system for subsequent grinding and polishing. Ferroalloys need crushing and grinding to a fine powder with tungsten carbide tooling to avoid iron and chromium contamination. Plan for sample identification and traceability, because a mix-up between heats is a bigger error source than instrument precision.
Full specifications
| Wheel diameter | 200–350 mm |
|---|---|
| Maximum section | 60–150 mm diameter |
| Wheel speed | 2800–3800 rpm, low speed option 200–600 rpm |
| Feed control | Manual or automatic with load control |
| Coolant volume | 20–60 L |
| Clamping | Vice with quick-release or cam lock |
| Cut damage depth | Typically 0.1–0.5 mm |
| Power supply | 380 V, 50/60 Hz, three phase |
Indicative values for this product class. Final specifications are confirmed on the quotation and in the calibration documents supplied with the instrument.
Applications
- Sectioning bars and billets for analysis
- Weld macro and heat-affected zone specimens
- Cutting castings and forgings for metallography
- Preparation of samples for hardness traverses
Key features
- Consumable abrasive wheel in aluminium oxide or silicon carbide
- Flood coolant system with tank and pump
- Controlled feed rate and clamping vice
- Cutting chamber with splash guard and drain
- Low speed precision option for delicate specimens
- Wheel selection for hard and soft metals
Frequently asked questions about Abrasive Cut-Off Saw for Metal Specimens
By grinding the sectioned face on successively finer papers, which removes the deformed and heat-affected zone. The depth of damage depends on wheel type, feed rate and cooling, and is typically a few tenths of a millimetre.
A softer-bonded aluminium oxide or silicon carbide wheel that wears back to expose fresh abrasive. Hard wheels glaze on hard steel, cut slowly and generate more heat, increasing the risk of altering the specimen.
A wheel guard, fixed and movable splash covers, an interlocked lid, secure clamping and an emergency stop. Abrasive wheels can burst, so rated speed, correct mounting flanges and inspection before fitting are essential.
Cutting generates heat that can temper or anneal the specimen, altering hardness, microstructure and gas content. Coolant removes that heat so the sectioned surface still represents the original material.
A flat surface machined to the roughness stated in the method, free from cracks, porosity, scale, coatings and oxide, with the specimen thick enough to dissipate heat so sparks do not burn through it.
With a drill press or lathe using sharp tools and moderate parameters so the chips are not discoloured or burnt, then cleaned with solvent, dried, and magnetically separated if magnetic contamination is a concern.
Related models