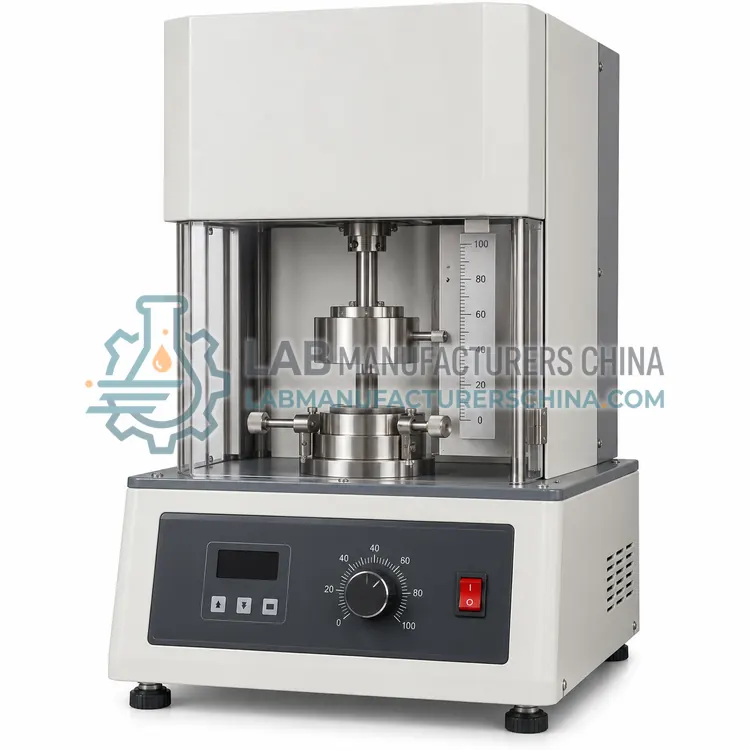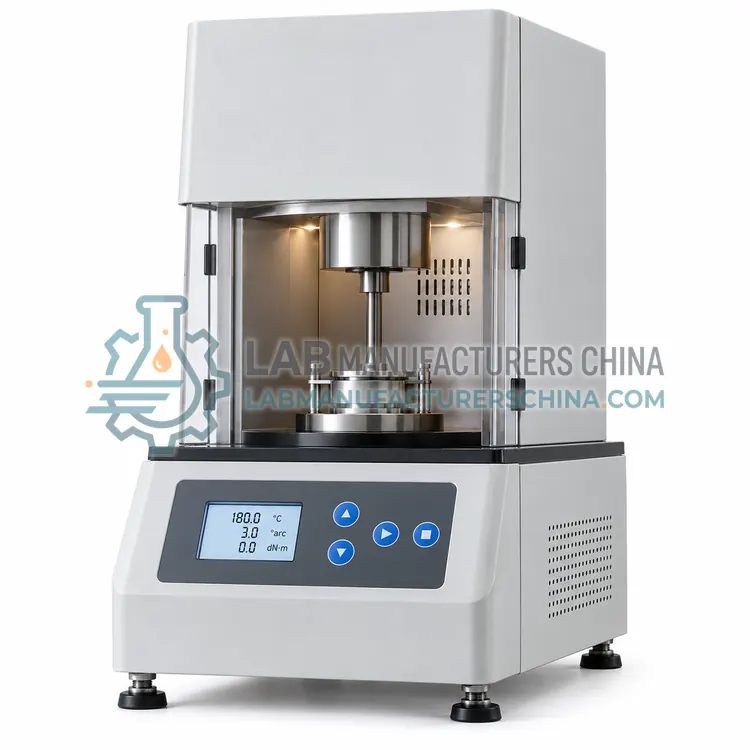
Mooney Viscometer for High-Viscosity and Highly Filled Compounds
高黏度高填充胶料用门尼黏度仪
- SKU MOV-0005
- Mooney Viscometers
- CE (to be confirmed)
- ISO 9001 manufacturing (to be confirmed)
Price on request — FOB / CIF quoted per order
Prices depend on configuration, quantity and destination port.
Key specifications
| Torque range | 0–400 Mooney units |
|---|---|
| Cavity temperature | 100 °C standard, up to 200 °C option |
| Temperature accuracy | ±0.3 °C |
| Rotor speed | 2.0 rpm |
| Drive power | Up to 1.5 kW |
| Specimen mass | About 10–12 g |
Request a quote Download brochure · to be provided
By Lab Manufacturers China Technical TeamLast reviewed Standards: ISO 289-1, ISO 289-2, ISO 289-4
What is the Mooney Viscometer for High-Viscosity and Highly Filled Compounds?
A high-torque Mooney viscometer is built to measure stiff, highly loaded compounds whose viscosity approaches the limit of standard instruments. It is used for rubber with high filler loading, very high molecular weight grades and reclaimed rubber.
Overview
When a compound is very stiff, the standard instrument may reach its torque limit before the curve plateaus, or the drive may stall during preheat. A high-torque configuration therefore uses a more powerful drive, a reinforced cavity and rotor assembly and a torque measurement range extended well beyond the standard 200 units, with the same cavity geometry so that results remain traceable to the method. Temperature control must be robust because a large mass of stiff compound takes longer to reach equilibrium and the heat generated by shearing is greater. Specimens may need to be pre-warmed or shaped to fit the cavity, and the method should state these steps, since a stiff compound is more sensitive to loading technique than a soft one.
How does it work?
A rubber specimen is placed in a grooved cylindrical cavity heated to the standard test temperature, usually 100 °C, and a serrated disc rotor is pressed into it. The rotor turns slowly, typically at 2 revolutions per minute, shearing the compound between rotor and cavity wall, and the torque needed to maintain rotation is converted into Mooney units. The specimen is preheated for a defined time so it reaches cavity temperature, then the rotor runs for a fixed period while the torque settles to a plateau, which is reported as the Mooney viscosity. Continued running beyond the standard time reveals scorch, and releasing the rotor at the end of the test allows Mooney stress relaxation to be measured, a parameter sensitive to molecular structure and to compound elasticity.
What are the key features?
- Extended torque range beyond standard units
- High-power drive for stiff compounds
- Reinforced cavity and rotor assembly
- Robust temperature control during shearing
- Programmable preheat for slow equilibration
- Same cavity geometry for traceability
What are the technical specifications?
A typical mooney viscometer for high-viscosity and highly filled compounds configuration offers torque range of 0–400 Mooney units, cavity temperature of 100 °C standard, up to 200 °C option, temperature accuracy of ±0.3 °C, rotor speed of 2.0 rpm, drive power of Up to 1.5 kW and specimen mass of About 10–12 g. Values are indicative of the product class; the exact figures for each configuration are confirmed on the quotation and the calibration documents supplied with the instrument.
Which applications is it used for?
The Mooney Viscometer for High-Viscosity and Highly Filled Compounds is used in highly filled technical rubber compounds, very high molecular weight raw rubber grading, reclaimed rubber viscosity control and abrasive compound testing with hard fillers. Across the wider Mooney Viscometers class, laboratories also deploy it for mooney viscosity grading of raw natural and synthetic rubber, batch consistency control at mixing plants and scorch and pre-vulcanisation checks.
Which standards and certifications apply?
Relevant standards and methods include ISO 289-1, ISO 289-2, ISO 289-4, ASTM D1646, ASTM D3346, GB/T 1232.1 and IEC 61010-1. Certification candidates for this model are CE and ISO 9001 manufacturing; each is to be confirmed for the specific configuration before shipment, and certificates are supplied only where they have been issued.
Verify cavity temperature with a calibrated probe, because Mooney viscosity falls steeply with temperature and a deviation of one degree changes the value measurably. Keep the rotor and cavity grooves free of cured rubber, since residue reduces the shearing volume and biases results. Use the standard specimen mass, preheat time and rotor speed, and note which of the standard times applies to your material. Condition specimens at standard laboratory temperature and test oily or tacky compounds consistently, because slip at the rotor surface lowers the reading. A reference rubber compound provides the routine check on the complete measurement chain.
How do I select the right Mooney Viscometer for High-Viscosity and Highly Filled Compounds?
Select a high-torque configuration when standard instruments stall, plateau late or exceed their torque range on your materials, which is common with heavily filled and very high molecular weight compounds. Confirm the drive power, the torque range and the preheat capability, and check whether hardened rotors are offered, since abrasive fillers wear the serrations and change the effective shearing geometry.
How does it compare with other Mooney Viscometers variants?
Choose the configuration from the compound and the purpose. Standard single-cavity instruments suit raw rubber incoming inspection and are the reference geometry for historical data. An instrument with automatic rotor release and stress relaxation measurement adds information about molecular structure and is preferred where compound elasticity affects shaping. Multi-cavity or automated instruments are justified when many batches are tested per shift or when raw rubber is graded automatically. Higher-temperature operation or a dedicated cavity may be needed for silicone compounds, which are measured at a different condition, and for very stiff or highly filled compounds the torque range and rotor design must be confirmed before selection.
Full specifications
| Torque range | 0–400 Mooney units |
|---|---|
| Cavity temperature | 100 °C standard, up to 200 °C option |
| Temperature accuracy | ±0.3 °C |
| Rotor speed | 2.0 rpm |
| Drive power | Up to 1.5 kW |
| Specimen mass | About 10–12 g |
| Preheat period | Up to 5 min programmable |
| Rotor material | Hardened and abrasion resistant |
| Data output | Torque curve and Mooney value |
Indicative values for this product class. Final specifications are confirmed on the quotation and in the calibration documents supplied with the instrument.
Applications
- Highly filled technical rubber compounds
- Very high molecular weight raw rubber grading
- Reclaimed rubber viscosity control
- Abrasive compound testing with hard fillers
Key features
- Extended torque range beyond standard units
- High-power drive for stiff compounds
- Reinforced cavity and rotor assembly
- Robust temperature control during shearing
- Programmable preheat for slow equilibration
- Same cavity geometry for traceability
Frequently asked questions about Mooney Viscometer for High-Viscosity and Highly Filled Compounds
Three signs are typical: the torque curve keeps rising without reaching a plateau within the standard test time, the recorded value approaches the top of the instrument range, or the rotor stalls during preheat. Any of these means the measured value is unreliable and a high-torque configuration is needed.
A stiff compound conducts heat slowly and a large specimen mass takes longer to reach cavity temperature, so the standard preheat may not be enough and the reading drifts during the run. Extending the preheat is acceptable if recorded, but the condition should still be verified with a reference compound of similar stiffness.
Abrasive fillers round off the rotor serrations, reducing grip on the compound and lowering the measured torque, which is often mistaken for a change in the material. Rotor dimensions and surface condition should be inspected at defined intervals and the rotor replaced when outside tolerance.
It indicates how stiff the unvulcanised compound is under the standard shearing condition. Higher values mean the rubber mixes, extrudes and shapes with more difficulty but usually has higher molecular weight and better green strength, while lower values flow more easily. Specifications set narrow ranges so that processing remains consistent.
After the rotor stops, the torque decays and the rate of decay is recorded. Fast relaxation indicates a narrow molecular weight distribution or less long-chain branching, while slow relaxation indicates the opposite. The parameter helps explain processing differences between raw rubber grades that have similar Mooney viscosity.
The compound must reach cavity temperature before the torque is meaningful, because viscosity depends strongly on temperature. The standard specifies a preheat period in which the rotor turns slowly or remains at low speed, and starting the measurement early gives a value that drifts during the run rather than plateauing.
Related models