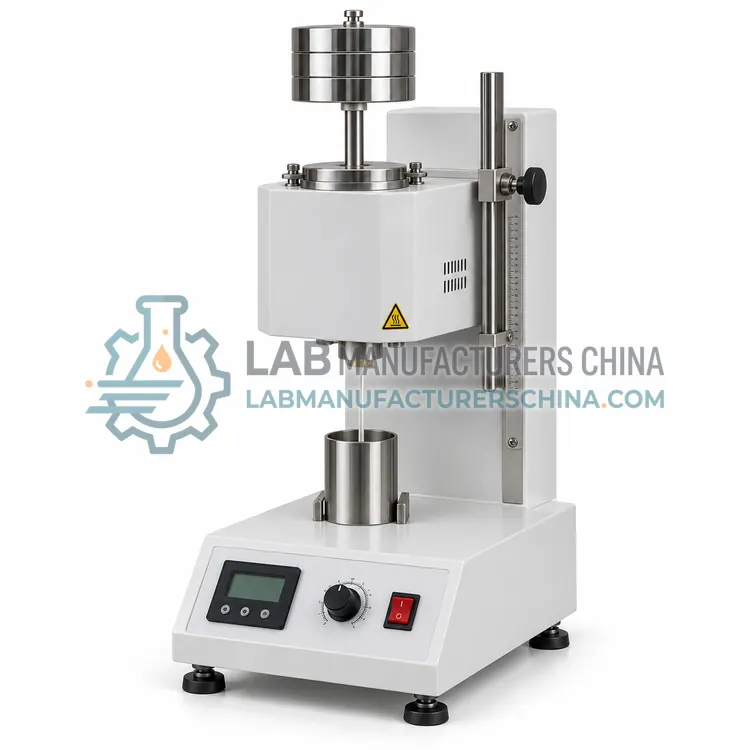
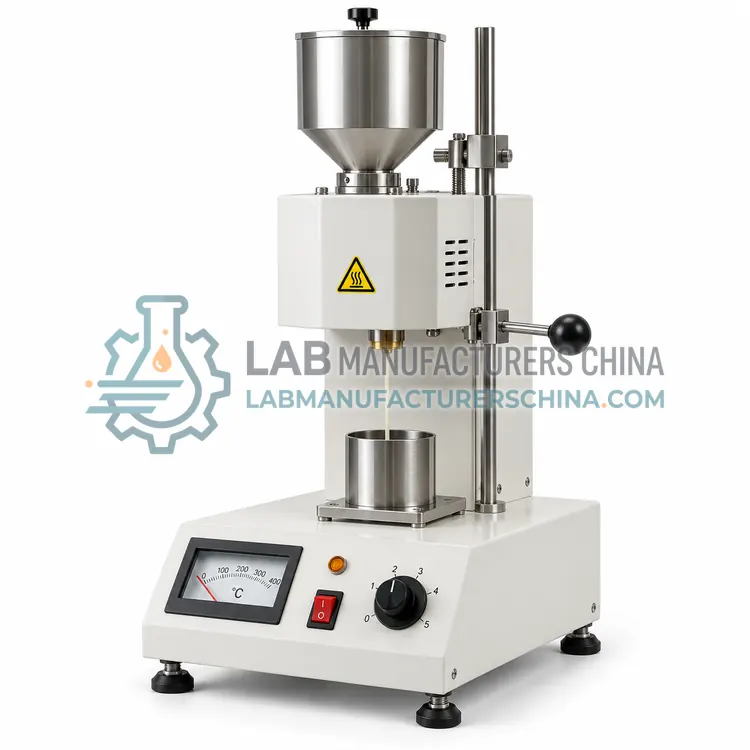
Melt Flow Analyzer for Filled and Reinforced Plastics
填充与增强塑料熔体流动分析仪
- SKU MFA-0005
- Melt Flow Analysis
- CE (to be confirmed)
- ISO 9001 manufacturing (to be confirmed)
Price on request — FOB / CIF quoted per order
Prices depend on configuration, quantity and destination port.
Key specifications
| Die material | Hardened tool steel or tungsten carbide |
|---|---|
| Temperature range | 50–400 °C |
| Load weights | 2.16 / 5 / 10 / 21.6 kg |
| Die options | Ø 2.095 mm standard, larger on request |
| Barrel liner | Wear-resistant alloy, replaceable |
| Temperature accuracy | ±0.2 °C |
Request a quote Download brochure · to be provided
By Lab Manufacturers China Technical TeamLast reviewed Standards: ISO 1133-1, ASTM D1238, ASTM D3364
What is the Melt Flow Analyzer for Filled and Reinforced Plastics?
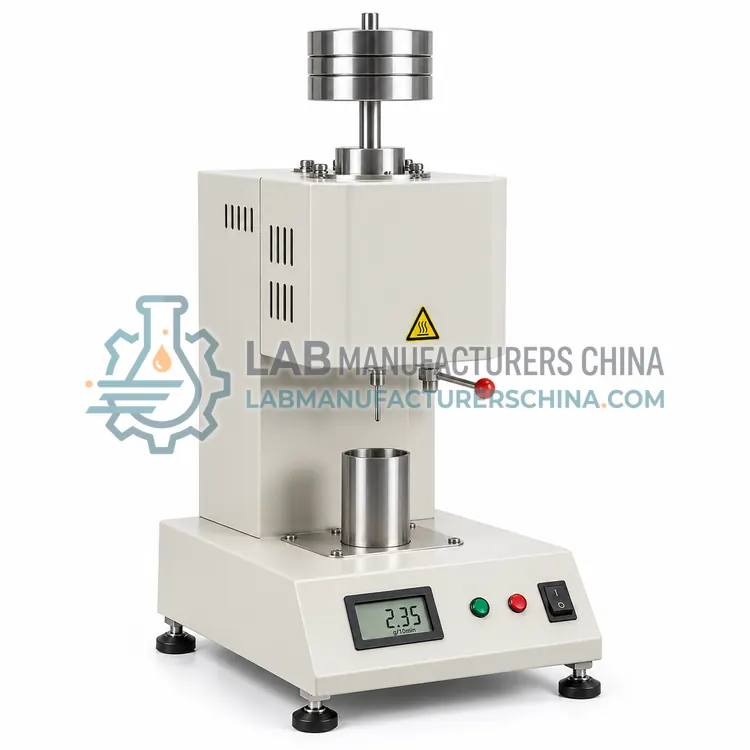
An analyzer configured for filled and reinforced plastics uses abrasion-resistant dies and barrels and a temperature range suited to stiff, highly loaded compounds. It measures flow behaviour of materials that would damage standard hardware or block a die.
Overview
Glass fibre, mineral fillers and flame-retardant packages raise viscosity and abrade the die land, so a dedicated configuration uses hardened or carbide dies, a wear-resistant barrel liner and often a larger die diameter to reduce blockage. Higher loads are frequently required to move such melts within a reasonable time, and the temperature range must reach the processing temperature of engineering grades. Repeatability is inherently poorer than for unfilled resin because filler particles disturb flow and may orient near the die wall, so the method should fix the sample mass, load and condition and report filler content with every result. Where the purpose is quality control rather than fundamental characterisation, the trend of successive lots is often more informative than the absolute value.
How does it work?
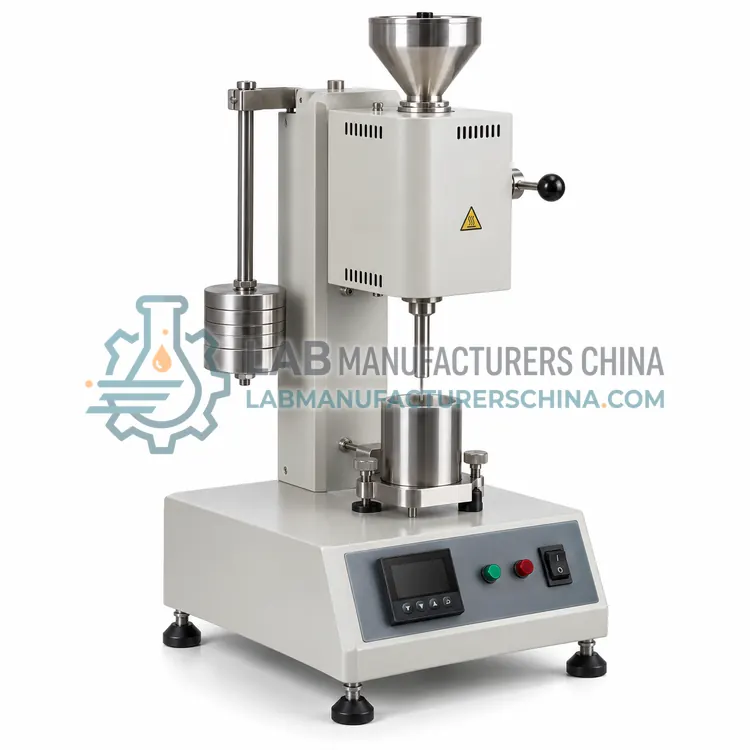
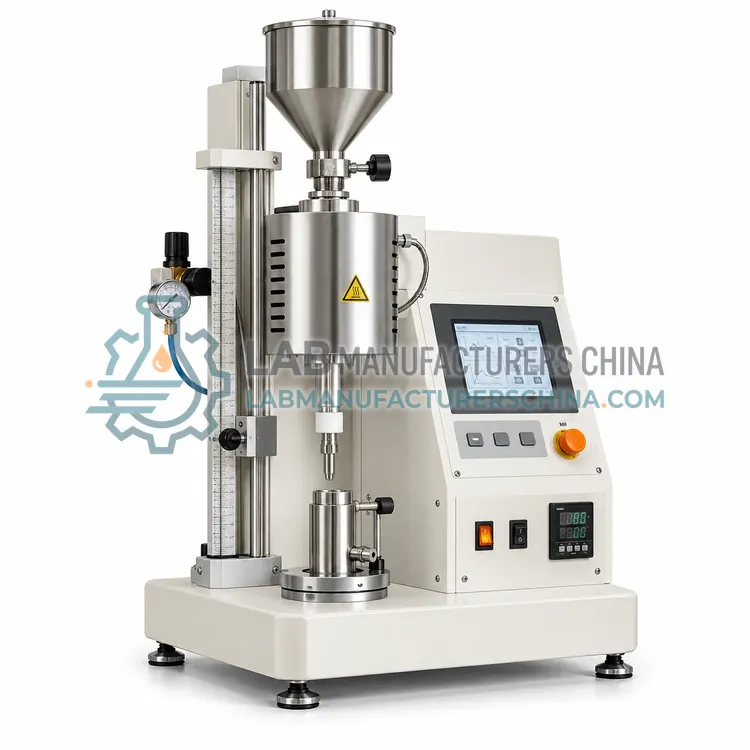
The method heats a plastic sample in a barrel of defined bore, compacts it with a piston and extrudes it through a die of defined diameter and length under a controlled load. Mass-flow rate is obtained by weighing extrudate cut over a known time, and volume-flow rate by recording piston displacement with an encoder. Dividing mass flow by volume flow gives melt density at the test temperature, which is a useful check on filler loading and on batch consistency. Temperature, load, die geometry and preheat time are fixed by the standard condition applicable to the plastic, so results from different laboratories are comparable only when the same condition letter is used. Comparative testing, where a reference material is run on the same instrument, is often the most practical way to confirm instrument condition.
What are the key features?
- Hardened or carbide die for abrasive fillers
- Wear-resistant barrel liner
- Extended load set including high loads
- Temperature range to 400 °C
- Larger die options to reduce blockage
- Filler content field in the result record
What are the technical specifications?
A typical melt flow analyzer for filled and reinforced plastics configuration offers die material of Hardened tool steel or tungsten carbide, temperature range of 50–400 °C, load weights of 2.16 / 5 / 10 / 21.6 kg, die options of Ø 2.095 mm standard, larger on request, barrel liner of Wear-resistant alloy, replaceable and temperature accuracy of ±0.2 °C. Values are indicative of the product class; the exact figures for each configuration are confirmed on the quotation and the calibration documents supplied with the instrument.
Which applications is it used for?
The Melt Flow Analyzer for Filled and Reinforced Plastics is used in glass-filled polyamide and polypropylene flow checks, flame-retardant compound lot consistency, mineral-filled pipe and profile compounds and recycled compound with residual filler. Across the wider Melt Flow Analysis class, laboratories also deploy it for lot release of polyethylene and polypropylene grades, verification of recycled plastic melt flow consistency and effect of filler and reinforcement on flow behaviour.
Which standards and certifications apply?
Relevant standards and methods include ISO 1133-1, ASTM D1238, ASTM D3364, GB/T 3682.1, GB/T 3682.2 and IEC 61010-1. Certification candidates for this model are CE and ISO 9001 manufacturing; each is to be confirmed for the specific configuration before shipment, and certificates are supplied only where they have been issued.
Level the instrument and allow full thermal equilibration before the first measurement, then verify barrel temperature with an external probe. Check die bore and length against the standard tolerance and replace worn dies, because an enlarged bore lowers the measured value. Use only dried material for hygroscopic plastics stated in the method, and discard any extrudate containing bubbles or voids. Clean the barrel between materials with purging compound, not with metal tools. Keep weights traceable and record the standard condition, sample mass, preheat time and any melt density value with every result so that a reviewer can reconstruct the test.
How do I select the right Melt Flow Analyzer for Filled and Reinforced Plastics?
Specify this configuration whenever the compound contains more than a few percent of abrasive filler, when flow stalls before the preheat time ends, or when the die blocks repeatedly. Confirm the die material and the barrel liner, and ask for the expected repeatability with your filler loading, since published tolerances usually refer to unfilled resin.
How does it compare with other Melt Flow Analysis variants?
Define the output you need first. For routine lot release, a gravimetric instrument that weighs timed cuts is adequate and easiest to defend against the standard. When results must be traceable in a digital system or the material is difficult to cut, an instrument with piston displacement measurement is preferable. Where throughput dominates, choose a multi-position analyzer or a robotic loading configuration. Add a melt density capability when filler content or batch-to-batch density variation is a quality concern. For filled, reinforced or very high molecular weight plastics, specify the load set and a corrosion- or abrasion-resistant barrel and die, because standard hardware may not reach the required condition or may wear quickly.
Full specifications
| Die material | Hardened tool steel or tungsten carbide |
|---|---|
| Temperature range | 50–400 °C |
| Load weights | 2.16 / 5 / 10 / 21.6 kg |
| Die options | Ø 2.095 mm standard, larger on request |
| Barrel liner | Wear-resistant alloy, replaceable |
| Temperature accuracy | ±0.2 °C |
| Sample mass per test | 4–10 g |
| Expected repeatability | Within 5–8% for glass-filled grades |
| Recommended preheat | 6–8 min for stiff compounds |
| Power supply | 220 V, 50/60 Hz |
Indicative values for this product class. Final specifications are confirmed on the quotation and in the calibration documents supplied with the instrument.
Applications
- Glass-filled polyamide and polypropylene flow checks
- Flame-retardant compound lot consistency
- Mineral-filled pipe and profile compounds
- Recycled compound with residual filler
Key features
- Hardened or carbide die for abrasive fillers
- Wear-resistant barrel liner
- Extended load set including high loads
- Temperature range to 400 °C
- Larger die options to reduce blockage
- Filler content field in the result record
Frequently asked questions about Melt Flow Analyzer for Filled and Reinforced Plastics
Filler particles create local variations in viscosity, may concentrate near the die wall and can bridge the die opening, so successive measurements differ more than for unfilled resin. Longer preheat and higher loads improve flow stability, and results should always be reported with the filler content and a note that they are comparative rather than absolute.
Tungsten carbide dies resist abrasion far better than hardened tool steel, though they cost more and are more brittle if mishandled. Hardened steel dies with the correct hardness are usually adequate for occasional use, and the die land should be measured periodically because wear increases the calculated flow rate.
Yes. Melt flow rate falls as filler loading rises, so two lots of the same nominal grade can differ simply because of filler content. Reporting the ash or filler value alongside the flow rate lets a reviewer separate formulation effects from molecular effects, which is essential when investigating a complaint.
It indicates how easily the grade flows at the test condition, which correlates with processability: a high value suits thin-wall or complex mouldings, a low value suits extrusion of thick sections and gives better melt strength. Because it is sensitive to molecular weight and filler content, it also serves as a lot-to-lot consistency check.
Melt density is obtained by dividing the mass-flow rate by the volume-flow rate, both measured at the same condition. It changes if filler loading, polymer grade or additive content changes, so it provides an independent check that a flow-rate difference is caused by molecular structure rather than by a formulation change.
Grind or use a representative portion of the compound, dry it if the base resin requires it, and expect poorer repeatability because filler particles disturb flow and may block the die. Report the filler content with the result and consider abrasive-resistant dies, since fillers such as glass fibre wear the die land and change the geometry.