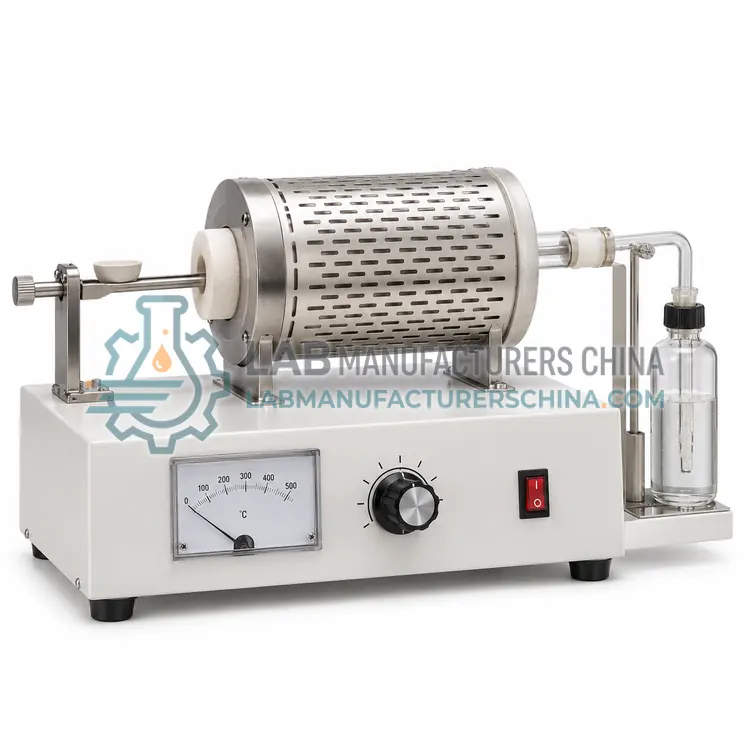
Infrared Sulfur Analyzer for Coal and Coke
煤和焦炭红外测硫仪
- SKU ELM-0005
- Elemental Analyzers
- CE (to be confirmed)
- ISO 9001 manufacturing (to be confirmed)
- RoHS (to be confirmed)
Price on request — FOB / CIF quoted per order
Prices depend on configuration, quantity and destination port.
Key specifications
| Sulfur range | 0.01–10% (m/m) |
|---|---|
| Sample mass | 0.1–1.0 g |
| Furnace temperature | 1150–1350 °C |
| Detector | Non-dispersive infrared (SO2) |
| Analysis time | 3–5 min |
| Repeatability | ≤ 0.02% absolute (below 1% S) |
Request a quote Download brochure · to be provided
By Lab Manufacturers China Technical TeamLast reviewed Standards: ASTM E1019, ASTM E1409, ASTM D5373
What is the Infrared Sulfur Analyzer for Coal and Coke?
An infrared sulfur analyzer burns a gram-scale coal, coke or solid fuel sample at 1150–1350 °C in oxygen and measures the SO2 formed by non-dispersive infrared absorption. It gives total sulfur in coal, coke and biomass within minutes for trading, blending and emission-control decisions.
Overview
A sample of 0.1–1 g is weighed into a ceramic boat, covered with a combustion aid such as vanadium pentoxide where needed, and pushed into a tube furnace at 1250–1350 °C with oxygen flow. Combustion gases pass through dust removal and dehydration to an infrared cell measuring SO2 absorption near 7.3 µm. Total sulfur is computed from integrated signal and sample mass against calibration with coal standards of known sulfur. The dedicated design handles high-ash solid fuels more robustly than chemical methods, and measurement time is 3–5 minutes against hours for Eschka gravimetry. Results are reported in percent, with options to report on air-dried, dry or dry-ash-free basis when moisture is entered. Calibrations are routinely checked with certified coal standards.
How does it work?
Elemental analyzers convert the element of interest into a simple gas at high temperature and then measure that gas. In combustion analysis, a sample burns in oxygen at 900–1350 °C, converting carbon to CO2, hydrogen to H2O, sulfur to SO2 and nitrogen to N2 or NOx. Gases are separated by chromatographic column or selective traps and detected by non-dispersive infrared cells, thermal conductivity detectors or chemiluminescence. Inert gas fusion heats a sample in a graphite crucible under helium to release oxygen as CO, nitrogen as N2 and hydrogen as H2, again measured by infrared and thermal conductivity. Induction furnaces heat metals and ores with accelerators such as tungsten and tin. Calibration uses certified standards of known composition.
What are the key features?
- Tube furnace operating up to 1350 °C for complete sulfur release from coal ash
- Non-dispersive infrared SO2 cell with temperature-stabilized optics
- Automatic boat loader for sequential batches of solid fuels
- Dust trap and dehydration unit protecting the infrared cell
- Result reporting on air-dried, dry and dry-ash-free bases
- Calibration storage for coal, coke and biomass matrices
What are the technical specifications?
A typical infrared sulfur analyzer for coal and coke configuration offers sulfur range of 0.01–10% (m/m), sample mass of 0.1–1.0 g, furnace temperature of 1150–1350 °C, detector of Non-dispersive infrared (SO2), analysis time of 3–5 min and repeatability of ≤ 0.02% absolute (below 1% S). Values are indicative of the product class; the exact figures for each configuration are confirmed on the quotation and the calibration documents supplied with the instrument.
Which applications is it used for?
The Infrared Sulfur Analyzer for Coal and Coke is used in total sulfur in thermal and coking coal, sulfur in coke and petroleum coke, sulfur in biomass and solid recovered fuel, coal blending and delivery acceptance and fuel compliance for power plants. Across the wider Elemental Analyzers class, laboratories also deploy it for carbon and sulfur in steel and ores, oxygen, nitrogen and hydrogen in metals and alloys and ultimate analysis of coal and coke.
Which standards and certifications apply?
Relevant standards and methods include ASTM E1019, ASTM E1409, ASTM D5373, ASTM D5453, ASTM D4239, ISO 15350, ISO 10694 and IEC 61010-1. Certification candidates for this model are CE, ISO 9001 manufacturing and RoHS; each is to be confirmed for the specific configuration before shipment, and certificates are supplied only where they have been issued.
Elemental analyzers need clean, dry, high-purity gases, typically oxygen and helium or argon at 99.995% or better, with regulators and moisture traps. Condition new combustion tubes, catalysts and reagents according to the manual, and replace them on a usage schedule. Run blanks and conditioning samples at start-up, then calibrate with certified standards that match the expected concentration range, such as acetanilide for CHN or steel standards for C and S. Control dust by cleaning the furnace and filters frequently, especially for ore and coke samples. Check for gas leaks regularly, weigh samples on a balance with suitable readability, and keep crucibles pre-ignited and free of contamination.
How do I select the right Infrared Sulfur Analyzer for Coal and Coke?
Select this variant when total sulfur in coal, coke or solid fuel is the main parameter and speed matters. Choose a CHNS analyzer for a full ultimate analysis. In an RFQ, state sulfur range, sample types, daily samples, autoloader need, oxygen supply and standards such as ASTM D4239 or ISO 351.
How does it compare with other Elemental Analyzers variants?
Select by element set and sample form. Carbon and sulfur in steel, ores, cement and ceramics point to a high-frequency induction furnace with infrared detection. Oxygen, nitrogen and hydrogen in metals call for an inert gas fusion analyzer. Organic samples requiring C, H, N, S and possibly O suit a CHNS/O dynamic-flash combustion analyzer. Sulfur or nitrogen at mg/kg levels in liquid fuels suit UV-fluorescence or chemiluminescence analyzers. Check measuring range, since percent-level and ppm-level analyses need different detector ranges. Consider sample throughput, autosampler capacity, consumables such as crucibles, anhydrone and catalysts, and the standard methods to be met, such as ASTM E1019 or ASTM D5453.
Full specifications
| Sulfur range | 0.01–10% (m/m) |
|---|---|
| Sample mass | 0.1–1.0 g |
| Furnace temperature | 1150–1350 °C |
| Detector | Non-dispersive infrared (SO2) |
| Analysis time | 3–5 min |
| Repeatability | ≤ 0.02% absolute (below 1% S) |
| Resolution | 0.001% S |
| Oxygen consumption | ≈ 1–1.5 L/min |
| Boat capacity | Up to 20–40 boats (autoloader) |
| Power supply | 220 V AC, 50 Hz, ≤ 3 kW |
Indicative values for this product class. Final specifications are confirmed on the quotation and in the calibration documents supplied with the instrument.
Applications
- Total sulfur in thermal and coking coal
- Sulfur in coke and petroleum coke
- Sulfur in biomass and solid recovered fuel
- Coal blending and delivery acceptance
- Fuel compliance for power plants
Key features
- Tube furnace operating up to 1350 °C for complete sulfur release from coal ash
- Non-dispersive infrared SO2 cell with temperature-stabilized optics
- Automatic boat loader for sequential batches of solid fuels
- Dust trap and dehydration unit protecting the infrared cell
- Result reporting on air-dried, dry and dry-ash-free bases
- Calibration storage for coal, coke and biomass matrices
Frequently asked questions about Infrared Sulfur Analyzer for Coal and Coke
Some sulfur in coal stays in ash as sulfates at low temperatures. Operating at 1350 °C decomposes these sulfates so all sulfur is released as SO2, and a combustion aid may be used to ensure recovery, as specified in ASTM D4239.
The analyzer measures sulfur on the sample as analyzed, typically air-dried. Using moisture and ash results entered in the software, it converts to as-received, dry and dry-ash-free bases with standard formulas such as those in ASTM D3180.
Certified coal reference materials with assigned sulfur content are preferred, covering low, medium and high sulfur. Sulfanilamide or other pure compounds may be used for checks, but matrix-matched coal standards are better for acceptance testing.
A carbon-sulfur analyzer uses an induction furnace and infrared cells to measure C and S in metals, ores and inorganic solids at ppm to percent levels. A CHNS analyzer uses flash combustion and gas separation for organic samples, reporting C, H, N and S together.
Combustion analyzers need high-purity oxygen for combustion and either helium or argon as carrier gas, plus compressed air for pneumatics in some models. Gas purity of 99.995% or better is typical, and moisture and CO2 traps protect detectors.
Replacement depends on sample load and type. Typical schedules are after 300–1000 combustions for tubes and reagents in CHNS systems, while induction furnace dust traps and filters are cleaned daily. Follow the maker's indicators and check recovery of standards.
Related models
UV-Fluorescence Total Sulfur and Chemiluminescence Nitrogen Analyzer
紫外荧光总硫与化学发光总氮分析仪
- CE (to be confirmed)
- +2