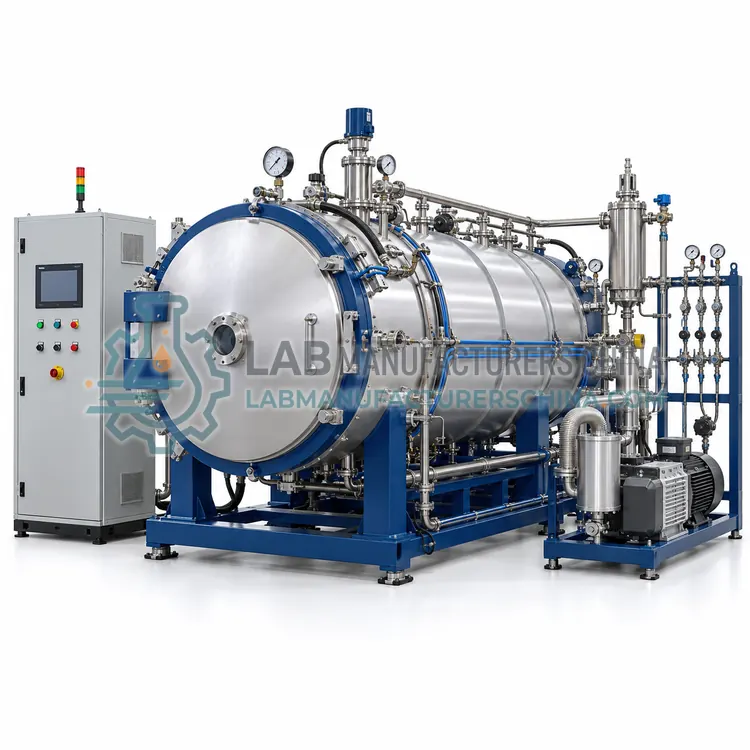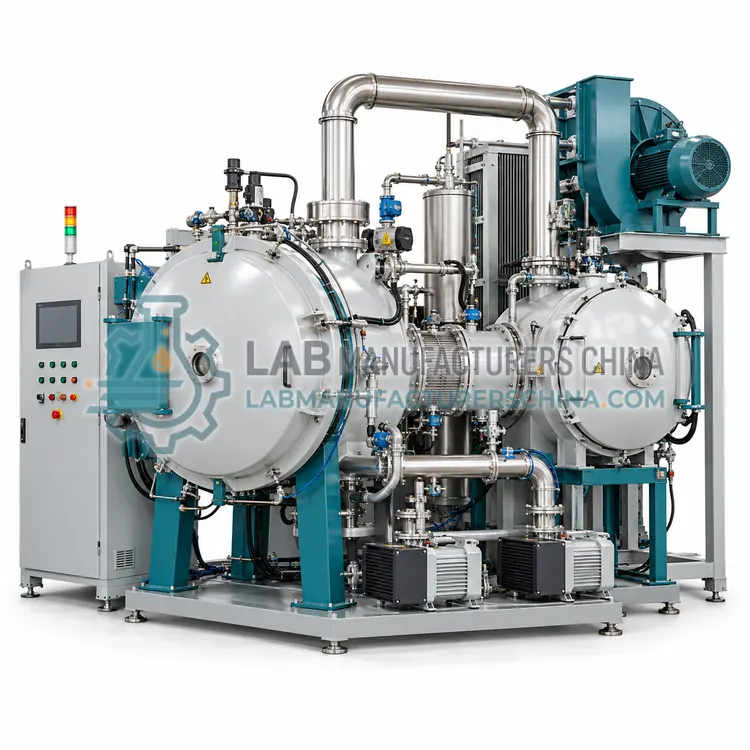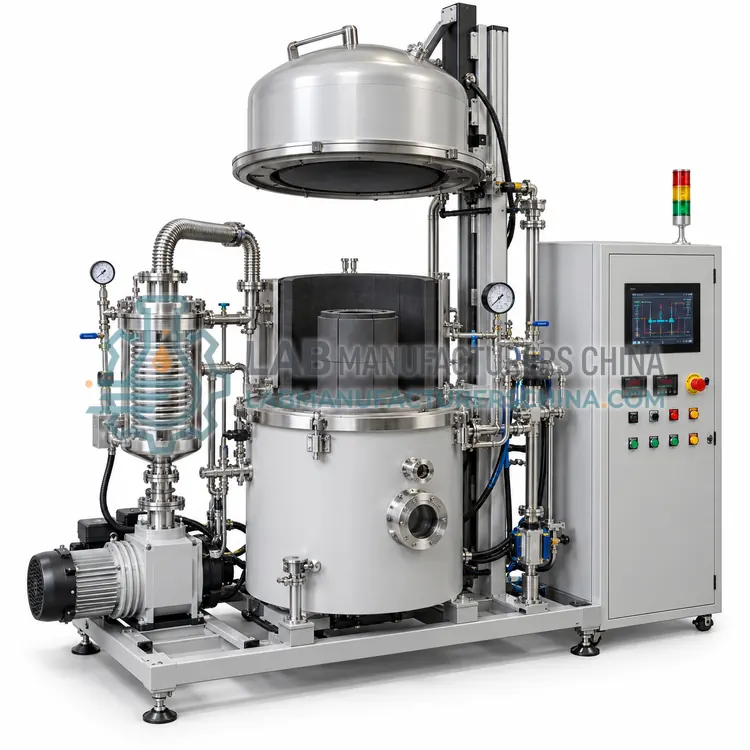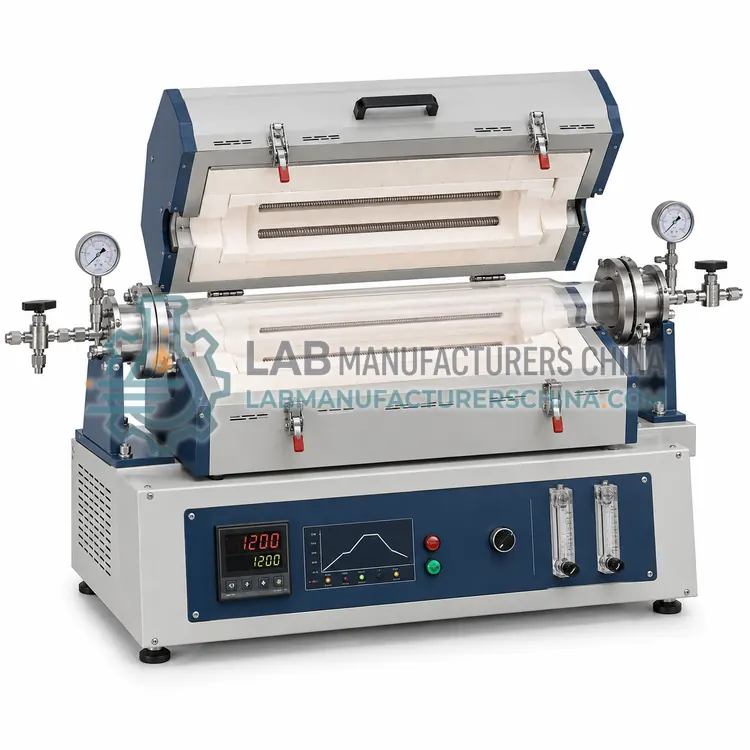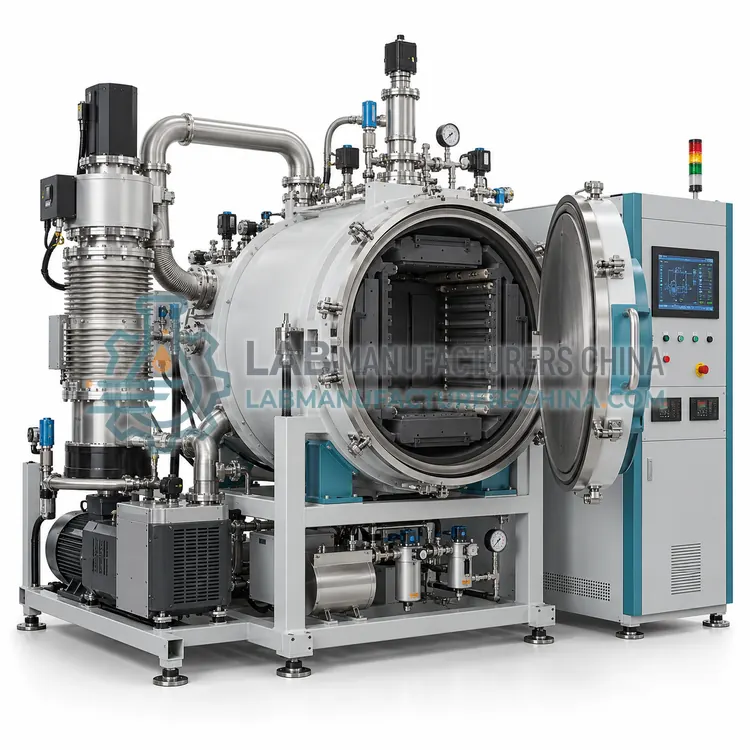
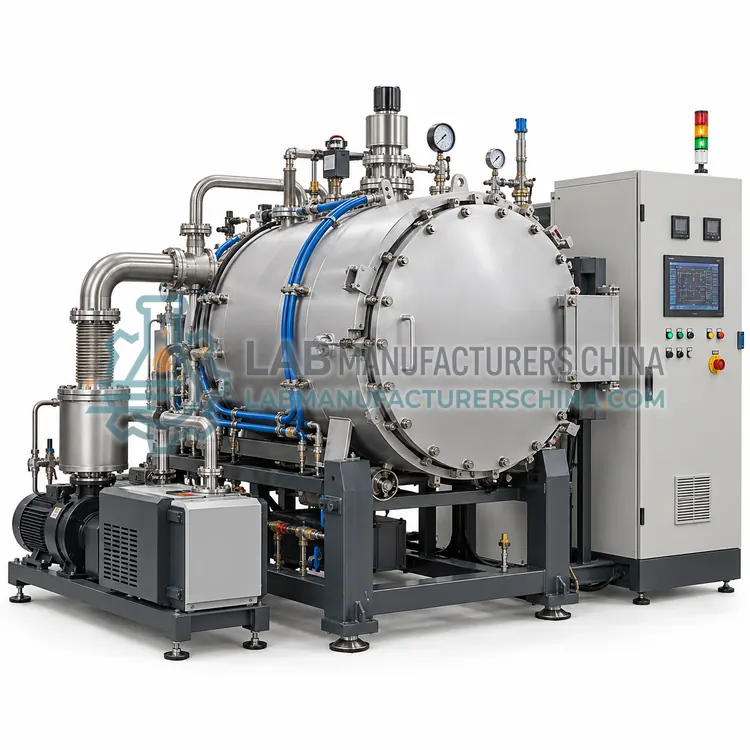
Vacuum Heat Treatment Furnace
真空热处理炉
- SKU VAF-0001
- Vacuum Furnaces
- CE (to be confirmed)
- ISO 9001 manufacturing (to be confirmed)
- RoHS (to be confirmed)
Price on request — FOB / CIF quoted per order
Prices depend on configuration, quantity and destination port.
Key specifications
| Hot zone size | 300×300×450 to 600×600×900 mm |
|---|---|
| Maximum temperature | 1200–1350 C |
| Working vacuum | 1–100 Pa |
| Hot zone material | Graphite felt or rigid graphite |
| Heating elements | Graphite or molybdenum |
| Quench pressure | 2–6 bar inert gas |
Request a quote Download brochure · to be provided
By Lab Manufacturers China Technical TeamLast reviewed Standards: IEC 61010-1, IEC 60519-1, AMS 2750
What is the Vacuum Heat Treatment Furnace?
A vacuum heat treatment furnace hardens, tempers, anneals and solution-treats metals without oxidation, preserving bright surfaces. It is chosen when clean, scale-free results and repeatable harden and temper cycles are required for valuable components.
What is the Vacuum Heat Treatment Furnace?
A vacuum heat treatment furnace hardens, tempers, anneals and solution-treats metals without oxidation, preserving bright surfaces. It is chosen when clean, scale-free results and repeatable harden and temper cycles are required for valuable components.
Overview
This furnace applies vacuum processing to general heat treatment, with a graphite or molybdenum hot zone and a programmable controller for ramp, soak and cooling steps. Working temperature reaches 1200 to 1350 C depending on elements, and vacuum of 1 to 100 Pa is usual, with inert-gas partial pressure to control element evaporation. Because radiation heats the load, parts are fixtured with clear line of sight to the elements and spaced for uniform heating. Gas quenching and backfill cooling give controlled rates. Hot-zone size fits batch loads up to hundreds of kilograms. It produces bright, decarburization-free surfaces that often need no further cleaning, which suits tooling, bearings and aerospace components.
How does it work?
A vacuum furnace removes the chamber atmosphere with a pump system, typically a rotary-vane or dry pump backed by a roots or diffusion pump, down to rough or high vacuum. With oxygen and nitrogen largely removed, heated materials resist oxidation and outgassing, and volatile species leave the surface. Heating comes from graphite, molybdenum or tungsten elements, or from induction coils, arranged around a hot zone insulated with graphite felt or rigid insulation. Radiation is the dominant heat-transfer mode, so loads must have a clear line of sight to the elements. Type C, N or K thermocouples or optical pyrometers measure temperature, and a programmable controller follows the cycle. Gas quenching or backfill ports allow rapid, controlled cooling after the hold.
What are the key features?
- Graphite or molybdenum hot zone
- Programmable ramp, soak and cooling cycles
- Partial-pressure control with inert gas
- Gas quenching and backfill cooling
- Bright, decarburization-free surfaces
- Batch loads up to several hundred kilograms
What are the technical specifications?
A typical vacuum heat treatment furnace configuration offers hot zone size of 300×300×450 to 600×600×900 mm, maximum temperature of 1200–1350 C, working vacuum of 1–100 Pa, hot zone material of Graphite felt or rigid graphite, heating elements of Graphite or molybdenum and quench pressure of 2–6 bar inert gas. Values are indicative of the product class; the exact figures for each configuration are confirmed on the quotation and the calibration documents supplied with the instrument.
Which applications is it used for?
The Vacuum Heat Treatment Furnace is used in tool and die steel hardening, bearing and gear heat treatment, aerospace component processing and solution treatment of stainless steels. Across the wider Vacuum Furnaces class, laboratories also deploy it for vacuum heat treatment of tool steels, brazing of aerospace components and sintering of hard metals and ceramics.
Which standards and certifications apply?
Relevant standards and methods include IEC 61010-1, IEC 60519-1, AMS 2750, AMS 2769 and ISO 9001. Certification candidates for this model are CE, ISO 9001 manufacturing and RoHS; each is to be confirmed for the specific configuration before shipment, and certificates are supplied only where they have been issued.
Install on a level, rigid floor with services for power, cooling water, compressed gas and compressed air, and provide ventilation for any exhaust and gas relief. Keep cooling water clean and temperature-controlled to protect seals and pumps. Check the furnace for leaks after every opening and before critical runs, since even small leaks oxidize surfaces and spoil vacuum. Clean hot-zone insulation and elements when contamination appears, and replace graphite parts before erosion becomes severe. Maintain pump service records, verify pyrometry and uniformity surveys on schedule, and never bypass over-temperature, water-flow or door interlocks.
How do I select the right Vacuum Heat Treatment Furnace?
Select the vacuum heat treatment furnace for scale-free hardening, annealing and tempering of high-value components. Atmosphere furnaces are cheaper where surface quality is less critical. In the RFQ, specify hot zone size, load mass, maximum temperature, quench pressure, pumping system and any pyrometry or uniformity requirements.
How does it compare with other Vacuum Furnaces variants?
Choose a vacuum furnace when oxidation, contamination or outgassing rules out atmosphere processing, or when surface quality and purity matter. Define the process first: heat treatment, sintering, brazing or degassing, since each sets the temperature, vacuum level and cooling method. Set the hot zone size from load dimensions and weight, and confirm the maximum temperature against the element and insulation materials. Decide on cooling, choosing between gas quenching, backfill with inert gas or slow cooling. Specify pumping stages, leak rate, partial-pressure control and safety features. For regulated heat treatment, require pyrometry compliance and uniformity surveys, and confirm three-phase power and cooling-water supply.
Full specifications
| Hot zone size | 300×300×450 to 600×600×900 mm |
|---|---|
| Maximum temperature | 1200–1350 C |
| Working vacuum | 1–100 Pa |
| Hot zone material | Graphite felt or rigid graphite |
| Heating elements | Graphite or molybdenum |
| Quench pressure | 2–6 bar inert gas |
| Temperature uniformity | ±5–10 C |
| Pumping system | Rotary-vane plus roots |
| Heating power | 30–150 kW |
| Power supply | 380 V, 3-phase, 50/60 Hz |
Indicative values for this product class. Final specifications are confirmed on the quotation and in the calibration documents supplied with the instrument.
Applications
- Tool and die steel hardening
- Bearing and gear heat treatment
- Aerospace component processing
- Solution treatment of stainless steels
Key features
- Graphite or molybdenum hot zone
- Programmable ramp, soak and cooling cycles
- Partial-pressure control with inert gas
- Gas quenching and backfill cooling
- Bright, decarburization-free surfaces
- Batch loads up to several hundred kilograms
Frequently asked questions about Vacuum Heat Treatment Furnace
It prevents oxidation and decarburization, leaving bright surfaces that often need no cleaning, and it removes dissolved gases. Cycles are highly repeatable and free of salt or atmosphere residues, which suits critical tooling, aerospace and medical components.
At high temperature and deep vacuum, alloying elements and graphite elements can evaporate and contaminate the load. Introducing a small amount of inert gas raises pressure enough to suppress evaporation while still preventing oxidation.
Most furnaces use argon or nitrogen at 2 to 6 bar or higher for gas quenching, with the pressure and blower speed setting the cooling rate. Some alloys need only slow cooling or backfill, and the required rate follows the material's hardenability.
It heat-treats, sinters, brazes and degasses metals and ceramics in a sealed chamber at low pressure, avoiding oxidation and contamination. It is used for tool steels, aerospace components, hard metals and reactive metals where clean surfaces and controlled atmospheres are essential.
Rough vacuum of about 1 to 100 Pa suits many heat treatments, while sintering and brazing may use 0.001 to 0.1 Pa. Partial-pressure control with inert gas is often used to limit element evaporation and alloying-element loss at high temperature.
After the hold, inert gas such as argon or nitrogen is admitted and circulated by a high-speed blower through a heat exchanger, cooling the load at a controlled rate. The available quenching pressure, often 2 to 10 bar, sets the maximum cooling rate.
Related models