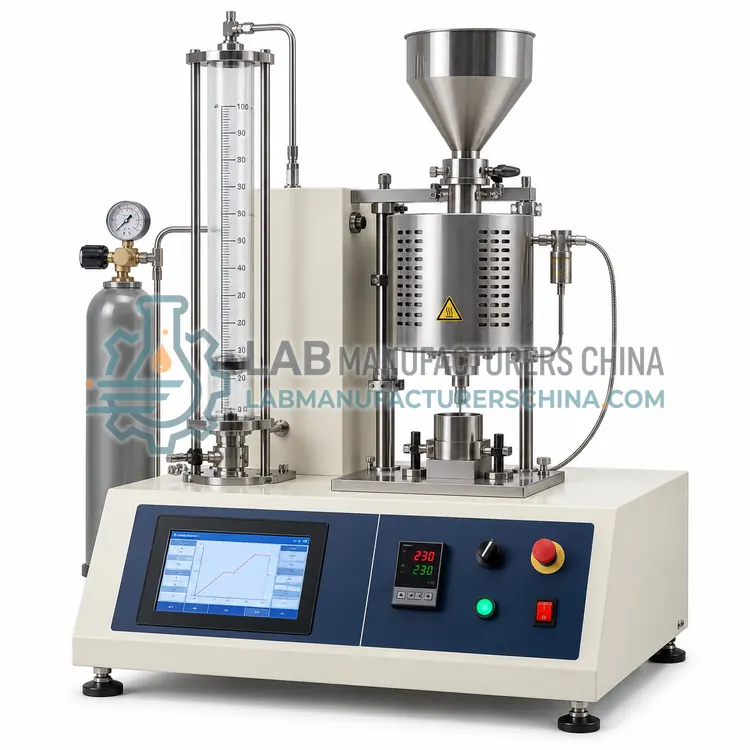
High-Pressure Capillary Rheometer for Polymer Extrusion
聚合物挤出用高压毛细管流变仪
- SKU RHE-0003
- Rheometers
- CE (to be confirmed)
- ISO 9001 manufacturing (to be confirmed)
- IEC 61010-1 safety compliance (to be confirmed)
Price on request — FOB / CIF quoted per order
Prices depend on configuration, quantity and destination port.
Key specifications
| Maximum pressure | Up to 2000 bar |
|---|---|
| Temperature range | Ambient to 450 °C |
| Temperature accuracy | ±0.5 °C |
| Barrel diameter | 9.55 / 12 / 15 mm |
| Piston speed | 0.0005–20 mm/s |
| Shear rate range | 1–2 × 10⁶ s⁻¹ |
Request a quote Download brochure · to be provided
By Lab Manufacturers China Technical TeamLast reviewed Standards: ISO 3219, ISO 11443, ISO 6721-10
What is the High-Pressure Capillary Rheometer for Polymer Extrusion?
A high-pressure capillary rheometer operates to about 2000 bar and covers the very high shear rates found in extrusion dies, spinnerets and thin-wall moulding. It is specified when standard instruments reach their pressure limit before the process shear rate is covered.
Overview
Increasing pressure capability extends the measurable shear rate range, because the same die produces a higher pressure drop at higher throughput. A high-pressure instrument therefore uses a reinforced barrel, a thicker-walled die holder, burst-rated pressure transducers and a rigid frame that limits deflection under load. It reaches apparent shear rates beyond 10⁶ s⁻¹, which corresponds to flow in a thin extrusion die land, a fibre spinning capillary or a thin-wall injection cavity. These conditions also make it possible to observe melt fracture, sharkskin and slip, and to quantify the critical shear stress at which surface defects appear. Materials handled include highly filled halogen-free flame-retardant compounds, mineral-filled grades and ultra-high-molecular-weight polyethylene, whose viscosity would exceed the pressure limit of a standard instrument.
How does it work?
A rheometer applies a controlled deformation to a polymer sample and measures the resulting force or torque. Rotational instruments use parallel plates, cones or concentric cylinders and can work in steady shear, giving shear viscosity against shear rate, or in oscillation, giving storage and loss moduli against frequency. Capillary instruments force melt through a die of known diameter and length at a controlled piston speed, measuring pressure to calculate apparent shear viscosity at shear rates that reach those of real extrusion. Torque rheometers mix material in a heated chamber and record the torque needed to turn the rotors, which tracks gelation, fusion and degradation in a compounding context. The choice depends on the shear rate range, the sample form and whether elasticity or only viscosity is required.
What are the key features?
- Maximum working pressure up to 2000 bar
- Reinforced barrel and die holder for high pressure
- Burst-rated pressure transducers
- Shear rates above 10⁶ s⁻¹
- Critical shear stress and melt fracture detection
- Dies in hardened and corrosion-resistant alloys
What are the technical specifications?
A typical high-pressure capillary rheometer for polymer extrusion configuration offers maximum pressure of Up to 2000 bar, temperature range of Ambient to 450 °C, temperature accuracy of ±0.5 °C, barrel diameter of 9.55 / 12 / 15 mm, piston speed of 0.0005–20 mm/s and shear rate range of 1–2 × 10⁶ s⁻¹. Values are indicative of the product class; the exact figures for each configuration are confirmed on the quotation and the calibration documents supplied with the instrument.
Which applications is it used for?
The High-Pressure Capillary Rheometer for Polymer Extrusion is used in thin-wall injection moulding compound evaluation, fibre spinning and film die process design, highly filled and flame-retardant compound testing and ultra-high-molecular-weight polyethylene processing. Across the wider Rheometers class, laboratories also deploy it for molecular weight and molecular weight distribution comparison, processing behaviour prediction for extrusion and moulding and filler and additive effect on melt viscosity.
Which standards and certifications apply?
Relevant standards and methods include ISO 3219, ISO 11443, ISO 6721-10, ASTM D3835, ASTM D4440, ASTM D2538 and IEC 61010-1. Certification candidates for this model are CE, ISO 9001 manufacturing and IEC 61010-1 safety compliance; each is to be confirmed for the specific configuration before shipment, and certificates are supplied only where they have been issued.
Sample preparation dominates repeatability: dry hygroscopic polymers, compression-mould discs of defined thickness for rotational testing, and ensure filled samples are homogeneous. Set the gap and check it with a zero-gap routine before each series, because a small gap error changes the calculated viscosity. In capillary work, verify piston speed and pressure transducer calibration, and apply the Bagley and Rabinowitsch corrections when true viscosity is required. Purge the oven with nitrogen for high-temperature or oxidation-sensitive polymers. Clean dies and plates thoroughly, since degraded residue changes the surface and the measured torque, and record temperature, geometry and gap with every result.
How do I select the right High-Pressure Capillary Rheometer for Polymer Extrusion?
Specify a high-pressure instrument when the process shear rate cannot be reached because the standard pressure limit is hit first, which typically happens with filled compounds, very high molecular weight grades or very small dies. Confirm the die diameter set and the pressure transducer range you need, since accuracy is quoted against full scale. Ask about barrel heating uniformity at the top of the pressure range.
How does it compare with other Rheometers variants?
Match the instrument to the shear rate range that governs your process. Rotational rheometers cover low shear rates and are the only option when viscoelastic data, yield stress or normal force are required, making them suitable for molecular weight comparisons and additive studies. Capillary rheometers reach the high shear rates of extrusion and injection moulding and are more tolerant of filled and highly viscous materials. Torque rheometers are used when the question concerns compounding behaviour, gelation or thermal stability under shear rather than a fundamental viscosity value. Inline instruments are selected for continuous process monitoring and never replace laboratory characterisation, because they see only one fixed measurement point.
Full specifications
| Maximum pressure | Up to 2000 bar |
|---|---|
| Temperature range | Ambient to 450 °C |
| Temperature accuracy | ±0.5 °C |
| Barrel diameter | 9.55 / 12 / 15 mm |
| Piston speed | 0.0005–20 mm/s |
| Shear rate range | 1–2 × 10⁶ s⁻¹ |
| Die diameters | 0.3–2.0 mm |
| Pressure transducer accuracy | ±0.25% of full scale |
| Sample mass per test | 10–60 g |
| Power supply | 380 V, 50 Hz, three-phase |
Indicative values for this product class. Final specifications are confirmed on the quotation and in the calibration documents supplied with the instrument.
Applications
- Thin-wall injection moulding compound evaluation
- Fibre spinning and film die process design
- Highly filled and flame-retardant compound testing
- Ultra-high-molecular-weight polyethylene processing
Key features
- Maximum working pressure up to 2000 bar
- Reinforced barrel and die holder for high pressure
- Burst-rated pressure transducers
- Shear rates above 10⁶ s⁻¹
- Critical shear stress and melt fracture detection
- Dies in hardened and corrosion-resistant alloys
Frequently asked questions about High-Pressure Capillary Rheometer for Polymer Extrusion
Bulk flow in an extruder screw typically involves 10 to 1000 s⁻¹, while the die land and thin cavities can exceed 10⁴ to 10⁶ s⁻¹. Capillary rheometers are therefore run over a wide range, and the upper part of the curve, only accessible with high-pressure instruments, is the region that controls surface defects.
Transducers are calibrated against a dead-weight tester or a reference gauge across their range and are quoted as a percentage of full scale. Accuracy therefore improves when a transducer matched to the working pressure is installed, rather than relying on a very high range instrument for low-pressure measurements. Routine zero and span checks are essential.
Not if the instrument is used within its ratings and abrasive fillers are paired with hardened or carbide dies. Wear does occur on the die land and barrel bore over time, and both should be measured periodically against the original dimensions, because dimensional change affects the calculated shear stress even when the instrument still functions normally.
A rotational rheometer measures viscosity in steady or oscillatory shear at low shear rates, where the material response is dominated by molecular relaxation. A capillary rheometer measures at high shear rates that match extrusion and injection moulding. The two techniques overlap in a mid-range and should agree after corrections, but each covers a shear rate window the other cannot reach.
Viscosity is calculated from measured torque, angular velocity and the gap between the geometries, so an error in gap propagates directly into the result. Compression of the sample and thermal expansion change the effective gap, which is why a zero-gap routine and a constant sample thickness are used before each series.
They can, but filler particles may slip at the plate surface, settle, or bridge the gap, so the measured viscosity can be too low. Practical measures are to use serrated or roughened plates, larger gaps, and lower filler loadings where possible, and to compare results only between samples of the same filler content and particle size.