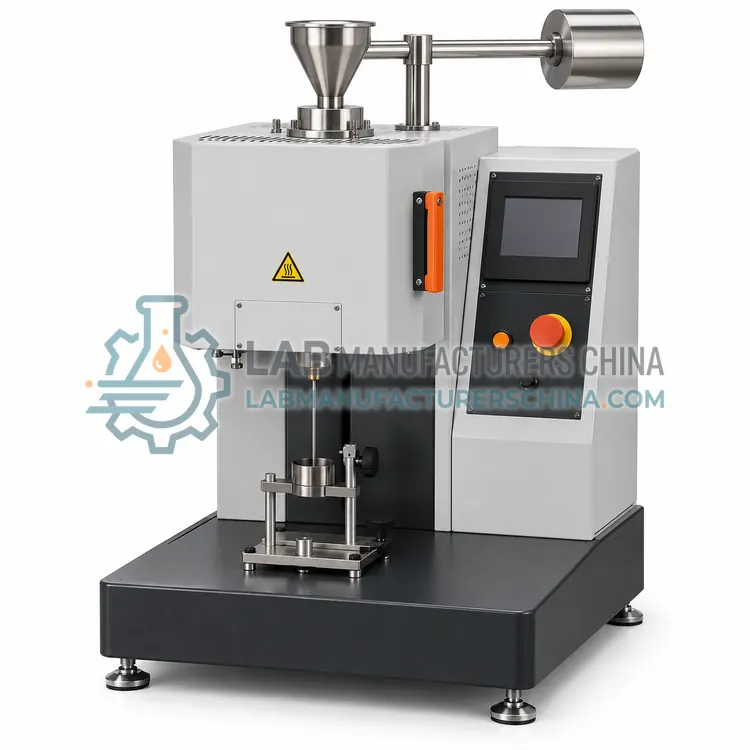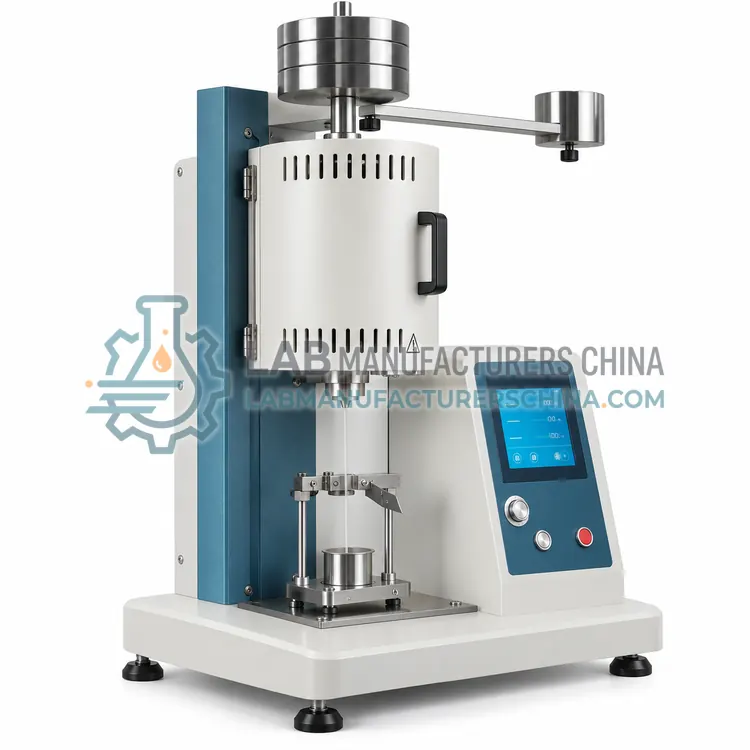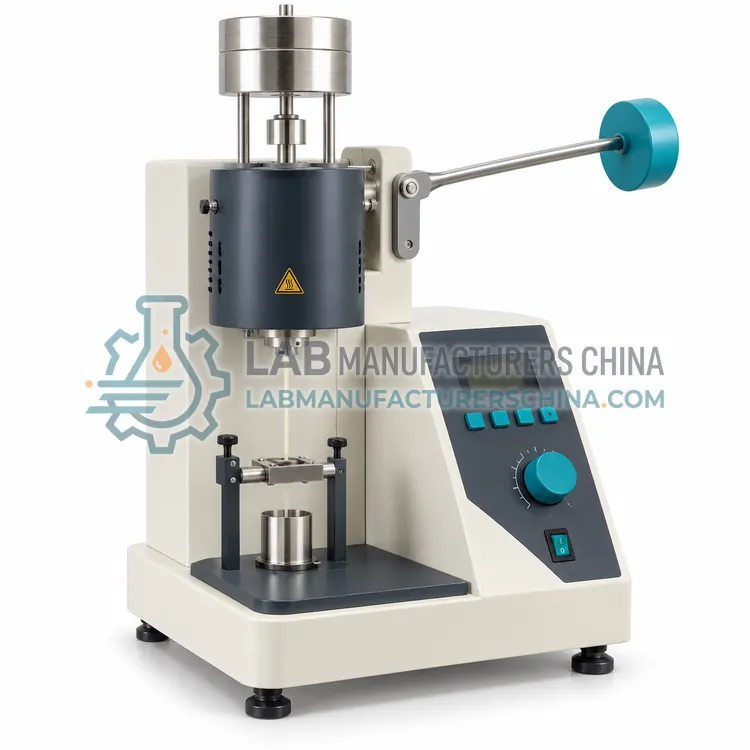
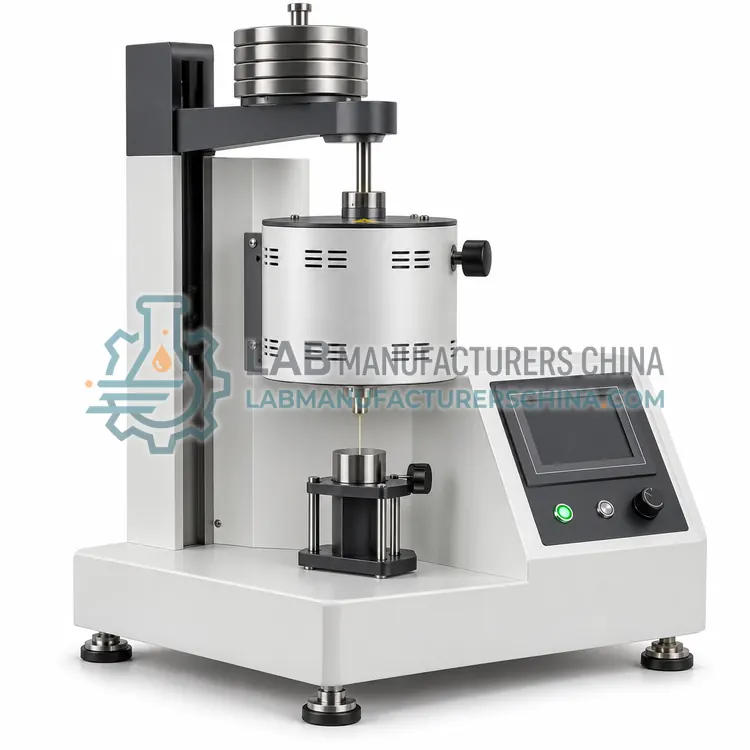
High-Temperature Melt Flow Rate Tester
高温熔体流动速率仪
- SKU MFT-0004
- Melt Flow Testers
- CE (to be confirmed)
- ISO 9001 manufacturing (to be confirmed)
Price on request — FOB / CIF quoted per order
Prices depend on configuration, quantity and destination port.
Key specifications
| Temperature range | 50–450 °C |
|---|---|
| Temperature accuracy | ±0.5 °C at 400 °C |
| Purge gas | Nitrogen or argon, ≥ 99.99% |
| Die dimensions | Ø 2.095 mm × 8.0 mm |
| Barrel material | Hardened steel or corrosion-resistant alloy |
| Load weights | 1.2 / 2.16 / 5 / 10 / 21.6 kg |
Request a quote Download brochure · to be provided
By Lab Manufacturers China Technical TeamLast reviewed Standards: ISO 1133-1, ISO 1133-2, ASTM D1238
What is the High-Temperature Melt Flow Rate Tester?
A high-temperature melt flow rate tester extends the barrel range to about 450 °C with inert gas purging, so engineering polymers such as polyamide, polysulfone and polyether ether ketone can be measured without oxidative degradation. It is specified when standard polyolefin conditions do not cover the material set.
Overview
Above roughly 300 °C, many polymers oxidise quickly in air, crosslink or release volatiles that change the flow behaviour during the test. A high-temperature tester therefore adds a wider heater band, high-temperature insulation, ceramic or metal-sheathed sensors, and a nitrogen or argon inlet that blankets the barrel headspace. The die and barrel may be supplied in hardened tool steel for aromatic polyamides or in corrosion-resistant alloys where fluoropolymers are processed. Higher temperatures increase wear on seals and shorten the life of the piston, so maintenance intervals are shorter than for standard units. Because flow varies strongly with temperature at these levels, calibration of the control loop and documentation of the purge flow rate are essential to comparable results.
How does it work?
A melt flow tester consists of a heated vertical barrel with a defined bore, a hardened steel die at the bottom, a piston and a set of certified weights. Polymer granules are loaded, compacted and held at the test temperature, then extruded through the die under a specified load. In method A, timed portions of extrudate are cut and weighed, and the result is expressed in grams per ten minutes. In method B, an encoder records piston displacement against time and the melt volume-flow rate is calculated in cubic centimetres per ten minutes, which can be converted to mass flow using the melt density. Temperature, load, die geometry and thermal equilibration time are all fixed by the method, because melt viscosity depends steeply on temperature and shear rate.
What are the key features?
- Barrel temperature range up to about 450 °C
- Nitrogen or argon purge to limit oxidation
- High-temperature insulation and sheathed sensors
- Wear-resistant barrel and die options
- Extended preheat and soak programming
- Temperature uniformity verified over the full range
What are the technical specifications?
A typical high-temperature melt flow rate tester configuration offers temperature range of 50–450 °C, temperature accuracy of ±0.5 °C at 400 °C, purge gas of Nitrogen or argon, ≥ 99.99%, die dimensions of Ø 2.095 mm × 8.0 mm, barrel material of Hardened steel or corrosion-resistant alloy and load weights of 1.2 / 2.16 / 5 / 10 / 21.6 kg. Values are indicative of the product class; the exact figures for each configuration are confirmed on the quotation and the calibration documents supplied with the instrument.
Which applications is it used for?
The High-Temperature Melt Flow Rate Tester is used in polyamide and polyacetal process control, polyether ether ketone and polysulfone quality checks, fluoropolymer and high-performance resin inspection and development of high-temperature engineering grades. Across the wider Melt Flow Testers class, laboratories also deploy it for polyolefin resin production and grade certification, incoming inspection of polyethylene and polypropylene and recycled plastics quality screening.
Which standards and certifications apply?
Relevant standards and methods include ISO 1133-1, ISO 1133-2, ASTM D1238, GB/T 3682.1, GB/T 3682.2 and IEC 61010-1. Certification candidates for this model are CE and ISO 9001 manufacturing; each is to be confirmed for the specific configuration before shipment, and certificates are supplied only where they have been issued.
Install the tester on a level, vibration-free bench away from draughts, and allow the barrel to reach thermal equilibrium before the first test, which usually takes 15 to 30 minutes. Clean the barrel and die after every test or every material change, using purging compound for degraded polymer; never scrape the barrel bore with hardened tools. Verify temperature with an external thermometer in the bore at defined intervals, check die dimensions against the method tolerance, and keep weights traceable. Dry hygroscopic polymers before testing, discard any extrudate containing bubbles or voids, and repeat the test when a single cut deviates strongly from the others.
How do I select the right High-Temperature Melt Flow Rate Tester?
Specify a high-temperature unit when the required test temperature exceeds 300 °C, when the standard condition for your polymer is set above that value, or when the polymer visibly degrades in air at the test temperature. Confirm the purge gas connection and flow control, ask for the temperature accuracy at the highest working point rather than at 200 °C, and agree a maintenance interval for seals and pistons that reflects the higher temperature duty.
How does it compare with other Melt Flow Testers variants?
Start from the standard your customer or specification cites, because ISO 1133 and ASTM D1238 fix different loads and procedures. Method A is sufficient for routine resin grading, while method B is preferable when the laboratory needs a fast result or the material is difficult to cut cleanly. Choose a high-temperature barrel when the scope includes engineering polymers such as polyamide, polysulfone or polyether ether ketone, and a corrosion-resistant barrel for PVC and fluoropolymers. Automatic units pay back where more than about ten tests per day are run, and multi-station units suit polyolefin plants that compare several production lines in one shift. Specify the load set, temperature range, data export format and cleaning accessories.
Full specifications
| Temperature range | 50–450 °C |
|---|---|
| Temperature accuracy | ±0.5 °C at 400 °C |
| Purge gas | Nitrogen or argon, ≥ 99.99% |
| Die dimensions | Ø 2.095 mm × 8.0 mm |
| Barrel material | Hardened steel or corrosion-resistant alloy |
| Load weights | 1.2 / 2.16 / 5 / 10 / 21.6 kg |
| Max test temperature setting | 450 °C |
| Data output | USB and RS232 |
| Power | 1.2–2 kW |
| Weight | 50–70 kg |
Indicative values for this product class. Final specifications are confirmed on the quotation and in the calibration documents supplied with the instrument.
Applications
- Polyamide and polyacetal process control
- Polyether ether ketone and polysulfone quality checks
- Fluoropolymer and high-performance resin inspection
- Development of high-temperature engineering grades
Key features
- Barrel temperature range up to about 450 °C
- Nitrogen or argon purge to limit oxidation
- High-temperature insulation and sheathed sensors
- Wear-resistant barrel and die options
- Extended preheat and soak programming
- Temperature uniformity verified over the full range
Frequently asked questions about High-Temperature Melt Flow Rate Tester
At high temperature, oxygen in the barrel headspace reacts with many polymers, causing crosslinking, chain scission or volatiles that change the extrusion rate during the test. A nitrogen or argon blanket displaces air and keeps the melt chemistry stable, so the result reflects the polymer rather than the degradation it experienced.
Well-designed high-temperature barrels hold about ±0.5 °C at 400 °C, compared with ±0.2 °C at conventional polyolefin temperatures. Because melt flow roughly doubles for every 20 to 30 °C rise, even that tolerance affects results, so the control loop should be calibrated at the working temperature rather than only at lower points.
The die geometry is the same as for standard testing, but the alloy may differ. Hardened tool steel resists wear from glass-filled engineering polymers, while corrosion-resistant alloys suit fluoropolymers that release hydrogen fluoride. The die should still be checked against the standard bore and length tolerance, since geometry, not material, defines the shear rate.
MFR is the melt mass-flow rate in grams per ten minutes, obtained by weighing timed cuts of extrudate. MVR is the melt volume-flow rate in cubic centimetres per ten minutes, obtained from piston displacement and time. The two are related through melt density, so a laboratory can report MFR from method B data if it knows the melt density at test temperature.
Melt viscosity changes steeply with temperature, so a sample that has not reached the barrel temperature extrudes faster or slower than the specified condition. Methods therefore require a defined preheat time, typically four to six minutes, after the sample is compacted. Checking the barrel with an external probe at intervals confirms that the controller reading is accurate.
Clean the die and barrel after each test or whenever the material changes, because residual polymer degrades at test temperature and alters the next result. Disassemble the die while warm, wipe it with a soft cloth and approved solvent, and never use abrasive tools. For heavily degraded or crosslinked residues, run purging compound before manual cleaning.