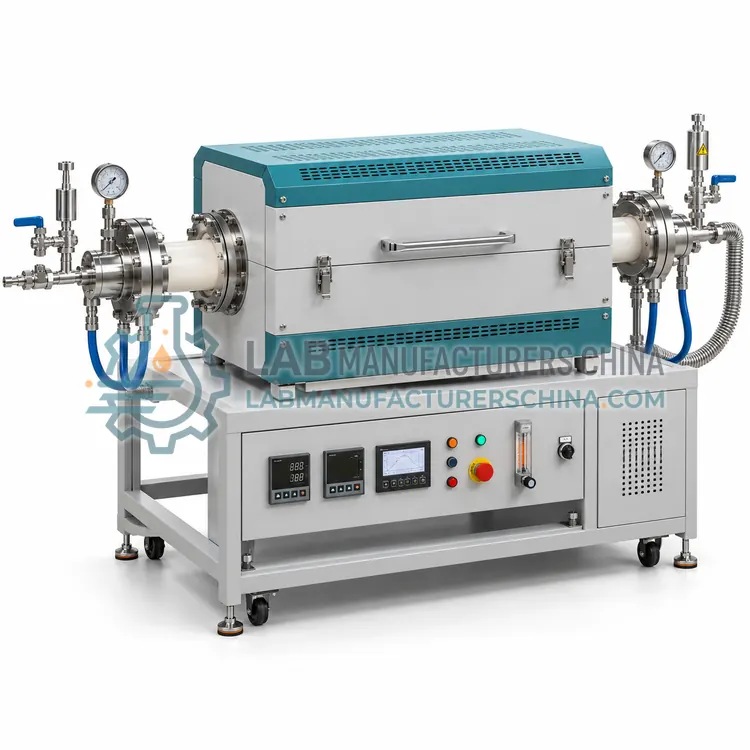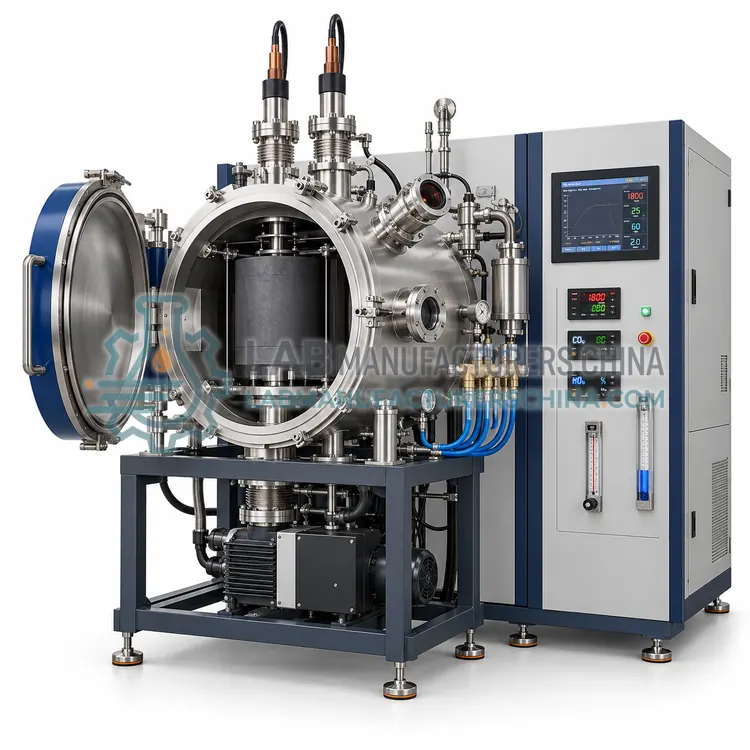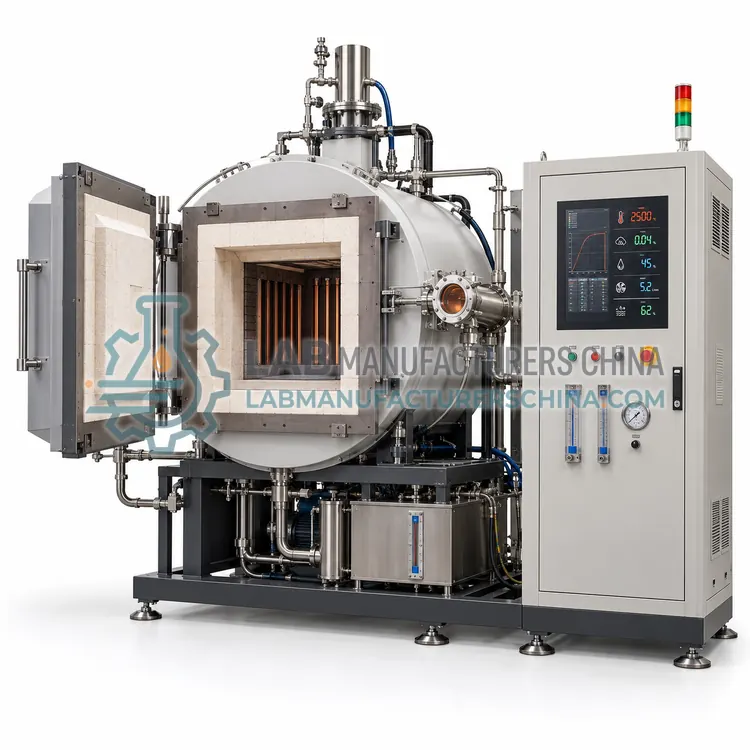
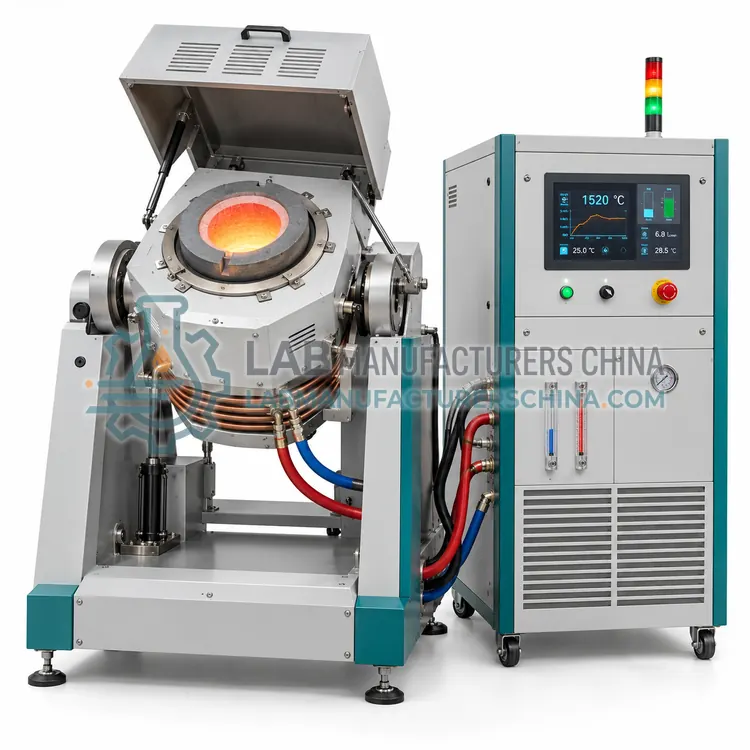
Induction Melting Furnace
感应熔炼炉
- SKU HTF-0004
- High Temperature Furnaces
- CE (to be confirmed)
- ISO 9001 manufacturing (to be confirmed)
- RoHS (to be confirmed)
Price on request — FOB / CIF quoted per order
Prices depend on configuration, quantity and destination port.
Key specifications
| Crucible capacity | 0.5–20 kg |
|---|---|
| Maximum temperature | 1600–2000 C |
| Induction frequency | 2–200 kHz |
| Melting power | 15–150 kW |
| Crucible material | Graphite, alumina or copper |
| Atmosphere | Vacuum or inert gas |
Request a quote Download brochure · to be provided
By Lab Manufacturers China Technical TeamLast reviewed Standards: IEC 61010-1, IEC 61010-2-010, IEC 60519-1
What is the Induction Melting Furnace?
An induction melting furnace melts conductive metals and alloys by coupling an alternating magnetic field into the charge or a susceptor. It is chosen for alloy preparation and melting research under vacuum or inert gas.
What is the Induction Melting Furnace?
An induction melting furnace melts conductive metals and alloys by coupling an alternating magnetic field into the charge or a susceptor. It is chosen for alloy preparation and melting research under vacuum or inert gas.
Overview
The induction melting furnace uses a water-cooled copper coil carrying alternating current to induce eddy currents in a conductive charge or susceptor, heating it from within. Frequencies from a few kilohertz to several hundred kilohertz suit different charge sizes and coupling, and the melt is often stirred by the electromagnetic field, which improves homogeneity. Crucibles are graphite, alumina, zirconia or water-cooled copper for reactive melts, and the chamber can be evacuated or filled with inert gas to prevent oxidation. Temperature reaches 1600 to 2000 C for most laboratory units, measured by thermocouple, optical pyrometer or by melt power estimation. It serves alloy development, reactive metal melting, glass melting and casting of small ingots.
How does it work?
High-temperature furnaces concentrate heat in a densely insulated hot zone using elements that remain stable at extreme temperature. Silicon carbide and molybdenum disilicide resist oxidation in air to about 1600 to 1800 C, while graphite and tungsten elements work beyond 2000 C under vacuum or inert gas because they oxidize in air. Induction furnaces instead use an alternating magnetic field to induce currents in a conductive crucible or susceptor, heating the charge directly. Dense alumina, zirconia or graphite insulation limits heat loss, and water-cooled shells protect the structure. Type B or C thermocouples, optical pyrometers and radiation sensors cover the range, and programmable controllers follow slow ramp profiles that avoid thermal shock. Atmosphere control is often essential to prevent oxidation, evaporation or contamination of the sample.
What are the key features?
- Water-cooled copper induction coil
- Adjustable frequency for different charge sizes
- Electromagnetic stirring of the melt
- Graphite, ceramic or water-cooled copper crucible
- Vacuum or inert-gas chamber
- Type C thermocouple or optical pyrometer
What are the technical specifications?
A typical induction melting furnace configuration offers crucible capacity of 0.5–20 kg, maximum temperature of 1600–2000 C, induction frequency of 2–200 kHz, melting power of 15–150 kW, crucible material of Graphite, alumina or copper and atmosphere of Vacuum or inert gas. Values are indicative of the product class; the exact figures for each configuration are confirmed on the quotation and the calibration documents supplied with the instrument.
Which applications is it used for?
The Induction Melting Furnace is used in alloy development and melting, reactive metal melting, glass and frit melting, small ingot casting and rapid alloy screening. Across the wider High Temperature Furnaces class, laboratories also deploy it for advanced ceramic sintering, refractory material testing and glass and frit melting.
Which standards and certifications apply?
Relevant standards and methods include IEC 61010-1, IEC 61010-2-010, IEC 60519-1, DIN 17052-1, ISO 9001 and ISO 17025. Certification candidates for this model are CE, ISO 9001 manufacturing and RoHS; each is to be confirmed for the specific configuration before shipment, and certificates are supplied only where they have been issued.
High-temperature furnaces need rigid foundations, generous clearances and, for water-cooled types, reliable cooling with flow and temperature interlocks. Install gas and vacuum lines with proper purging and leak checking, and never heat a graphite or refractory-metal element in air. Warm up and cool slowly according to the schedule to protect dense refractories and elements from thermal shock. Replace elements and thermocouples as matched sets and on condition. Verify temperature with a reference instrument and profile the hot zone periodically, keep records, and train operators on atmosphere, water and emergency shutdown procedures.
How do I select the right Induction Melting Furnace?
Select the induction melting furnace when a conductive charge must be melted, stirred and cast, especially under vacuum or inert gas. Resistance furnaces suit sintering and heat treatment rather than melting. In the RFQ, specify charge mass and material, top temperature, frequency, crucible type, atmosphere and cooling water.
How does it compare with other High Temperature Furnaces variants?
Choose a high-temperature furnace only when the process genuinely needs 1400 C or above, since cost, element life and atmosphere requirements rise steeply with temperature. Decide the atmosphere first: air, inert gas, vacuum or reducing, because elements and insulation depend on it. Then set the maximum temperature and hot zone size from the sample and crucible, and select the heating method, with resistance for clean work and induction for melting conductive charges. Confirm the temperature measurement method for the range, since thermocouples need type B or C and optical pyrometers are used above about 1800 C. Specify ramping capability, cooling, water supply and safety protection.
Full specifications
| Crucible capacity | 0.5–20 kg |
|---|---|
| Maximum temperature | 1600–2000 C |
| Induction frequency | 2–200 kHz |
| Melting power | 15–150 kW |
| Crucible material | Graphite, alumina or copper |
| Atmosphere | Vacuum or inert gas |
| Temperature measurement | Type C thermocouple or pyrometer |
| Cooling water | Required for coil and shell |
| Stirring | Electromagnetic, inherent |
| Power supply | 380 V, 3-phase, 50/60 Hz |
Indicative values for this product class. Final specifications are confirmed on the quotation and in the calibration documents supplied with the instrument.
Applications
- Alloy development and melting
- Reactive metal melting
- Glass and frit melting
- Small ingot casting
- Rapid alloy screening
Key features
- Water-cooled copper induction coil
- Adjustable frequency for different charge sizes
- Electromagnetic stirring of the melt
- Graphite, ceramic or water-cooled copper crucible
- Vacuum or inert-gas chamber
- Type C thermocouple or optical pyrometer
Frequently asked questions about Induction Melting Furnace
Induction couples energy directly into the conductive charge or susceptor through a magnetic field, melting quickly and stirring the melt electromagnetically. Resistance heating warms the crucible from outside, which is simpler and more uniform for holding but slower for melting.
The copper coil and often the crucible shell carry high current or face high heat, so water cooling keeps them below their limits. Flow and temperature interlocks are essential, since a loss of cooling during a melt can damage the coil and create a safety hazard.
Only electrically conductive charges couple directly, so metals and alloys melt readily. Non-conductive materials such as glass or oxides need a conductive susceptor, often graphite, which heats and transfers heat to the charge.
Standard high-temperature furnaces reach 1400 to 1800 C with silicon carbide or molybdenum disilicide elements. Graphite or tungsten hot zones under vacuum or inert gas extend the range to 2200 to 3000 C, but they cannot operate in air.
Graphite oxidizes rapidly in air above about 500 C, losing mass and contaminating the sample. Under vacuum or inert gas such as argon, graphite elements and insulation remain stable to well above 2000 C, which is why they dominate ultra-high-temperature work.
Induction heating suits melting conductive charges and heating a susceptor rapidly, because energy couples directly into the material or crucible. Resistance heating gives more uniform, controllable heating of a chamber and is preferred for sintering and heat treatment.
Related models