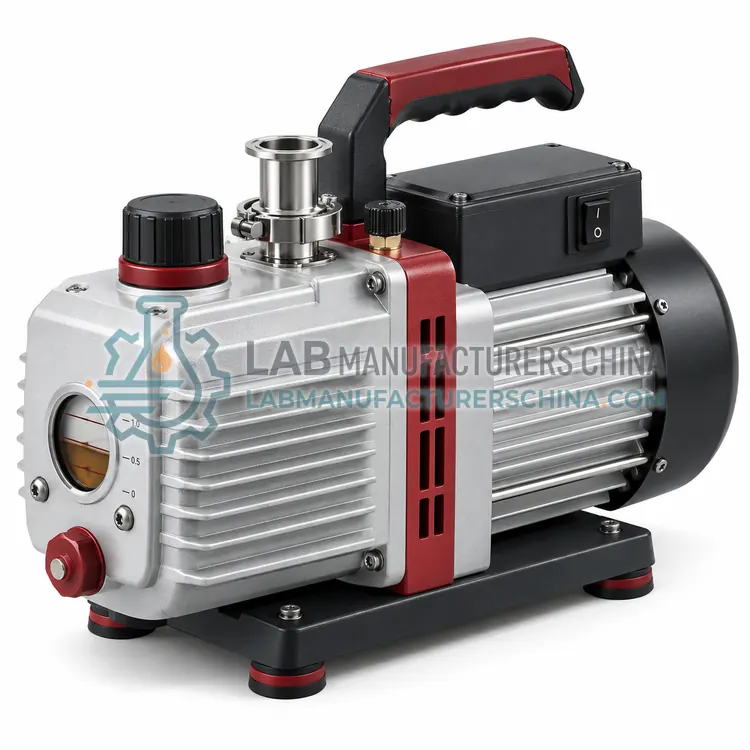
Chemistry Duty Rotary Vane Vacuum Pump
耐化学旋片真空泵
- SKU VAP-0003
- Vacuum Pumps
- CE (to be confirmed)
- RoHS (to be confirmed)
- ISO 9001 manufacturing (to be confirmed)
Price on request — FOB / CIF quoted per order
Prices depend on configuration, quantity and destination port.
Key specifications
| Ultimate vacuum | 2–0.5 mbar |
|---|---|
| Pumping speed | 30–200 L/min |
| Motor power | 200–750 W |
| Oil capacity | 0.3–1.5 L |
| Gas ballast | Yes |
| Corrosion protection | Coated internals or stainless |
Request a quote Download brochure · to be provided
By Lab Manufacturers China Technical TeamLast reviewed Standards: IEC 61010-1, IEC 61326-1, ISO 21360
What is the Chemistry Duty Rotary Vane Vacuum Pump?
A chemistry duty rotary vane vacuum pump delivers a deep vacuum of about 2 to 0.5 mbar for rotary evaporation, drying and vacuum ovens. It is built with corrosion-resistant internals and is normally used with a cold trap and oil mist filter.
What is the Chemistry Duty Rotary Vane Vacuum Pump?
A chemistry duty rotary vane vacuum pump delivers a deep vacuum of about 2 to 0.5 mbar for rotary evaporation, drying and vacuum ovens. It is built with corrosion-resistant internals and is normally used with a cold trap and oil mist filter.
Overview
The chemistry duty rotary vane pump uses an eccentric rotor with spring-loaded vanes that trap and compress gas against the stator. Ultimate vacuum is around 2 to 0.5 mbar, and pumping speed ranges from 30 to 200 L/min. Internals are coated or made from corrosion-resistant materials, and the oil is formulated for chemical service, sometimes with a fluorinated oil for aggressive vapors. A gas ballast valve admits air to purge condensable vapor from the oil, which is important when pumping solvents. Accessories include a separator, oil mist filter, cold trap and vacuum gauge. Because deep vacuum and higher flow increase solvent carry-over, correct trapping and oil maintenance are essential. These pumps are widely used for rotary evaporation, gel drying, vacuum ovens, filtration under deep vacuum and Schlenk line work.
How does it work?
A laboratory vacuum pump removes gas from a sealed vessel to lower the pressure. Diaphragm pumps flex a membrane with check valves, drawing gas in and expelling it without oil, which suits filtration, aspiration and general laboratory work. Rotary vane pumps use an eccentric rotor with sliding vanes to trap and compress gas, giving a deeper vacuum for rotary evaporation and drying, but they need oil and protection against solvent vapor. Water aspirators use a Venturi effect in flowing tap water and are inexpensive but consume water and reach only a modest vacuum. In each case the pump is matched to a receiver, trap and gauge, and solvent or acid vapor must be trapped before it reaches the pump. Flow rate, ultimate pressure and chemical compatibility define performance.
What are the key features?
- Ultimate vacuum of about 2–0.5 mbar
- Pumping speed of 30–200 L/min
- Corrosion-resistant rotor, vanes and coatings
- Gas ballast valve for condensable vapors
- Chemical-grade or fluorinated pump oil
- Oil mist filter and cold trap accessories
What are the technical specifications?
A typical chemistry duty rotary vane vacuum pump configuration offers ultimate vacuum of 2–0.5 mbar, pumping speed of 30–200 L/min, motor power of 200–750 W, oil capacity of 0.3–1.5 L, gas ballast of Yes and corrosion protection of Coated internals or stainless. Values are indicative of the product class; the exact figures for each configuration are confirmed on the quotation and the calibration documents supplied with the instrument.
Which applications is it used for?
The Chemistry Duty Rotary Vane Vacuum Pump is used in rotary evaporation, vacuum oven operation, gel and sample drying, deep vacuum filtration and schlenk line vacuum. Across the wider Vacuum Pumps class, laboratories also deploy it for vacuum filtration and solid-phase extraction, rotary evaporation and solvent recovery and vacuum oven drying and degassing.
Which standards and certifications apply?
Relevant standards and methods include IEC 61010-1, IEC 61326-1, ISO 21360, EN 12469 and GB 4793.1. Certification candidates for this model are CE, RoHS and ISO 9001 manufacturing; each is to be confirmed for the specific configuration before shipment, and certificates are supplied only where they have been issued.
Always fit a liquid trap between the vessel and the pump so that condensate or foam cannot enter the pump head. For solvent work, add a cold trap or an acid-resistant inline filter and change the pump oil regularly, watching for discoloration or emulsion. Vent the exhaust away from the operator when pumping hazardous vapors. Check diaphragms and valves on the maintenance schedule, since they are the usual wear points, and keep spare parts. Mount the pump on a stable surface with adequate ventilation, and confirm the electrical supply and, where required, use a pump rated for the ambient conditions. Follow IEC 61010-1 for electrical safety. Verify the achieved vacuum with a gauge rather than assuming the rated value, and record it for method consistency.
How do I select the right Chemistry Duty Rotary Vane Vacuum Pump?
Choose a chemistry duty rotary vane pump for rotary evaporation, drying and ovens that need a deep vacuum. For filtration only, an oil-free diaphragm pump is simpler. In the RFQ, state ultimate vacuum, pumping speed, solvent types, KF connection sizes and whether a gas ballast and trap are required.
How does it compare with other Vacuum Pumps variants?
Choose by the required vacuum level and the vapor being pumped. For filtration, aspiration and vacuum concentration where a moderate vacuum is enough, an oil-free diaphragm pump is usually the right choice, because it needs little maintenance and cannot backstream oil. For rotary evaporation, gel drying and vacuum ovens that need a deeper vacuum, a chemically resistant rotary vane pump with a cold trap and oil mist filter works well. Use a water aspirator only where tap water is available and water use is acceptable. Then match the free-air flow rate to the system volume and the speed of operation you need, and confirm the pump can start against the load. Check wetted materials and diaphragm or vane materials for solvent and acid compatibility, noise level, and whether a gauge, regulator or vacuum controller is included.
Full specifications
| Ultimate vacuum | 2–0.5 mbar |
|---|---|
| Pumping speed | 30–200 L/min |
| Motor power | 200–750 W |
| Oil capacity | 0.3–1.5 L |
| Gas ballast | Yes |
| Corrosion protection | Coated internals or stainless |
| Oil mist filter | Included or optional |
| Noise level | 50–65 dB(A) |
| Intake connection | KF 16–KF 25 |
| Power supply | 220–240 V, 50/60 Hz |
Indicative values for this product class. Final specifications are confirmed on the quotation and in the calibration documents supplied with the instrument.
Applications
- Rotary evaporation
- Vacuum oven operation
- Gel and sample drying
- Deep vacuum filtration
- Schlenk line vacuum
Key features
- Ultimate vacuum of about 2–0.5 mbar
- Pumping speed of 30–200 L/min
- Corrosion-resistant rotor, vanes and coatings
- Gas ballast valve for condensable vapors
- Chemical-grade or fluorinated pump oil
- Oil mist filter and cold trap accessories
Frequently asked questions about Chemistry Duty Rotary Vane Vacuum Pump
A gas ballast admits fresh air into the compression cycle so that condensable vapor is expelled with the exhaust rather than dissolving in the oil. It keeps the oil clean and preserves vacuum performance.
When it becomes dark, cloudy or emulsified, often every few hundred operating hours in solvent service. Use the correct grade or fluorinated oil and dispose of used oil as chemical waste.
Yes, rotary vane pumps are built for continuous duty, but extended running with solvent vapor increases oil contamination. Trap condensables and monitor vacuum to decide when service is needed.
Choose oil-free for filtration, aspiration and general work where a moderate vacuum is enough and maintenance should be simple. Choose an oil-sealed rotary vane pump for deeper vacuum in rotary evaporation, drying and ovens, adding a cold trap to protect the oil.
Fit a cold trap and, where needed, an activated carbon or acid trap between the vessel and the pump. Keep the trap cold and empty it regularly. For oil-sealed pumps, change the oil when it darkens or emulsifies.
Match the free-air flow rate to the funnel and flask volume and to the filtration speed. A pump of about 10 to 30 L/min suits most single-place filtration, while multi-place manifolds need higher flow or several pumps.