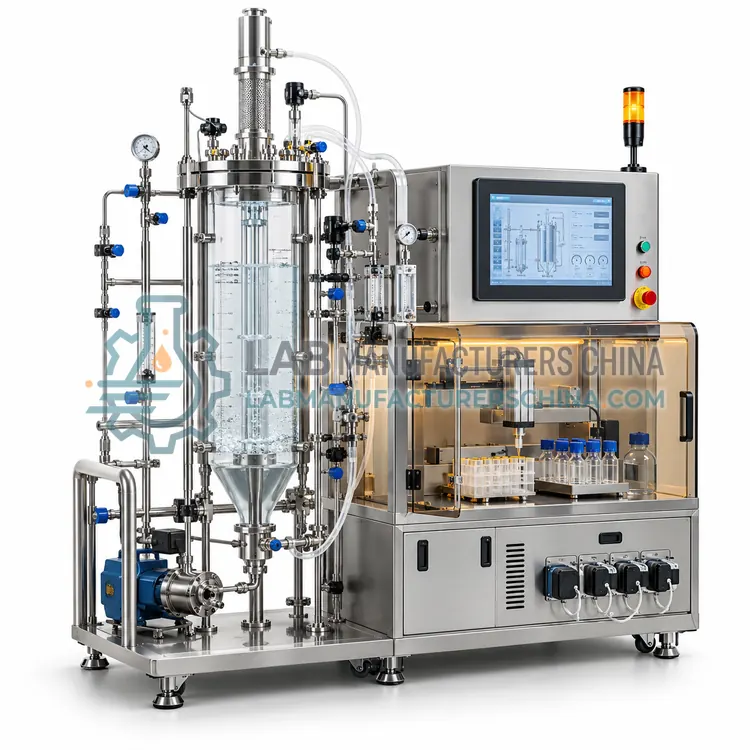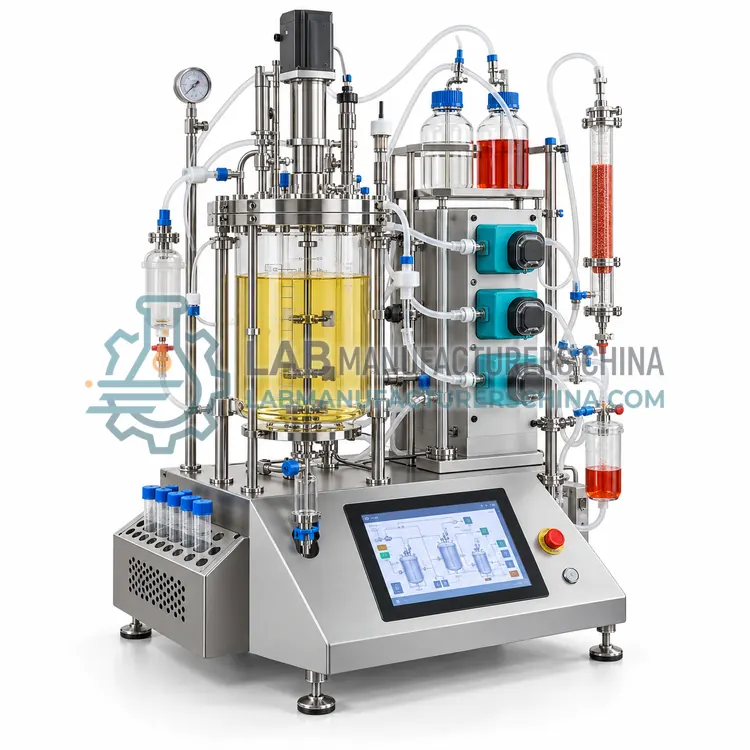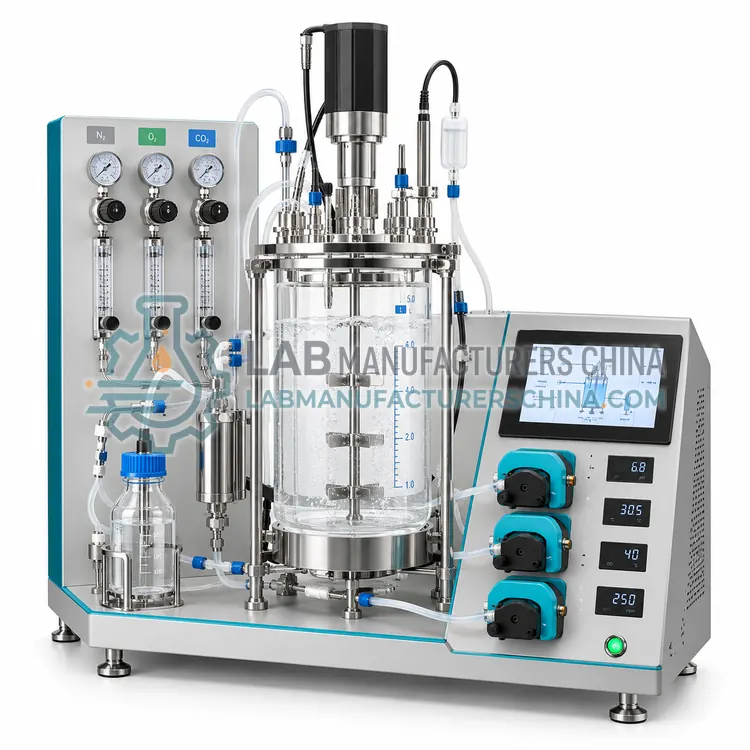
Pilot Single-Use Fermenter
一次性使用中试发酵罐
- SKU PIF-0003
- Pilot Fermenters
- CE (to be confirmed)
- ISO 13485 manufacturing (to be confirmed)
- ISO 11137 sterilization (to be confirmed)
Price on request — FOB / CIF quoted per order
Prices depend on configuration, quantity and destination port.
Key specifications
| Working volume | 50–500 L |
|---|---|
| Bag material | Multi-layer polyethylene film |
| Sterilization | Gamma irradiation 25–40 kGy |
| Mixing | Impeller, rocking or wave |
| Temperature range | 10–50 °C |
| Dissolved oxygen control | Single-use sensor, cascade control |
Request a quote Download brochure · to be provided
By Lab Manufacturers China Technical TeamLast reviewed Standards: EU GMP Annex 1, EU GMP Annex 11, 21 CFR Part 11
What is the Pilot Single-Use Fermenter?
A pilot single-use fermenter uses a pre-sterilized bag in a reusable support, avoiding cleaning validation between products at pilot scale. It suits demanding clinical batches, multi-product production and reliable intermediate-scale process development.
What is the Pilot Single-Use Fermenter?
A pilot single-use fermenter uses a pre-sterilized bag in a reusable support, avoiding cleaning validation between products at pilot scale. It suits demanding clinical batches, multi-product production and reliable intermediate-scale process development.
Overview
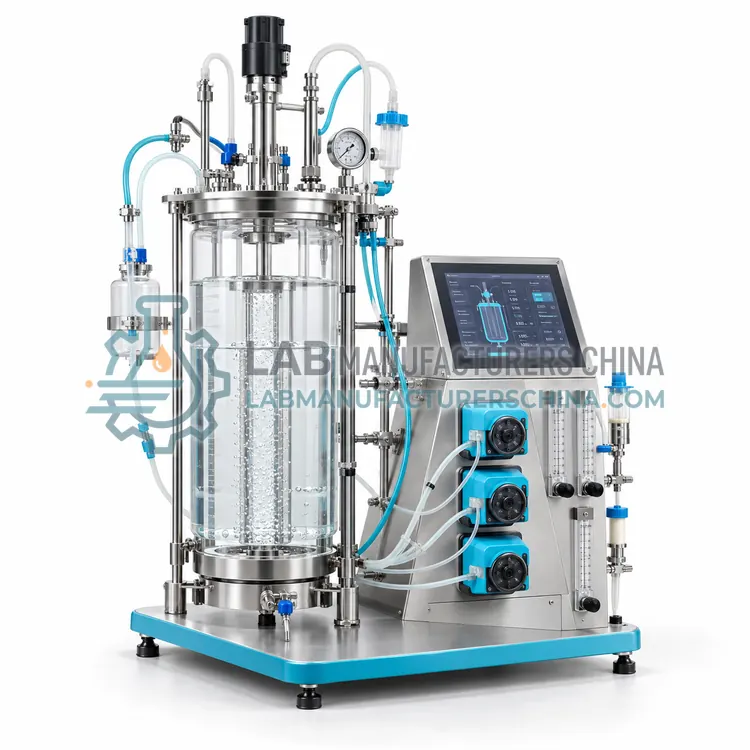
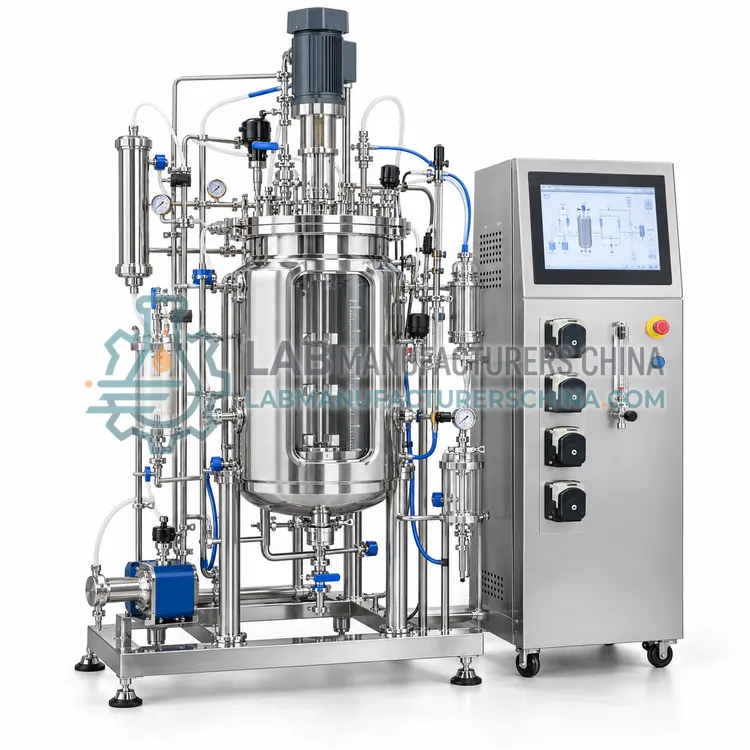
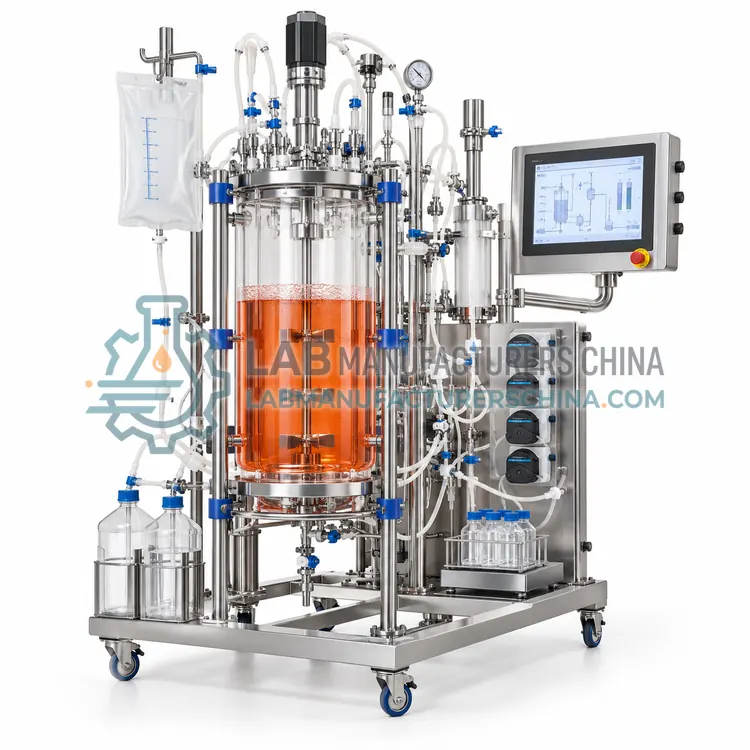
A pilot single-use fermenter brings the disposable concept to the 50 to 500 litre range. A pre-sterilized, gamma-irradiated bag fits a stainless support that provides temperature control and, in some designs, a magnetically driven or top-mounted impeller. The bag includes gas sparging and exhaust, feed, sampling and dosing ports and, increasingly, single-use sensors for pH and dissolved oxygen. Rocking or wave-mixed bags provide gentler mixing for shear-sensitive cultures, while stirred bags give higher oxygen transfer. Because the fluid path is single-use, changeover between products is fast and cleaning validation is not needed for that path, which suits clinical batches and multi-product facilities. Extractables and leachables data, bag integrity testing, volume and pressure limits and supply continuity are the main considerations.
How does it work?
A pilot fermenter applies the same biological principles as a laboratory vessel but at a scale where mixing, oxygen transfer and heat removal behave differently. Agitation by a larger impeller and higher gas flow increase oxygen transfer, described by the volumetric mass-transfer coefficient, while a jacket or coil removes the greater metabolic heat load. Sensors for temperature, pH, dissolved oxygen, pressure and often foam or redox are placed so that readings represent the bulk liquid, and cascade control adjusts agitation, gas flow and back pressure to hold dissolved oxygen. Because mixing time and tip speed cannot all be kept equal to the laboratory scale, engineers choose the most critical criterion for the process and verify performance. Pilot vessels are usually stainless steel with clean-in-place and sterilize-in-place capability, and they include defined sampling and harvest points.
What are the key features?
- Pre-sterilized bag in a reusable stainless support
- Stirred, rocking or wave mixing options
- Integrated single-use pH and dissolved oxygen sensors
- No cleaning validation of the product-contact path
- Fast changeover between products
What are the technical specifications?
A typical pilot single-use fermenter configuration offers working volume of 50–500 L, bag material of Multi-layer polyethylene film, sterilization of Gamma irradiation 25–40 kGy, mixing of Impeller, rocking or wave, temperature range of 10–50 °C and dissolved oxygen control of Single-use sensor, cascade control. Values are indicative of the product class; the exact figures for each configuration are confirmed on the quotation and the calibration documents supplied with the instrument.
Which applications is it used for?
The Pilot Single-Use Fermenter is used in clinical batch production, multi-product pilot manufacturing, scale-up process development and shear-sensitive culture scale-up. Across the wider Pilot Fermenters class, laboratories also deploy it for scale-up verification, pilot and clinical batch production and enzyme and metabolite production.
Which standards and certifications apply?
Relevant standards and methods include EU GMP Annex 1, EU GMP Annex 11, 21 CFR Part 11, 21 CFR Part 211, GB/T 150, USP <87>, USP <88>, ICH Q11 and IEC 61010-1. Certification candidates for this model are CE, ISO 13485 manufacturing and ISO 11137 sterilization; each is to be confirmed for the specific configuration before shipment, and certificates are supplied only where they have been issued.
Qualify the vessel after installation with pressure and temperature tests and confirm cleaning and sterilization performance with documented procedures. Calibrate all probes and verify sensor placement so that readings reflect bulk conditions. Establish scale-up criteria before the first run, such as constant volumetric mass-transfer coefficient, tip speed or mixing time, and document which was chosen and why. Monitor foam, heat removal and dissolved oxygen closely, since these are the usual failure modes when moving up in scale. Keep batch records that capture setpoints, deviations and offline measurements. Manage utility supply, gaskets and seals as routine maintenance items, and review alarms after each campaign.
How do I select the right Pilot Single-Use Fermenter?
Choose a pilot single-use fermenter when changeover speed and cleaning avoidance matter at intermediate scale. In an RFQ specify volume, mixing principle, bag and sensor options, pressure and temperature limits, extractables data and the integrity test method.
How does it compare with other Pilot Fermenters variants?
Size the vessel to reproduce the most important laboratory parameter and to produce enough material for the next step, whether that is a clinical batch, a trial product quantity or data for production design. Decide between stainless steel, which suits repeated campaigns and higher pressures, and single-use, which shortens changeover. Confirm that the geometry, impeller type and gas handling can match the linear velocity or mass-transfer rate you intend to hold constant. List the control loops and their ranges, the number of feed, sampling and harvest ports, and whether redox, exhaust gas analysis or back-pressure control are needed. Evaluate clean-in-place and sterilize-in-place design, material certificates, records and the ability to transfer recipes to production vessels. Check service access and utility requirements before installation.
Full specifications
| Working volume | 50–500 L |
|---|---|
| Bag material | Multi-layer polyethylene film |
| Sterilization | Gamma irradiation 25–40 kGy |
| Mixing | Impeller, rocking or wave |
| Temperature range | 10–50 °C |
| Dissolved oxygen control | Single-use sensor, cascade control |
| Pressure rating | Up to 0.2–0.5 bar |
| Extractables testing | BPOG and USP <661> aligned studies |
Indicative values for this product class. Final specifications are confirmed on the quotation and in the calibration documents supplied with the instrument.
Applications
- Clinical batch production
- Multi-product pilot manufacturing
- Scale-up process development
- Shear-sensitive culture scale-up
Key features
- Pre-sterilized bag in a reusable stainless support
- Stirred, rocking or wave mixing options
- Integrated single-use pH and dissolved oxygen sensors
- No cleaning validation of the product-contact path
- Fast changeover between products
Frequently asked questions about Pilot Single-Use Fermenter
Pilot single-use fermenters typically reach about 500 litres, and dedicated production-scale single-use bioreactors extend to a few thousand litres. Above this, mechanical support, mixing and gas exchange in a bag become harder to control reliably.
Single-use pH and dissolved oxygen patches are supplied pre-calibrated or calibrated at the point of use and are read by a reusable transmitter. Their performance is verified against offline measurements, because drift can occur during long runs.
Stirred single-use bags can handle moderately viscous broths, but very viscous or filamentous cultures may not mix well because impeller power and baffling are limited. Such processes often remain on stainless steel with a conventional agitator.
It verifies that a process developed at bench scale still behaves as expected at larger volume, and it produces enough material for clinical trials, product evaluation or production design. It also exposes scale-dependent effects such as oxygen limitation or poor heat removal.
Constant volumetric mass-transfer coefficient, constant tip speed, constant power per volume and constant mixing time cannot all be held at once. The team selects the criterion most related to product quality or yield, applies it, and verifies performance at the pilot scale before transferring to production.
Stainless steel suits repeated campaigns, high pressures and steam sterilization, and can be validated for many years of use. Single-use suits multi-product or clinical work where cleaning validation between products would be costly, but volume, pressure and extractables data must be considered.
Related models